
Turning stainless steel: how to choose between the BF, BM and BR chipbreakers
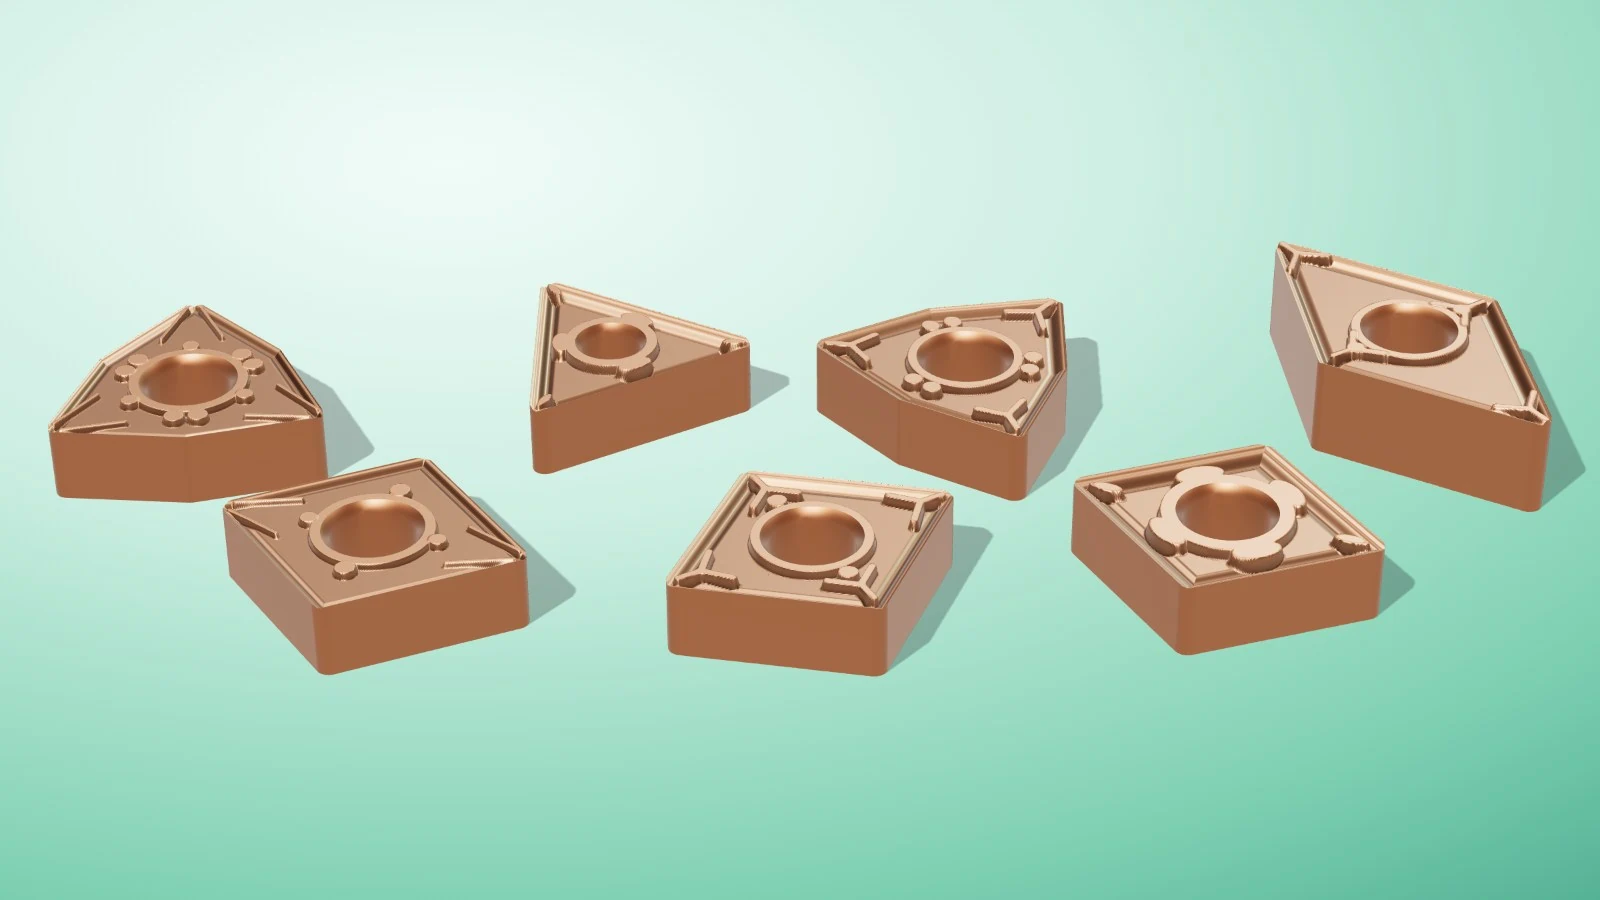
Stainless steel tends to work-harden, form built-up edges and generate long, tough chips. That is why using an insert designed for carbon steel often leads to rapid wear and a poor finish. The INNOT stainless steel series was created to solve these problems with three chipbreakers and two dedicated PVD grades.
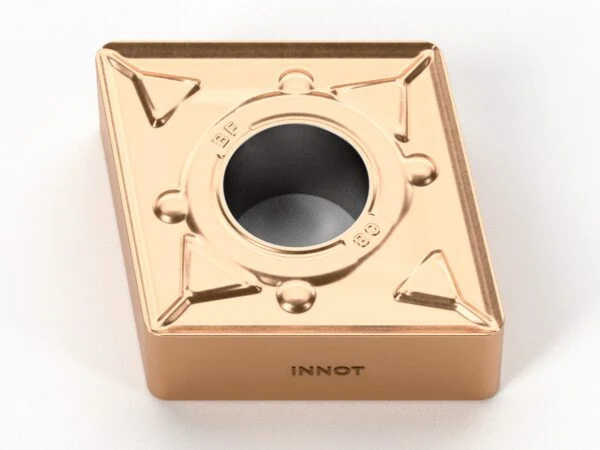
BF: finishing with light cuts
Sharp cutting edge and low cutting forces, with good chip control even at small depths. On austenitic stainless steel (AISI 304, 316) the starting values are: Vc 95–185 m/min, fn 0.08–0.30 mm/rev, ap 0.20–2.00 mm.
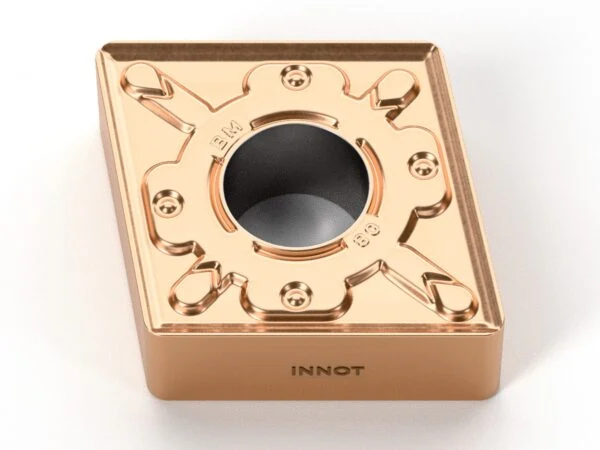
BM: semi-finishing, the most versatile
Micro-preparation of the cutting edge provides both sharpness and strength, for high productivity and long tool life. Values on austenitic grades: Vc 90–170 m/min, fn 0.10–0.52 mm/rev, ap 1.00–5.80 mm.
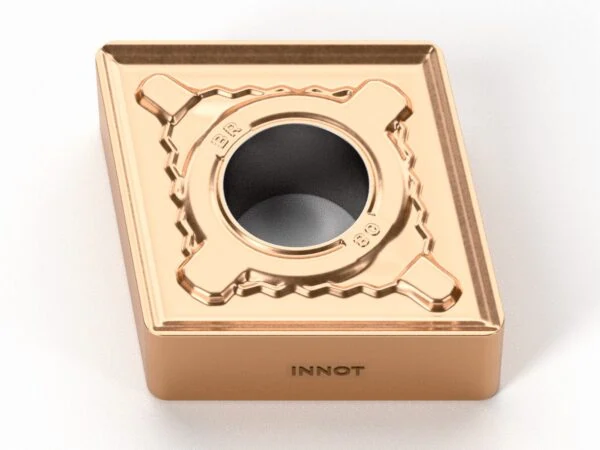
BR: roughing and interrupted cuts
High-strength profile for roughing and interrupted cuts. Values on austenitic grades: Vc 80–150 m/min, fn 0.18–0.66 mm/rev, ap 1.70–7.00 mm.
Application range and starting values
| Chipbreaker | Operation | Vc (m/min) | fn (mm/rev) | ap (mm) |
|---|---|---|---|---|
| BF | Finishing | 95–185 | 0.08–0.30 | 0.20–2.00 |
| BM | Semi-finishing | 90–170 | 0.10–0.52 | 1.00–5.80 |
| BR | Roughing | 80–150 | 0.18–0.66 | 1.70–7.00 |
Indicative values on austenitic stainless steel (AISI 304, 316) with grade IT7225. On martensitic stainless steel, reduce the cutting speed by about 10 m/min.
Which grade: IT7225 or IT7125?
- IT7225: first choice for stainless steel, AlTiSiN + TiSiN nano-gradient coating with excellent wear resistance and toughness. Suitable for stable and average conditions, it is the only one recommended on martensitic stainless steel (AISI 420, 431).
- IT7125: universal grade with low-friction AlTiN coating, tougher in interrupted cuts and difficult conditions.
Three tips from the shop floor
- Do not go too low with the feed: "rubbing" increases work hardening.
- Use plenty of constant coolant.
- On martensitic stainless steel lower the cutting speed by about 10 m/min compared with austenitic grades and use grade IT7225, as shown in the tables.
You will find the full cutting data in the product sheets CNMG-BF, CNMG-BM and CNMG-BR. Have a special case? Write to us: we help you choose.






