
Superalloys and Inconel: cutting data with SF and SM chipbreakers
Heat-resistant superalloys such as Inconel 718 keep their strength even at high temperatures. That is exactly what makes them hard to machine: heat concentrates on the cutting edge, the material work-hardens and notch wear appears easily. You need sharp cutting edges, specific grades and moderate cutting speeds.
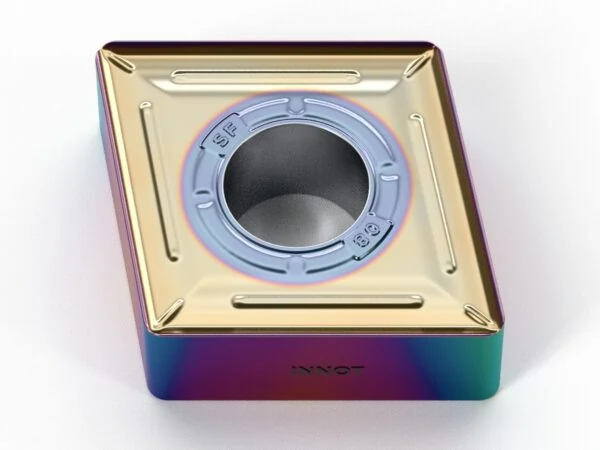
SF: finishing
The specially designed corner radius and the sharp cutting edge reduce cutting forces and vibration, for a smooth surface and good chip evacuation.
- IT9205: Vc 40–80 m/min
- IT9215: Vc 30–70 m/min
- fn 0.02–0.20 mm/rev, ap 0.20–1.80 mm
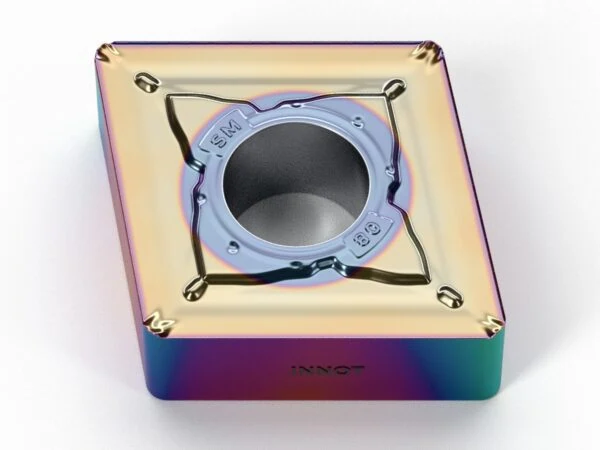
SM: from semi-finishing to roughing
It combines edge strength and chip control. The light cut slows work hardening and limits notch wear.
- IT9205: Vc 40–80 m/min
- IT9215: Vc 30–70 m/min
- fn 0.15–0.40 mm/rev in stable conditions (up to 0.30 in difficult conditions), ap 0.70–3.00 mm
Application range and starting values
| Chipbreaker | Operation | Vc IT9205 (m/min) | Vc IT9215 (m/min) | fn (mm/rev) | ap (mm) |
|---|---|---|---|---|---|
| SF | Finishing | 40–80 | 30–70 | 0.02–0.20 | 0.20–1.80 |
| SM | Semi-finishing and roughing | 40–80 | 30–70 | 0.15–0.40 | 0.70–3.00 |
Indicative values on Inconel 718 and nickel-based superalloys. Under difficult conditions with SM, stay within 0.30 mm/rev.
IT9205 or IT9215?
Both have a multilayer AlTiN + TiSiN + AlCrN PVD coating. IT9205 favours wear resistance and allows higher speeds; IT9215 is tougher and safer when conditions get difficult.
A real case
On a steam valve made of a nickel-iron superalloy (Incoloy 901 type), in external turning with emulsion, we used a CNMG120408-SM in grade IT9215 at Vc 41.7 m/min, fn 0.2 mm/rev and ap 2.5 mm. Result: even wear and insert life 30% longer than the insert used previously.
Full cutting data in the product sheets CNMG-SF and CNMG-SM. Machining titanium or superalloys? Contact us for cutting data on your material.






