
Grey or nodular iron, continuous cut or with casting skin: how to choose between CNMG for cast iron, flat CNMA and CNMG-ZR, with cutting speeds, feeds and practical tips.
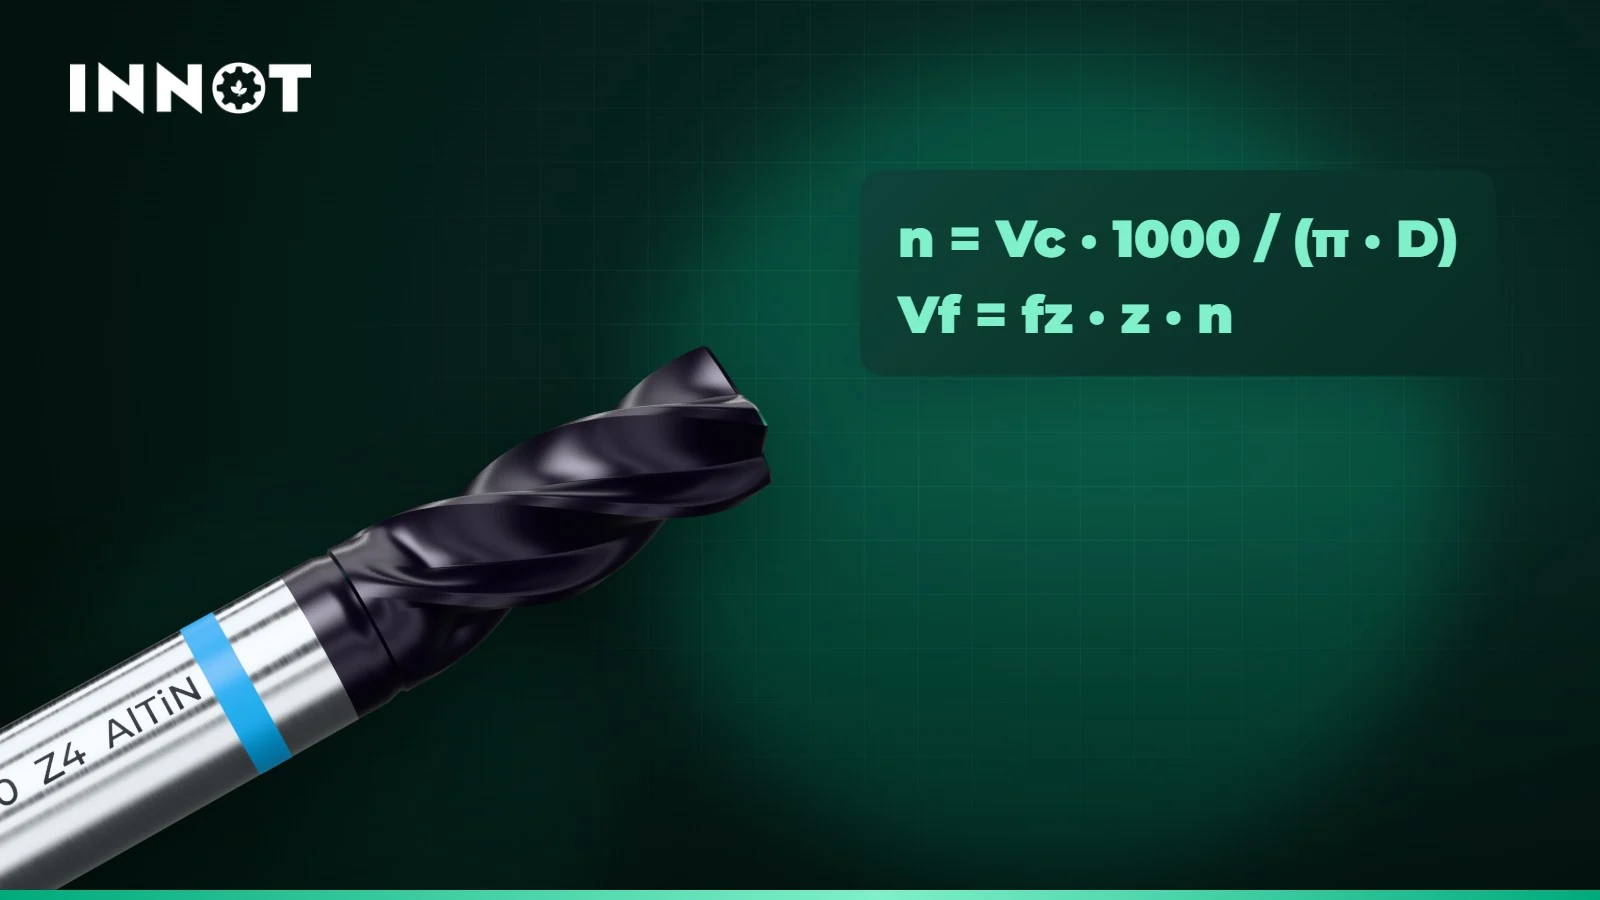
From Vc to rpm, machine feed, cutting time and metal removal rate: the turning and milling formulas with worked examples and chip thinning.
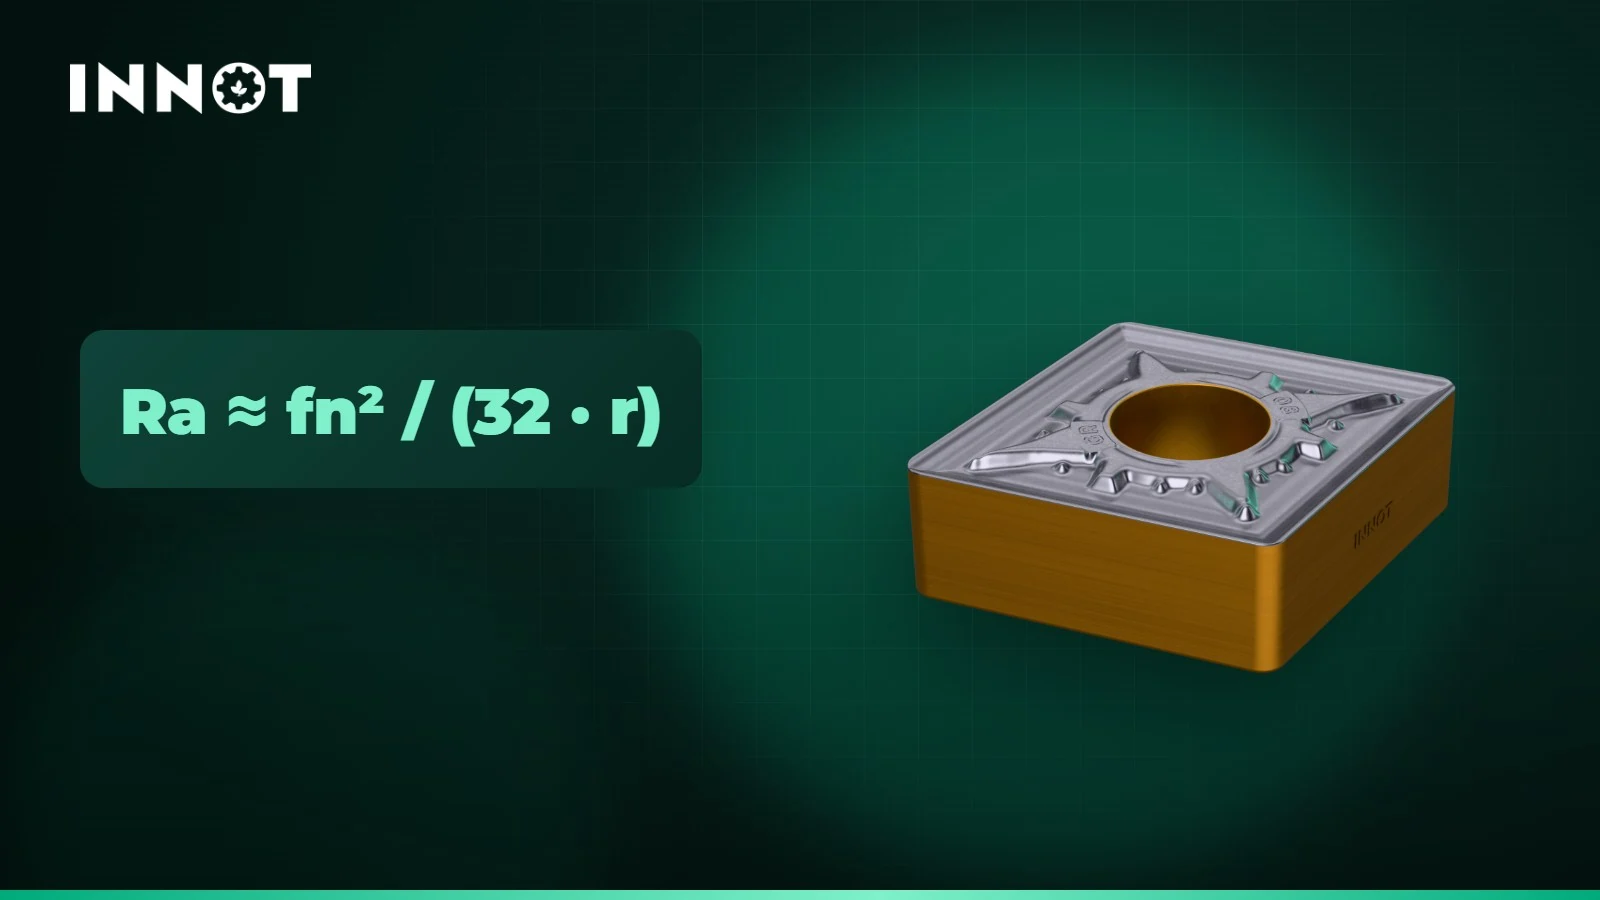
The formula Ra ≈ fn² / (32·r) explained with a ready-made table: maximum feed for Ra 0.8 – 1.6 – 3.2 – 6.3 µm with nose radii from 0.4 to 1.6 mm.
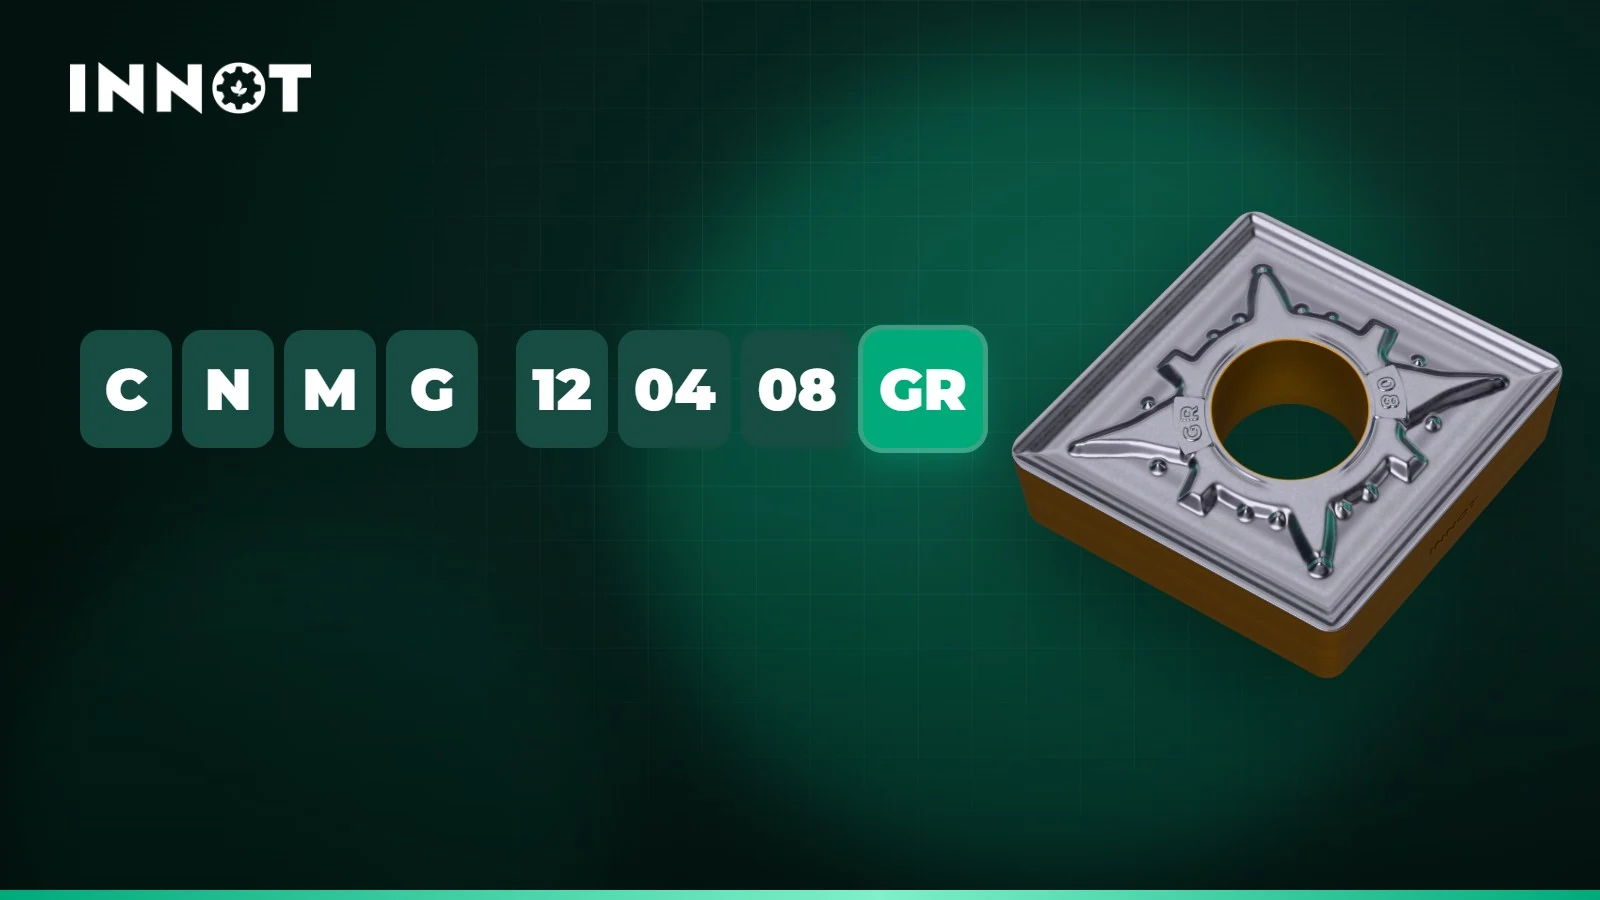
Shape, clearance angle, tolerance, type, size and nose radius: the ISO designation of an insert letter by letter, with tables and practical examples.
Machining Inconel 718 and nickel-based superalloys requires specific inserts and cutting data. Here is how to use the INNOT SF and SM chipbreakers with grades IT9205 and IT9215.
Finishing, semi-finishing or roughing: a quick guide to choosing the right INNOT chipbreaker and grade for machining AISI 304, 316 and martensitic stainless steels.
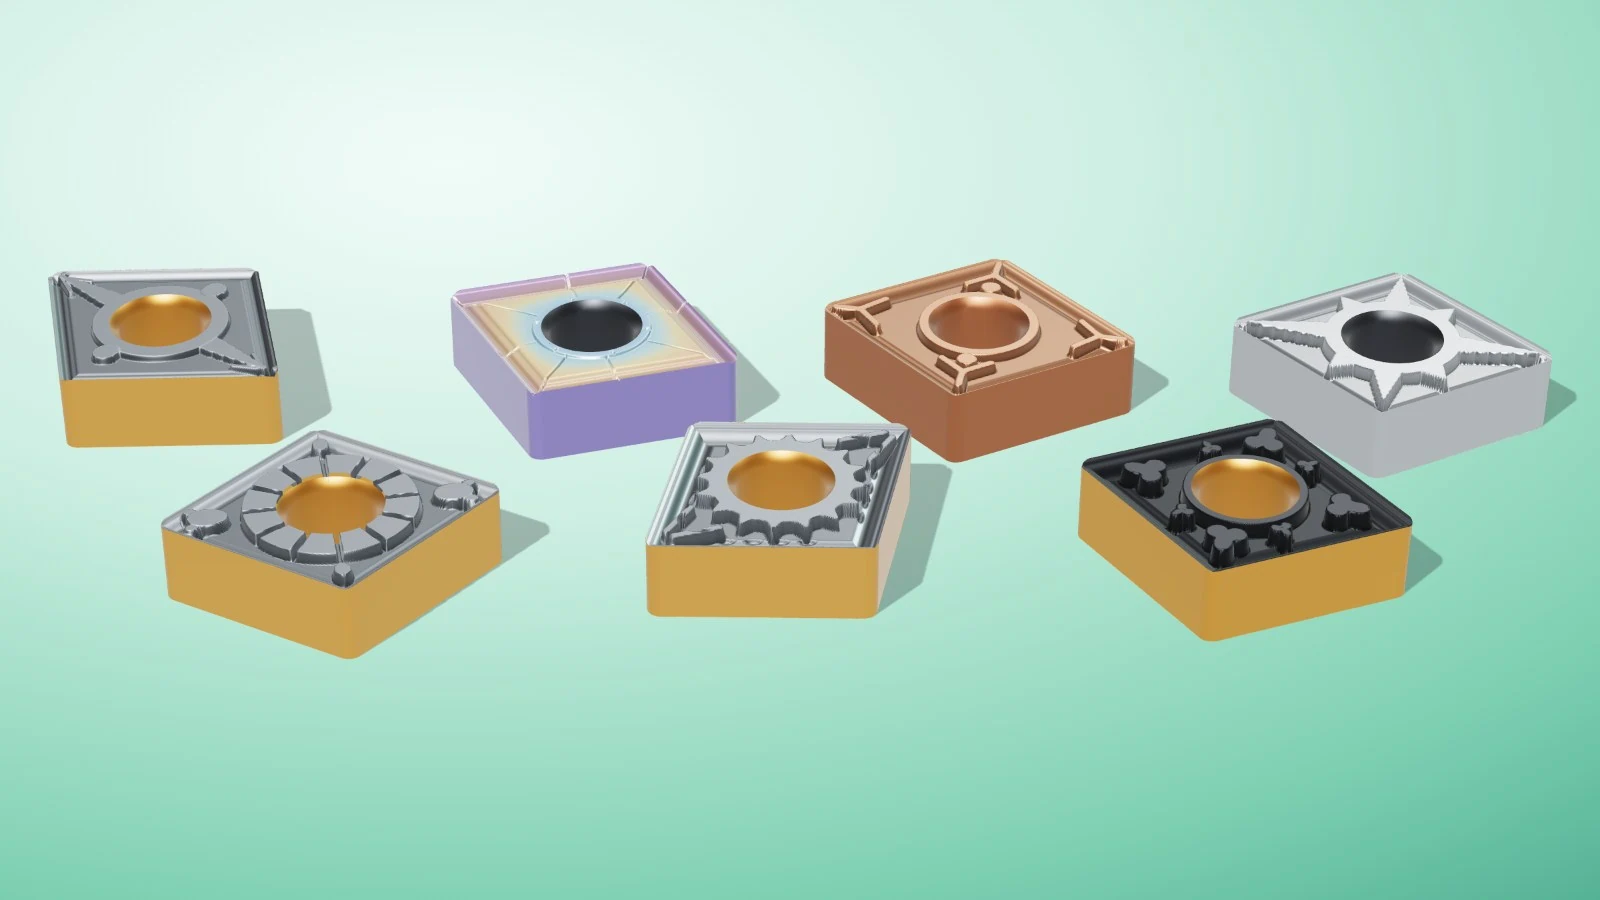
The complete family of INNOT CNMG inserts is now online: chipbreakers from finishing to heavy roughing, dedicated grades for every ISO material and cutting data for every combination.






