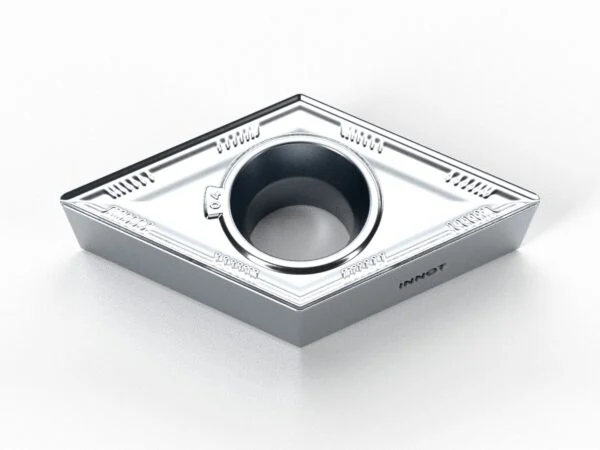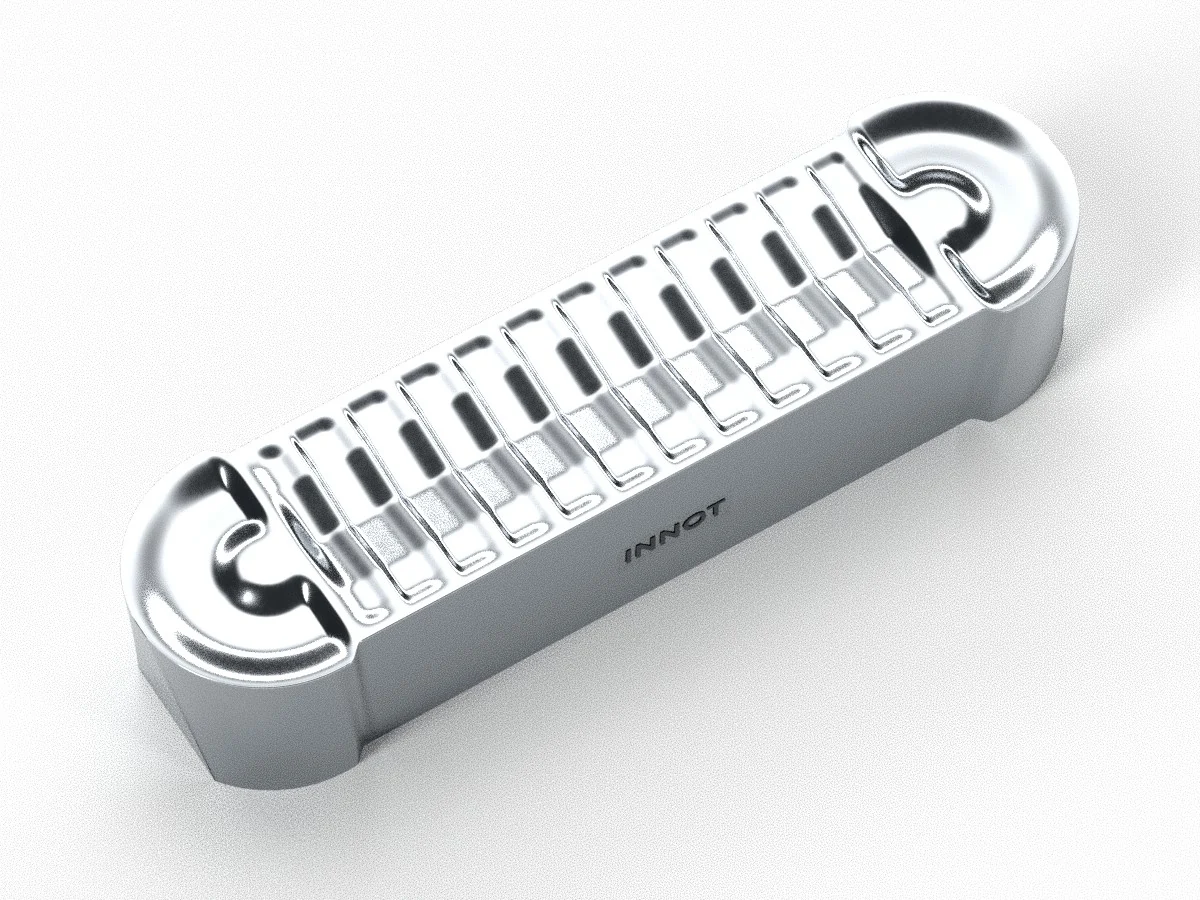
QPEB-AK
Full-radius insert for grooves on aluminium alloy wheels, with sharp AK cutting edge and INNOT carbide grades.
ISO N
Alloy wheels
Uncoated
★ ITK10 · ITK20
Technical data sheet PDFCutting data, sizes and grades
Want to try it first? Request a free tester

Description
Specifications
| Code | Width CW | Corner radius RE | INSL | Available grades |
|---|---|---|---|---|
| QPEB8040-AK | 8.0 mm (±0.025) | 4.0 | 30.0 | ITK10 – ITK20 |
CW = cutting width, RE = corner radius, INSL = insert length (mm).
AK chipbreaker data sheet
| Operation | Grooves and profiles on aluminium alloy wheels |
| ISO material | N (aluminium and non-ferrous metals) |
| Type | Two cutting edges, full-radius tip |
| Tolerance | E – width ±0.025 mm |
| Features | Sharp, polished cutting edge for aluminium: low friction, no built-up edge and an excellent finish. Fine-grain uncoated carbide grades. |
| Compatible toolholders | Grooving toolholders on request |
Available INNOT grades
| Grade | ISO | Coating | Composition | Application |
|---|---|---|---|---|
| ITK10 ★ | N | Uncoated | Fine-grain carbide | First-choice grade for turning aluminium alloys. Uncoated carbide with a fine, uniform grain matrix: high transverse rupture strength and good wear resistance. |
| ITK20 ★ | N | Uncoated | Carbide | Universal grade for turning aluminium alloys. Uncoated carbide with excellent wear resistance, better chipping resistance, great versatility and reliability. |
★ Recommended grade for this insert. CVD = chemical vapour deposition coating, PVD = physical vapour deposition coating.
Recommended cutting data
Grooves and profiles on alloy wheels (ISO N) – AK chipbreaker
Starting values for cast and wrought aluminium alloys, with coolant.
| Operation | Grade | Vc (m/min) | fn (mm/rev) | ap (mm) |
|---|---|---|---|---|
| Radial plunge (groove) | ITK10 · ITK20 | 250 – 600 | 0.08 – 0.20 | – |
| Side turning and profiling | ITK10 · ITK20 | 300 – 700 | 0.15 – 0.35 | 0.50 – 3.00 |
Speeds of the ITK10 and ITK20 grades on aluminium alloys, reduced for radial plunging. With high-silicon alloys (above 10%) start from the minimum values.
Tips for use
- Parting off: when approaching the centre reduce the feed by 30% for longer life and a better finish; keep the tool overhang to a minimum.
- External grooving and side turning: with depths over 0.5 mm work in radial passes (up to 0.75 × insert width), retract 0.1 mm, then an axial pass.
- Wide grooves: make side-by-side stepped plunges, then finish the bottom and the flanks.
- Face grooves: start from the largest diameter and move inwards; for finishing machine the bottom and the outer diameter first, then the inner one.
- Internal grooves: work from the inside outwards to help the chip out.
You may also like