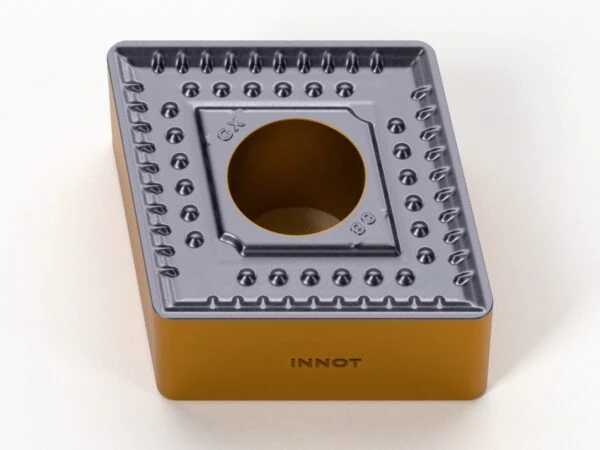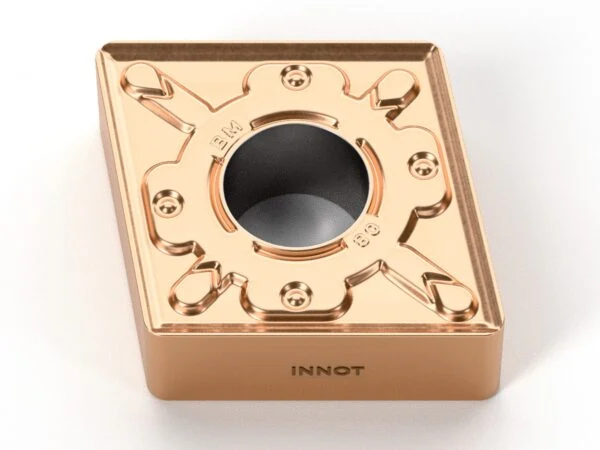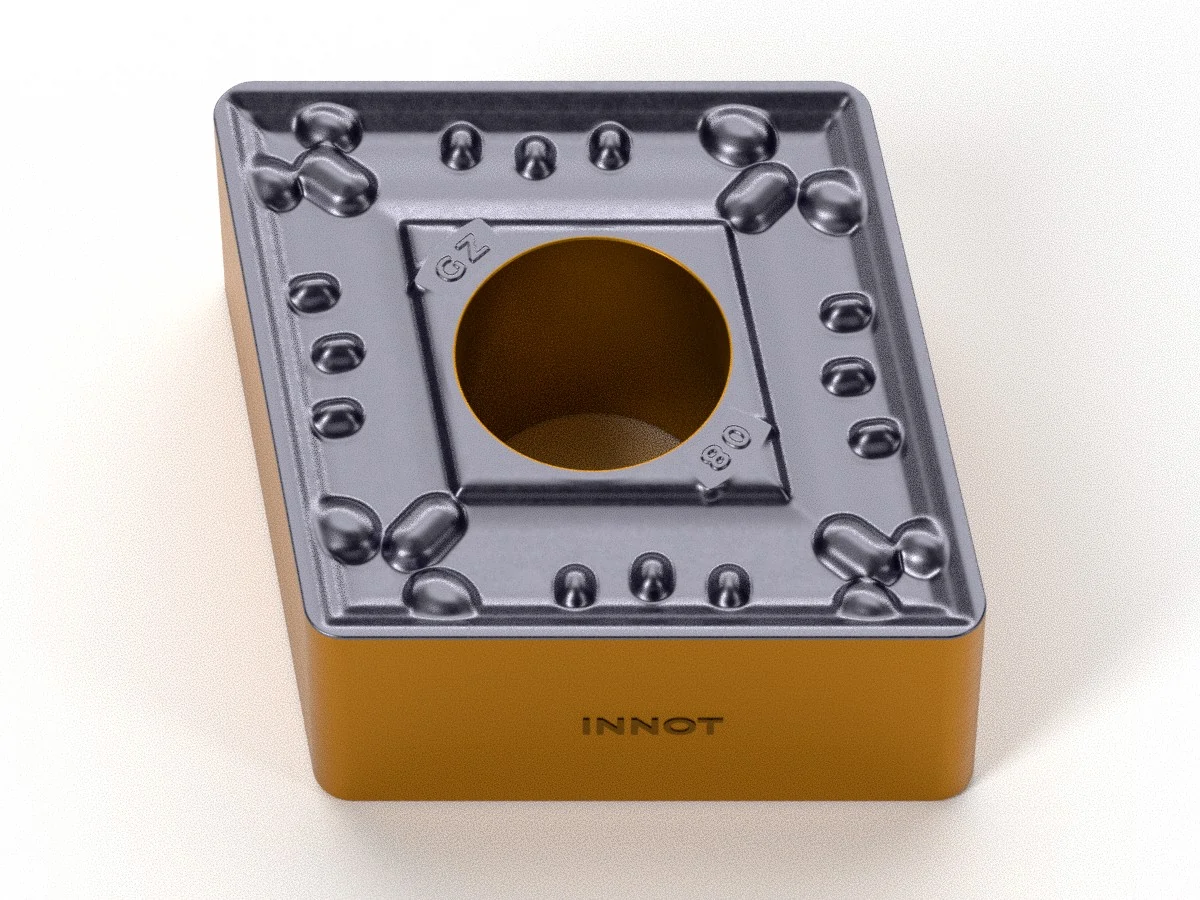
CNMM-GZ
80° negative insert for heavy roughing of steels, with GZ chipbreaker and INNOT CVD grades. Large depths of cut and high feeds.
Heavy roughing
CVD
★ IT8115 · IT8225
Technical data sheet PDFCutting data, sizes and grades
Want to try it first? Request a free tester

Description
ISO specifications
| ISO | RADIUS (RE) | AVAILABLE GRADES | CHIPBREAKER |
|---|---|---|---|
| CNMM1606 | 1.6 | IT8115 – IT8125 – IT8225 – IT8135 | GZ |
| CNMM1906 | 0.8 – 1.2 – 1.6 – 2.4 | IT8115 – IT8125 – IT8225 – IT8135 | GZ |
| CNMM2509 | 2.4 – 3.2 | IT8115 – IT8125 – IT8225 – IT8135 | GZ |
GZ chipbreaker data sheet
| Operation | Heavy roughing |
| ISO material | P (non-alloy, alloy and tool steels) |
| Tolerance | M |
| Features | Chipbreaker for heavy-duty machining of ISO P materials. The rake face with exclusively designed bosses reduces the chip contact area at large depths of cut and ensures excellent chip control. The sharp cutting edge effectively reduces cutting forces. Suitable for depths of cut up to 12 mm on the largest sizes. |
Available INNOT grades
| Grade | ISO | Coating | Composition | Application |
|---|---|---|---|---|
| IT8115 ★ | P | CVD | TiN + MT-TiCN + Al₂O₃ | Continuous and lightly interrupted cuts. Finishing and semi-finishing of carbon and alloy steels. |
| IT8125 | P | CVD | TiN + MT-TiCN + Al₂O₃ | Interrupted and continuous cuts on steel. The reinforced substrate limits plastic deformation at high temperature. |
| IT8225 ★ | P | CVD | TiN + MT-TiCN + Al₂O₃ | First-choice grade for steel, very versatile. Multilayer coating with excellent wear resistance and toughness. |
| IT8135 | P | CVD | TiN + MT-TiCN + Al₂O₃ | Grade for turning steel with heavy impacts. High-toughness substrate and reinforced binder phase: excellent impact resistance in heavily interrupted cuts. |
★ Recommended grade for this chipbreaker. CVD = chemical vapour deposition coating. ISO P = steels.
Recommended cutting data
Heavy external turning of steels (ISO P)
Recommended cutting data for the GZ chipbreaker, by material and cutting condition.
| Material | Condition | Vc (m/min) by grade | fn (mm/rev) | ap (mm) |
|---|---|---|---|---|
| Non-alloy and alloy steels ≤ 280 HB (S235, C45, 41Cr4, 42CrMo4…) |
Stable | IT8115: 100 – 200 IT8125: 100 – 180 IT8225: 100 – 195 |
0.25 – 1.00 | 3.00 – 12.00 |
| Non-alloy and alloy steels ≤ 280 HB (S235, C45, 41Cr4, 42CrMo4…) |
Average | IT8115: 100 – 200 IT8125: 100 – 180 IT8225: 100 – 195 |
0.25 – 0.95 | 3.00 – 12.00 |
| Non-alloy and alloy steels ≤ 280 HB (S235, C45, 41Cr4, 42CrMo4…) |
Difficult | IT8115 · IT8125 · IT8225: 60 – 180 | 0.25 – 0.90 | 3.00 – 12.00 |
| Quenched and tempered steels ≥ 280 HB | Stable | IT8115: 120 – 245 IT8225: 100 – 190 |
0.50 – 1.26 | 3.00 – 11.00 |
| Quenched and tempered steels ≥ 280 HB | Average | IT8115: 110 – 245 IT8225: 90 – 190 |
0.50 – 1.21 | 3.00 – 11.00 |
For steels ≥ 280 HB IT8115 and IT8225 are recommended. IT8135 is the grade for heavy impacts and heavily interrupted cuts: cutting data on request.
Heavy internal turning (boring) of steels (ISO P)
Starting values for internal turning with a boring bar, derived from this insert's external turning data: cutting speed −15%, feed −20%, maximum depth of cut −40%. Negative inserts are mounted on boring bars for bores from about Ø 25 mm upwards (Ø 32–40 mm for the larger sizes). Heavy roughing needs rigid boring bars in large bores, indicatively above Ø 60 mm.
| Material | Condition | Vc (m/min) by grade | fn (mm/rev) | ap (mm) |
|---|---|---|---|---|
| Non-alloy and alloy steels ≤ 280 HB (S235, C45, 41Cr4, 42CrMo4…) |
Stable | IT8115: 85 – 170 IT8125: 85 – 155 IT8225: 85 – 165 |
0.20 – 0.80 | 3.00 – 7.20 |
| Non-alloy and alloy steels ≤ 280 HB (S235, C45, 41Cr4, 42CrMo4…) |
Average | IT8115: 85 – 170 IT8125: 85 – 155 IT8225: 85 – 165 |
0.20 – 0.76 | 3.00 – 7.20 |
| Non-alloy and alloy steels ≤ 280 HB (S235, C45, 41Cr4, 42CrMo4…) |
Difficult | IT8115 · IT8125 · IT8225: 50 – 155 | 0.20 – 0.72 | 3.00 – 7.20 |
| Quenched and tempered steels ≥ 280 HB | Stable | IT8115: 100 – 210 IT8225: 85 – 160 |
0.40 – 1.01 | 3.00 – 6.60 |
| Quenched and tempered steels ≥ 280 HB | Average | IT8115: 95 – 210 IT8225: 75 – 160 |
0.40 – 0.97 | 3.00 – 6.60 |
With a boring bar overhang above 3 times the diameter (steel bar) or 5 times (carbide or anti-vibration bar), reduce speed and feed further. Use the bar's internal coolant to clear the chips.
You may also like