
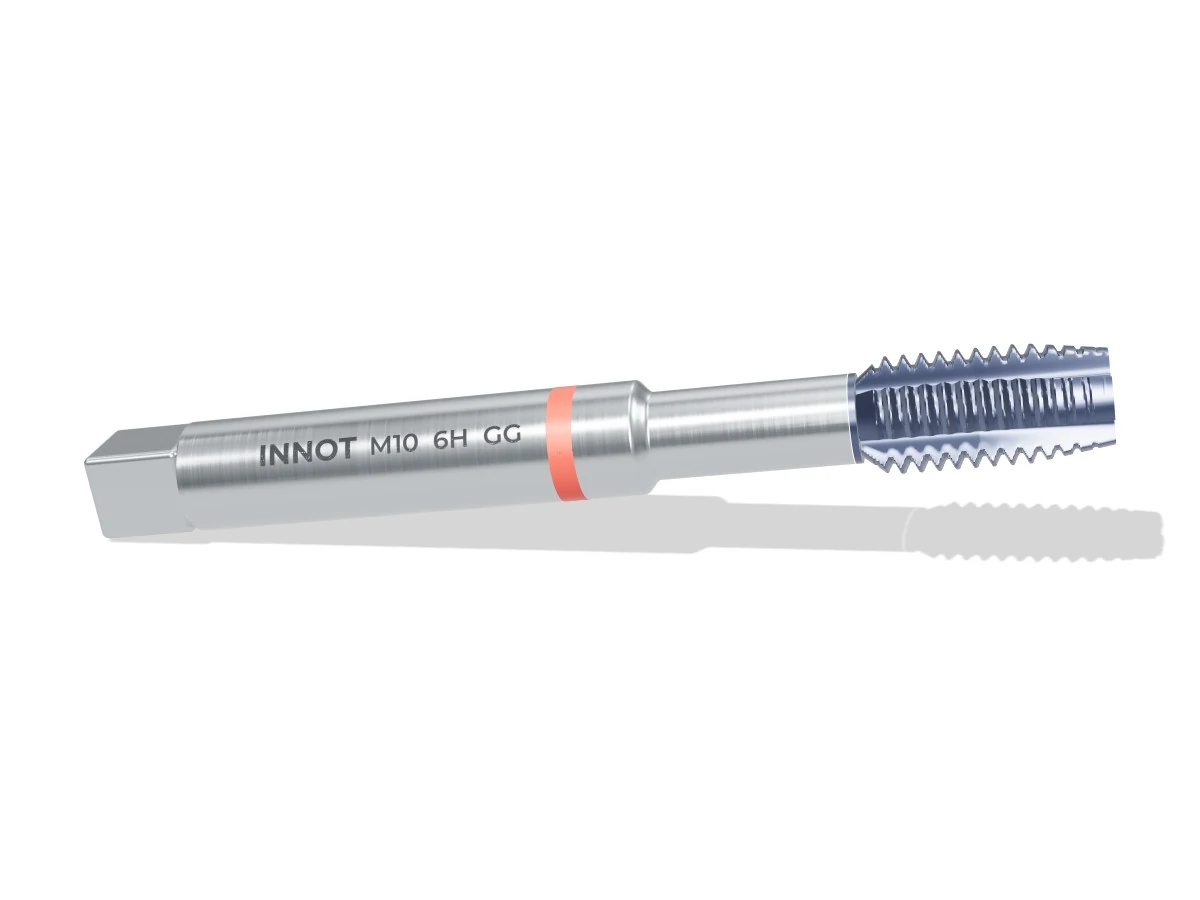
Cast iron tap – through and blind holes
Straight flute tap for cast irons and short-chipping materials, in through and blind holes. Broken chips, TiCN against abrasion.
ISO K
ISO N
Through and blind
TiCN
M2 – M36
Technical data sheet PDFCutting data, sizes and grades
Want to try it first? Request a free tester

Description
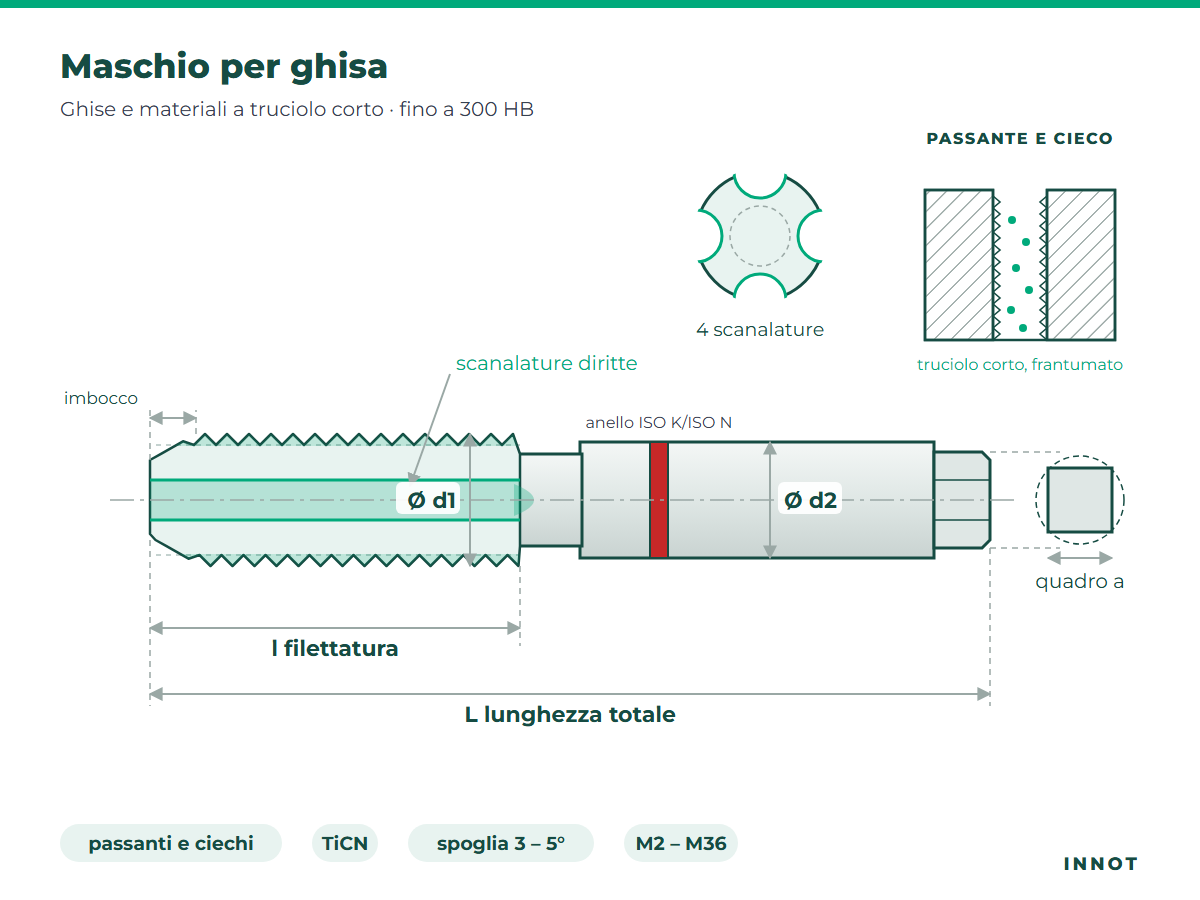
Technical drawing
At a glance
| Hole type | Through holes and blind holes |
| Geometry | Straight flutes · 4 straight flutes |
| Chamfer | Form C, 2 – 3 threads |
| Chip | Short and broken: stays in the flutes or comes out as powder |
| Thread depth | Up to 2.5 × d |
| Rake angle | 3 – 5° |
| Tool material | HSS-E; solid carbide on request for high-volume production |
| Coating | TiCN (first choice) · alternatively nitrided, TiN |
| Tolerance | 6H (6HX on request); 6G and 7G for threads to be galvanised or painted |
| Design | Reinforced shank from M2 to M10 (DIN 371), reduced shank from M12 (DIN 376); from M3 to M10 also with reduced shank for deep holes |
| Cutting direction | Right-hand; left-hand on request |
Workpiece materials
| Group | Cast irons and short-chipping materialsISO KISO N |
| Strength | up to 300 HB |
| Examples | grey cast iron EN-GJL (GG20 – GG30), ductile cast iron EN-GJS (GGG40 – GGG60), malleable cast iron; also die-cast aluminium with Si over 10 % and short-chipping brass |
Sizes – ISO metric thread
| Thread | Pitch P | Tap drill Ø | L overall | l thread | Ø d2 shank | Square a |
|---|---|---|---|---|---|---|
| M2 | 0,4 | 1,6 | 45 | 8 | 2,8 | 2,1 |
| M2,5 | 0,45 | 2,05 | 50 | 9 | 2,8 | 2,1 |
| M3 | 0,5 | 2,5 | 56 | 11 | 3,5 | 2,7 |
| M3,5 | 0,6 | 2,9 | 56 | 12 | 4 | 3 |
| M4 | 0,7 | 3,3 | 63 | 13 | 4,5 | 3,4 |
| M5 | 0,8 | 4,2 | 70 | 16 | 6 | 4,9 |
| M6 | 1 | 5 | 80 | 19 | 6 | 4,9 |
| M8 | 1,25 | 6,8 | 90 | 22 | 8 | 6,2 |
| M10 | 1,5 | 8,5 | 100 | 24 | 10 | 8 |
| M12 | 1,75 | 10,2 | 110 | 28 | 9 | 7 |
| M14 | 2 | 12 | 110 | 30 | 11 | 9 |
| M16 | 2 | 14 | 110 | 32 | 12 | 9 |
| M18 | 2,5 | 15,5 | 125 | 34 | 14 | 11 |
| M20 | 2,5 | 17,5 | 140 | 34 | 16 | 12 |
| M22 | 2,5 | 19,5 | 140 | 34 | 18 | 14,5 |
| M24 | 3 | 21 | 160 | 38 | 18 | 14,5 |
| M27 | 3 | 24 | 160 | 38 | 20 | 16 |
| M30 | 3,5 | 26,5 | 180 | 45 | 22 | 18 |
| M33 | 3,5 | 29,5 | 180 | 50 | 25 | 20 |
| M36 | 4 | 32 | 200 | 56 | 28 | 22 |
Dimensions in mm. M39 to M100 and fine, pipe and inch threads on request. The tap drill Ø is the one recommended for tolerance 6H.
Coatings for cast irons
| Coating | When to choose it |
|---|---|
| TiCN – titanium carbonitride ★ | Harder and more abrasion-resistant than TiN: quenched and tempered steels, cast irons and series production. |
| Nitriding | Treatment that hardens the tool surface: cast irons and abrasive short-chipping materials. |
| TiN – titanium nitride | The universal coating: less friction and less sticking, longer life on structural steels and common materials. |
★ INNOT first choice for this material. Every tap can be supplied with any coating in the range: specify it in your request.
Starting data
| Cutting speed Vc | 8 – 20 m/min (lower value for uncoated substrate or machines with a compensating chuck) |
| Feed | Equal to the thread pitch: synchronised tapping or chuck with axial compensation |
| Lubrication | Emulsion; grey cast iron also dry with extraction |
| Thread | Spindle speed (n) |
|---|---|
| M6 | 420 – 1.060 |
| M10 | 250 – 640 |
| M16 | 160 – 400 |
| M24 | 110 – 270 |
Guide values to be adapted to machine, clamping and lubrication. n = Vc × 1000 / (π × d).
Tips for use
- Straight flutes retain the broken chips: in deep blind holes blow out or clean the hole between parts.
- Grey cast iron also dry with dust extraction; on ductile iron use emulsion.
- Also suitable for die-cast aluminium with silicon over 10 % and for short-chipping brass.
- Check the tap drill: in cast iron a hole that is too small tears the thread flanks.
- Chamfer the hole entry at 90°: clean start and no burr on the first thread.
Selection guide
Fine, pipe, inch and left-hand threads: special and custom threads.
Need a different tap?
Thread, tolerance, length, substrate and coating: tell us the material, hole type and depth and we will propose the right tap with a quote within 30 minutes.
You may also like
Forming tap – through and blind holes
BSPT 55° pipe threading inserts
Recently viewed
Cast iron tap – through and blind holes
Blind hole tap – Stainless steels






