
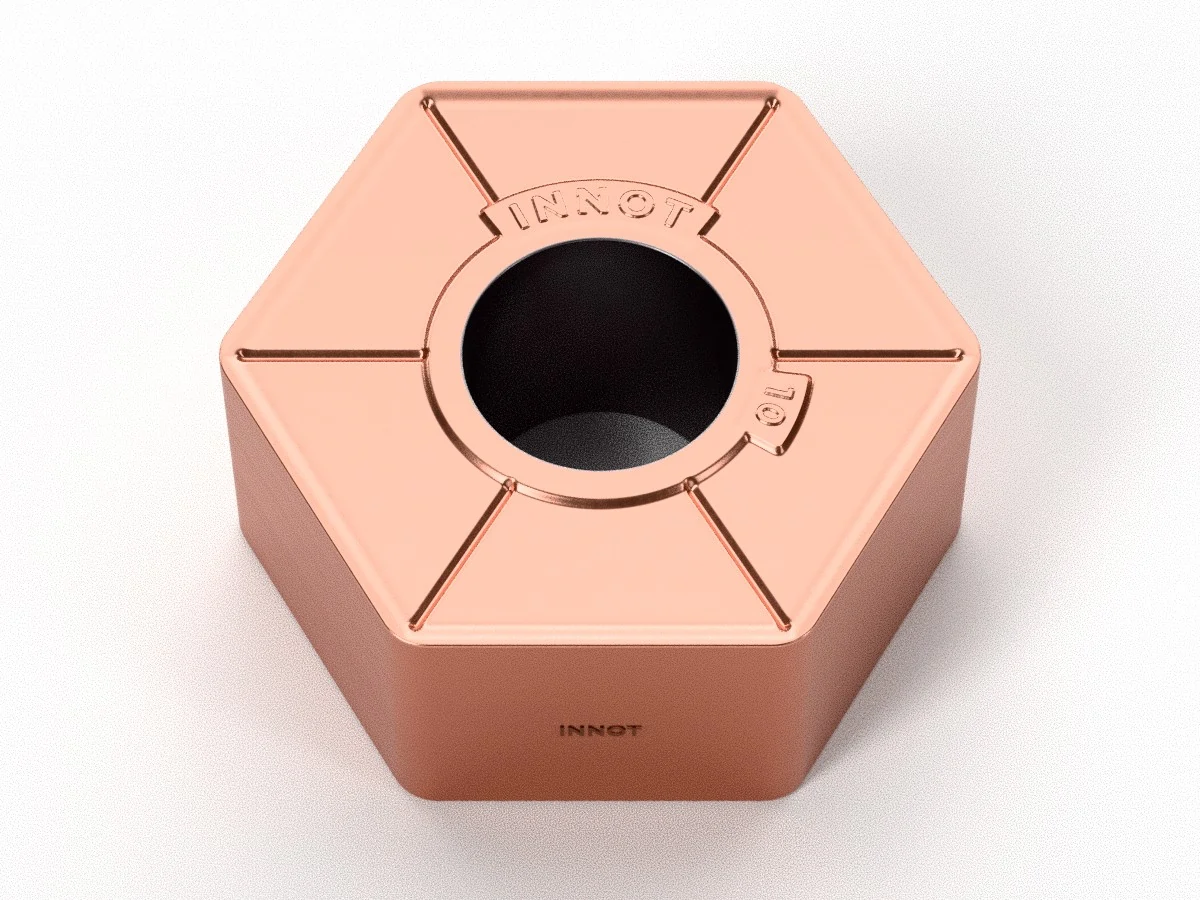
HNMX / HNGX
Double-sided hexagonal insert for face milling: 12 cutting edges, F (finishing), M (medium) and R (roughing) geometries.
ISO P
ISO M
ISO K
ISO H
Face milling
Face milling
★ IT6130 · IT5120 · IT5220 · IT5130
Technical data sheet PDFCutting data, sizes and grades
Want to try it first? Request a free tester
Fits on

Description
Specifications
| Code | IC | S | D1 | BS | RE | APMX |
|---|---|---|---|---|---|---|
| HNMX0906ANSN-F | 16.5 | 6.34 | 4.9 | 1 | 1.2 | 5 |
| HNMX0906ANSN-M | 16.5 | 6.34 | 4.9 | 1 | 1.2 | 5 |
| HNMX0906ANSN-R | 16.5 | 6.34 | 4.9 | 1 | 1.2 | 5 |
| HNGX0906ANSN | 16.5 | 6.34 | 4.9 | 1.2 | 1 | 5 |
Dimensions in mm. IC = inscribed circle, S = thickness, D1 = hole, BS = wiper flat, RE = corner radius, AN = clearance angle, APMX = maximum depth of cut.
Technical data
| Operation | Milling – Face milling |
| Shape | Hexagonal |
| ISO material | P (steels), M (stainless steels), K (cast irons), H (hardened steels) |
| Features | Double-sided negative hexagonal insert: 12 usable cutting edges for a very low cost per edge. |
| Compatible cutters | Indexable cutters with HNMX seat: send us your cutter code and we will check compatibility. |
Available INNOT grades
| Grade | ISO | Coating | Composition | Application |
|---|---|---|---|---|
| IT6130 ★ | P · K | CVD | TiN + MT-TiCN + Al₂O₃ | Semi-finishing and roughing of steels and cast irons. High-strength composite coating that balances wear and toughness; post-coating treatment increases insert toughness. |
| IT5120 ★ | P · M · K | PVD | TiAlN + CrAlN + TiSiN | Universal grade for steels, stainless steels and cast irons, also ideal on materials of 35–50 HRC. Excellent wear resistance and toughness, high hot hardness. |
| IT5220 ★ | P · M · K | PVD | AlTiN + TiSiN | Universal grade for steels, stainless steels and cast irons up to 40–50 HRC. Double-layer coating: strength, toughness and protection against edge chipping. |
| IT5130 ★ | P · M | PVD | AlTiN | High-efficiency milling of steels and stainless steels below 30 HRC. Specially formulated substrate that reduces the risk of chipping, with a latest-generation nano coating. |
| IT5110 | P · H | PVD | TiAlN + CrAlN + TiSiN | Milling of hardened steels 45–55 HRC. Nano-composite coating on an ultra-fine grain substrate: smooth surface, low friction, high nano-hardness and excellent oxidation resistance. |
| IT5210 | P · H | PVD | AlTiN + TiSiN | Milling of hardened steels 50–65 HRC. Coating with high thermal stability and oxidation resistance: withstands the most severe cutting temperatures. |
★ Recommended grade. Other grades are available on request.
Recommended cutting data
Milling – cutting speed and feed per tooth
| Material | Hardness HB | Grade | Vc (m/min) | fz (mm/tooth) |
|---|---|---|---|---|
| P Low-carbon / mild steel | ≤ 180 | IT5120 IT5220 IT5130 |
270 (220–350) 240 (200–320) 220 (200–320) |
0.3 (0.1–0.5) |
| P High-carbon / alloy steel | 180–280 | IT5110 IT5120 IT5220 IT5130 |
240 (200–320) 200 (160–280) 200 (160–280) 200 (160–260) |
0.2 (0.1–0.4) |
| P Alloy tool steel | 280–350 | IT5110 IT5210 IT5120 IT5220 |
220 (170–340) 200 (150–280) 180 (150–250) 180 (150–250) |
0.15 (0.1–0.3) |
| M Stainless steel | ≤ 270 | IT5120 IT5130 |
180 (120–240) 150 (120–180) |
0.2 (0.1–0.3) |
| K Cast iron | 180–250 | IT6130 IT5110 IT5120 |
280 (180–320) 200 (150–250) 200 (150–250) |
0.2 (0.1–0.4) |
Guide values: recommended (min–max range). Reduce by 20–30% with long overhangs, weak clamping or dry machining.
You may also like
BLMP (high feed)
Available
HHardenedPSteelKCast ironMStainlessSSuperalloysSemi-finishing · Roughing
UNM-CE (copy milling)
Available
PSteelKCast ironMStainlessSSuperalloysSemi-finishing · Roughing
SZMX
Available
HHardenedPSteelKCast ironMStainlessFace milling · Roughing
RDHX (15° round)
Available
HHardenedPSteelKCast ironMStainlessSSuperalloysFinishing · Semi-finishing · Roughing
SPMT / APMT-MM
Available
HHardenedPSteelKCast ironMStainlessRoughing
Recently viewed
UN 60° threading inserts (UNC, UNF)
Available
PSteelMStainlessSSuperalloysSpecial






