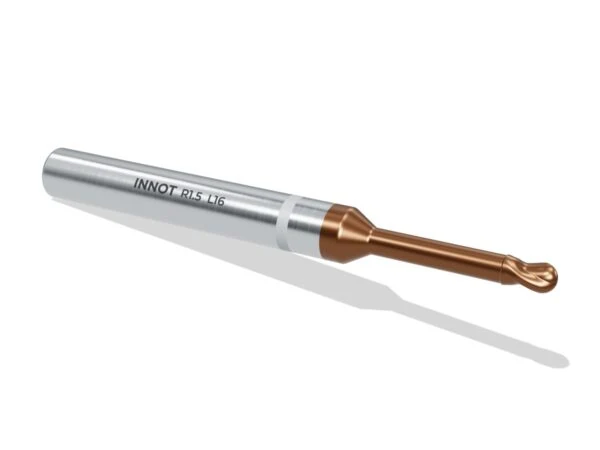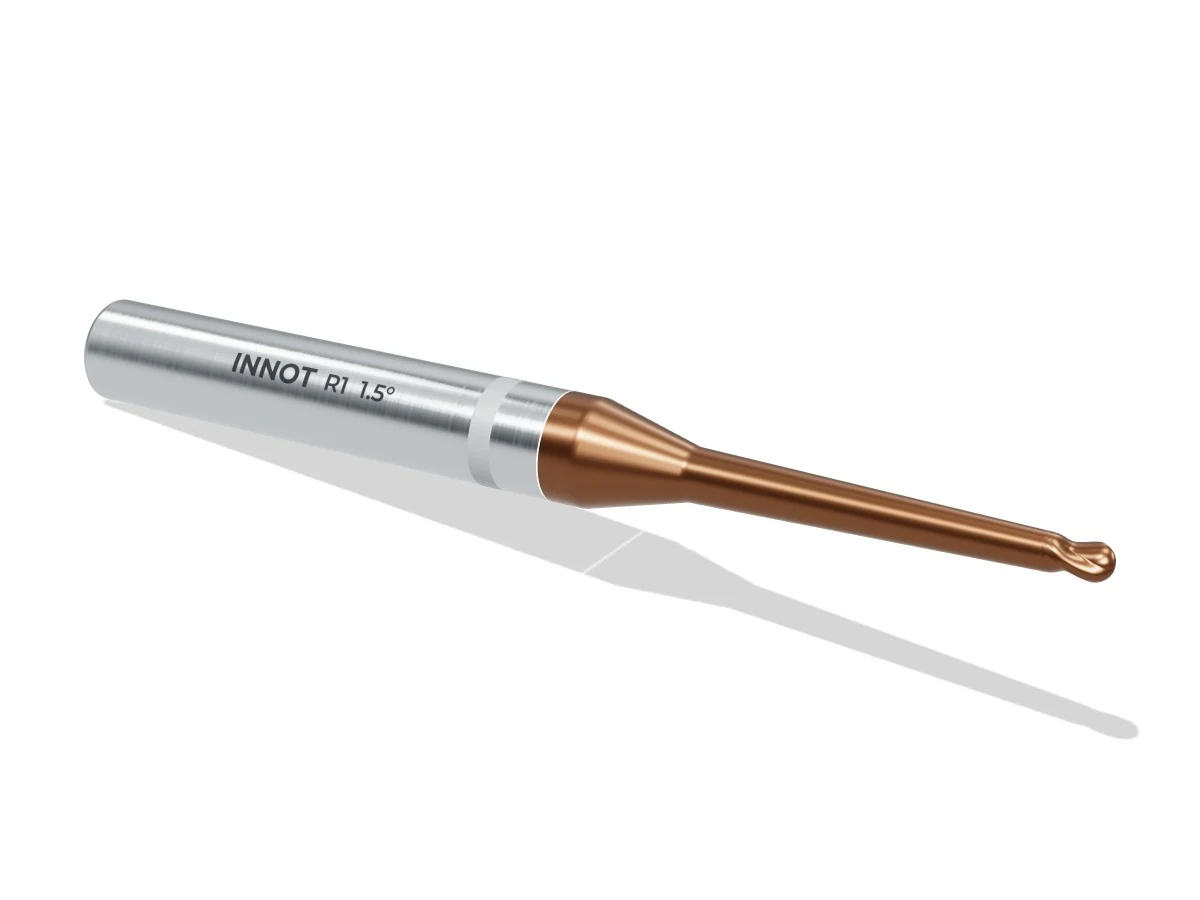
2-flute ball nose end mill with reinforced tapered neck
Ball nose end mill with reinforced tapered neck for copy milling and finishing of deep cavities with drafted walls: more rigidity, less vibration, up to 65 HRC.
ISO P
ISO M
ISO K
ISO N
ISO H
Ball nose
Ø 0.5 – 3 mm
Tapered neck
Up to 65 HRC
Technical data sheet PDFCutting data, sizes and grades
Want to try it first? Request a free tester

Description
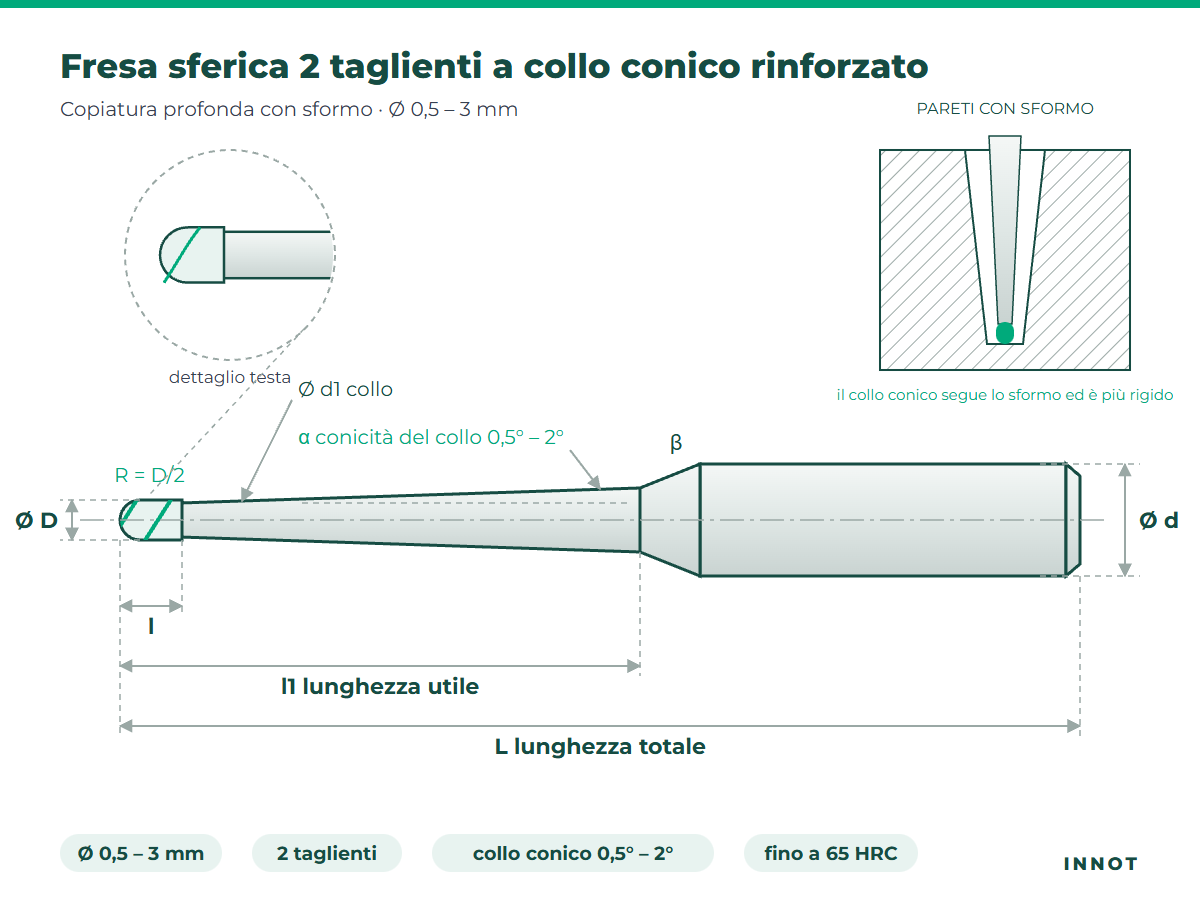
Technical drawing
Features
| Geometry | Ball nose (R = D/2), 2 flutes |
| Neck | Reinforced tapered: starts just below the cutting diameter and widens with a 0.5° to 2° taper up to the collar. It follows the wall draft and is more rigid than a cylindrical neck. |
| Diameters | Ø 0.5 – 3 mm in tight tolerance; intermediate diameters and above Ø3 custom made |
| Usable length | from 2 to 45 mm (up to 15 times the diameter) |
| Helix | 30°, right-hand cut |
| Shank | Ø 6 h6 with tapered collar |
| Materials | Mould steels, quenched and tempered and hardened steels up to 65 HRC, stainless steels, cast irons, copper and aluminium |
| Construction | Ultra-fine grain solid carbide, coating chosen for the material (high-silicon coating for hardened steels) |
Available sizes
| Ø D | l cutting | Ø d1 neck | l1 usable | Radius | Taper α | Ø d shank | L overall |
|---|---|---|---|---|---|---|---|
| Ø 0,5 | 0,35 | 0,45 | 2 – 14 | R 0,25 | 0,5° · 1° · 1,5° · 2° | 6 | 50 |
| Ø 0,6 | 0,4 | 0,55 | 2 – 15 | R 0,3 | 0,5° · 1° · 1,5° · 2° | 6 | 50 |
| Ø 0,8 | 0,5 | 0,75 | 4 – 20 | R 0,4 | 0,5° · 1° · 1,5° · 2° | 6 | 50 · 60 |
| Ø 1 | 0,8 | 0,95 | 8 – 35 | R 0,5 | 0,5° · 1° · 1,5° · 2° | 6 | 60 · 78 |
| Ø 1,2 | 1 | 1,15 | 10 – 40 | R 0,6 | 0,5° · 1° · 1,5° · 2° | 6 | 60 · 78 |
| Ø 1,5 | 1,35 | 1,45 | 10 – 40 | R 0,75 | 0,5° · 1° · 1,5° · 2° | 6 | 60 · 78 |
| Ø 2 | 1,7 | 1,9 | 10 – 45 | R 1 | 0,5° · 1° · 1,5° · 2° | 6 | 60 · 78 |
| Ø 2,5 | 2,1 | 2,4 | 10 – 45 | R 1,25 | 0,5° · 1° · 1,5° · 2° | 6 | 60 · 78 |
| Ø 3 | 2,5 | 2,9 | 10 – 45 | R 1,5 | 0,5° · 1° · 1,5° · 2° | 6 | 60 · 78 |
Dimensions in mm. For each diameter the usable lengths shown are available in 1 – 5 mm steps with four neck tapers. Other combinations, special radii and intermediate diameters custom made.
Why a tapered neck
- Mould walls almost always have a draft: the tapered neck follows it and reaches the bottom without touching the wall.
- For the same usable length the cross-section grows towards the shank: the tool deflects less, vibrates less and leaves a better finish.
- Choose the taper closest to the draft of your walls: more taper, more rigidity.
Coatings and carbide
All coatings are available on this tool, also in custom versions:
TiNTiCNTiAlNAlTiNAlCrNTiSiNAlTiSiNAlCrSiNCrNZrNTiB2DLCta-CCVD diamondUncoatedNeed a special length or radius?
Diameter, usable length, radius, neck taper, carbide rod and coating: configure the end mill and receive the quote within 30 minutes.
You may also like
Roughing end mill with wavy cutting edge
4- and 5-flute end mill for titanium
2-flute ball nose end mill
4-flute flat end mill – universal
Recently viewed