
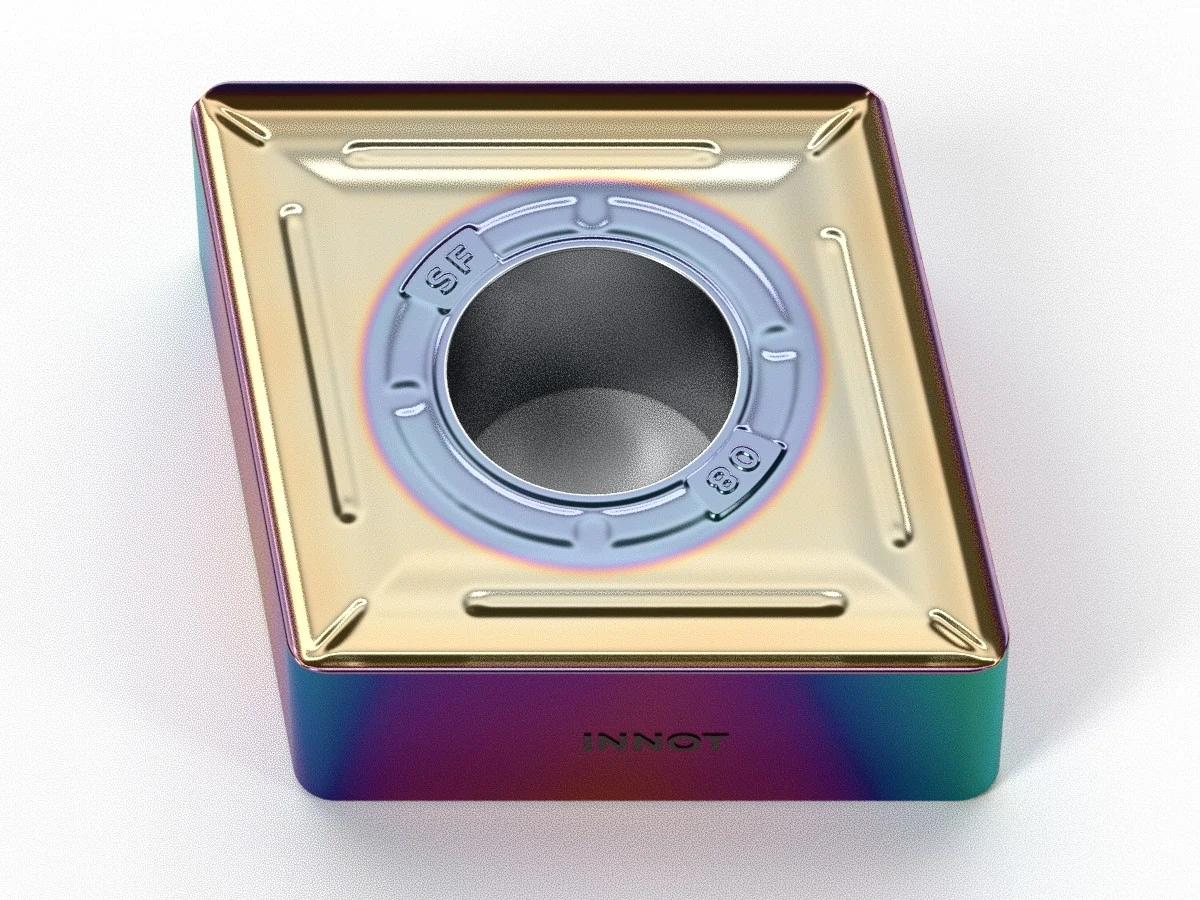
CNMG-SF
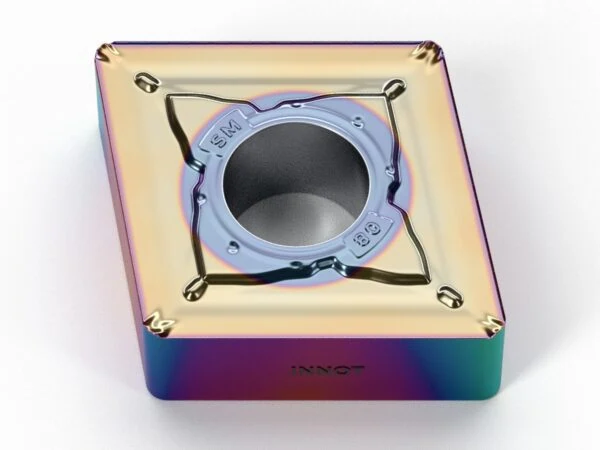
80° negative insert for finishing superalloys and titanium, with SF chipbreaker and INNOT PVD grades.
Finishing
PVD
★ IT9205 · IT9215
Technical data sheet PDFCutting data, sizes and grades
Want to try it first? Request a free tester

Description
ISO specifications
| ISO | RADIUS (RE) | AVAILABLE GRADES | CHIPBREAKER |
|---|---|---|---|
| CNMG1204 | 0.4 – 0.8 – 1.2 | IT7115 – IT9205 – IT9215 | SF |
SF chipbreaker data sheet
| Operation | Finishing |
| ISO material | S (heat-resistant superalloys and titanium alloys) |
| Tolerance | M |
| Features | Chipbreaker for finishing heat-resistant superalloys and titanium alloys. The specially designed corner radius and the sharp cutting edge reduce cutting forces and tool vibration, for a smooth surface and good chip evacuation. |
Available INNOT grades
| Grade | ISO | Coating | Composition | Application |
|---|---|---|---|---|
| IT7115 | M · S | PVD | AlTiSiN + TiSiN | Sub-micron grain substrate with nano-gradient coating: excellent wear and oxidation resistance, great stability. Suitable for titanium alloys and superalloys. |
| IT9205 ★ | S | PVD | AlTiN + TiSiN + AlCrN | Highly wear-resistant grade for superalloys. Uniform sub-micron hard phase and alloying elements for greater reliability; excellent thermal stability and oxidation resistance. |
| IT9215 ★ | S | PVD | AlTiN + TiSiN + AlCrN | Universal grade for turning superalloys. Greater toughness and reliability; the multilayer structure limits cracks and protects the coating from flaking and chipping. |
★ Recommended grade for this chipbreaker. PVD = physical vapour deposition coating. ISO S = superalloys and titanium. ISO M = stainless steels.
Recommended cutting data
External turning of superalloys (ISO S)
Heat-resistant superalloys (Inconel 718 and similar). Recommended cutting data for the SF chipbreaker.
| Condition | Grade | Vc (m/min) | fn (mm/rev) | ap (mm) |
|---|---|---|---|---|
| Stable | IT9205 | 40 – 80 | 0.02 – 0.20 | 0.20 – 1.80 |
| Stable | IT9215 | 30 – 70 | 0.02 – 0.20 | 0.20 – 1.80 |
| Average | IT9205 | 40 – 80 | 0.02 – 0.20 | 0.20 – 1.80 |
| Average | IT9215 | 30 – 70 | 0.02 – 0.20 | 0.20 – 1.80 |
| Difficult | IT9205 | 40 – 80 | 0.02 – 0.20 | 0.20 – 1.80 |
| Difficult | IT9215 | 30 – 70 | 0.02 – 0.20 | 0.20 – 1.80 |
IT9205 allows higher cutting speeds; IT9215 offers greater toughness. Start from the minimum Vc and increase according to wear. Always use plenty of coolant.
Internal turning (boring) of superalloys (ISO S)
Starting values for internal turning with a boring bar, derived from this insert's external turning data: cutting speed −15%, feed −20%, maximum depth of cut −40%. Negative inserts are mounted on boring bars for bores from about Ø 25 mm upwards (Ø 32–40 mm for the larger sizes).
| Condition | Grade | Vc (m/min) | fn (mm/rev) | ap (mm) |
|---|---|---|---|---|
| Stable | IT9205 | 35 – 70 | 0.02 – 0.16 | 0.20 – 1.10 |
| Stable | IT9215 | 25 – 60 | 0.02 – 0.16 | 0.20 – 1.10 |
| Average | IT9205 | 35 – 70 | 0.02 – 0.16 | 0.20 – 1.10 |
| Average | IT9215 | 25 – 60 | 0.02 – 0.16 | 0.20 – 1.10 |
| Difficult | IT9205 | 35 – 70 | 0.02 – 0.16 | 0.20 – 1.10 |
| Difficult | IT9215 | 25 – 60 | 0.02 – 0.16 | 0.20 – 1.10 |
With a boring bar overhang above 3 times the diameter (steel bar) or 5 times (carbide or anti-vibration bar), reduce speed and feed further. Use the bar's internal coolant to clear the chips.
Application case: nickel-iron superalloy
| Part | Main steam valve |
| Material | Nickel-iron-based superalloy (Incoloy 901 type) |
| Operation | External turning, emulsion |
| Insert | CNMG120408-SM · IT9215 |
| Vc | 41.7 m/min |
| fn | 0.2 mm/rev |
| ap | 2.5 mm |
| Result | Even wear, tool life +30% compared with the previous insert |
You may also like
Recently viewed
RDMW / RDKW
CNMG-BR
TNMG-GQ
TCGT-AK
5×D solid carbide drill






