Need help? Call us: (+39) 3757861361 or info@innot-it.com
Online tool shop for CNC machine shopsThe Evolution of Machining
Carbide inserts and cutting tools engineered for maximum edge life and shorter cycle times in your shop
- Quote within 30 minutes
- Grades for ISO P · M · K · N · S · H
- Solid carbide end mills up to 65 HRC
Find the right insert or tool now
Choose product type, material and operation: we filter the catalog for you.
Already using inserts from another brand? Find the INNOT equivalent
Recommended for youSee allNo product matches this combination: try removing a filter, or ask us for advice.Ask for adviceRecommended graderesultsUsing another brand? Find the INNOT equivalent
Choose the brand or type the code you use today: we instantly suggest the matching INNOT chipbreaker.
Our cutting solutions
Scroll to explore the INNOT families in 3D: every tool carries the INNOT marking.

01 / 06Turning Inserts
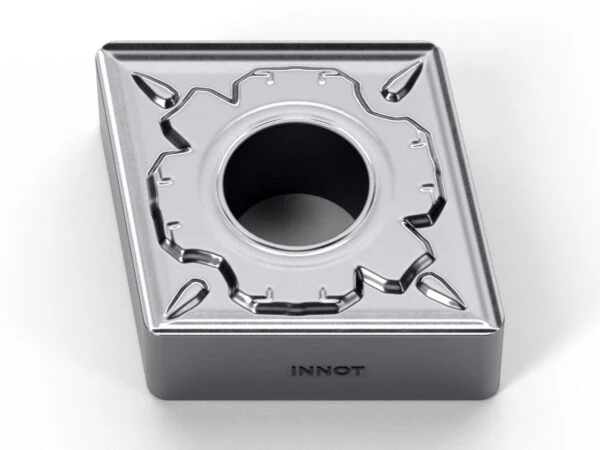
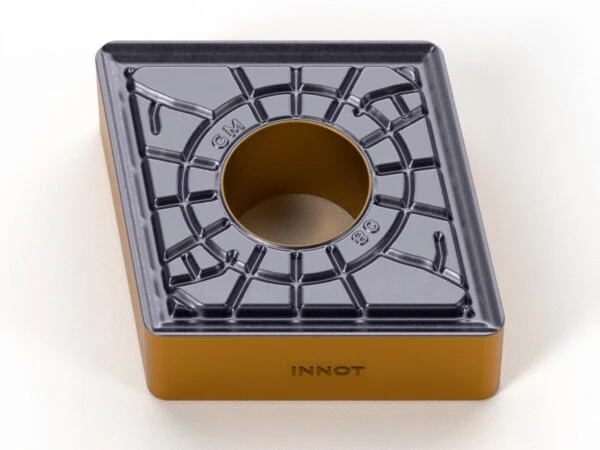
Negative and positive ISO inserts: chipbreakers for finishing, medium and roughing, CVD, PVD and cermet grades for every material.
- 121 items
- ISO P · M · K · N · S · H
- CNMG · DNMG · WNMG

02 / 06Milling Inserts
Indexable cutters for high feed, 45° face milling, 90° shoulder milling and copy milling, with coated carbide inserts.
- 24 items
- BLMP · SEKT · APMT · RDHX
- Torx screws

03 / 06Solid Carbide End Mills
Micrograin carbide with 2 to 6 flutes: square, corner radius and ball nose, also long-neck for mould making, up to 65 HRC.
- 14 items
- Up to 65 HRC
- AlTiN · TiSiN · AlCrN

04 / 06Drills
Solid carbide drills from 3×D to 30×D with internal coolant, step drills too, and indexable drills for larger holes.
- 9 items
- 3×D – 30×D
- Internal coolant

05 / 06Threading
Cutting and forming taps for through and blind holes, inserts for ISO, UN, Whitworth, NPT and BSPT threads.
- 19 items
- HSSE · HSSE-PM
- TiN · TiCN

06 / 06Toolholders and Chucks
Toolholders for external and internal turning, shank and shell mills and arbors, for the ISO inserts you already use.
- 15 items
- ISO coding
- Turning and milling
We machine all six material groups
For every ISO group we have dedicated grades, chipbreakers, geometries and coatings: from structural steels to hardened steels at 65 HRC.
Steels
Structural, alloyed, quenched and tempered and tool steels, free-cutting steels and castings.
up to 45 HRCSee the tools →KCast irons
Grey, ductile, malleable and compacted graphite iron: short, abrasive chips.
up to 300 HBSee the tools →MStainless steels
Austenitic, ferritic, martensitic and duplex: heat and work hardening under control.
AISI 300 e 400See the tools →NNon-ferrous
Aluminium and its alloys, copper, brass, bronze, plastics and composites.
also Si > 10 %See the tools →SSuperalloys and titanium
Inconel, Hastelloy, nickel and cobalt alloys, titanium and its alloys.
heat-resistantSee the tools →HHardened materials
Hardened and mould steels, chilled cast iron: solid carbide end mills up to 65 HRC.
from 45 to 65 HRCSee the tools →Can't find your material? Send us the material designation: we will tell you the right grade and geometry.
The chipbreaker makes the difference
Scroll and take a close look at how an INNOT insert is made: geometry, coating and designation.
A geometry for every material
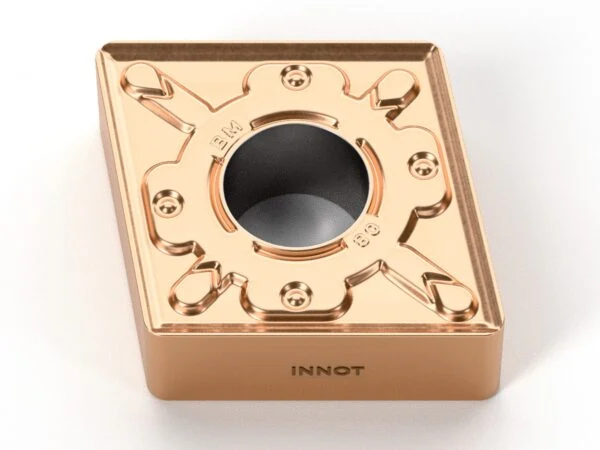
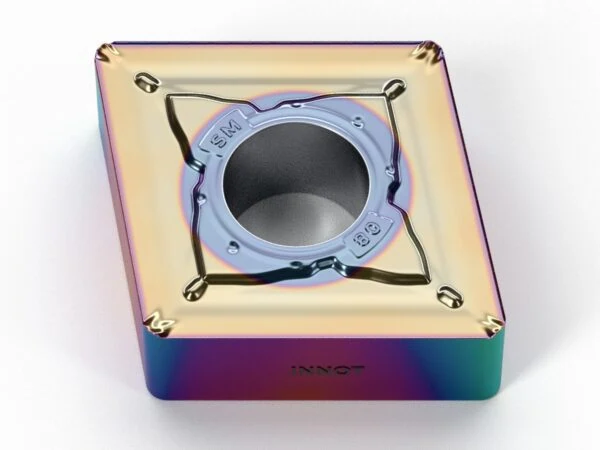
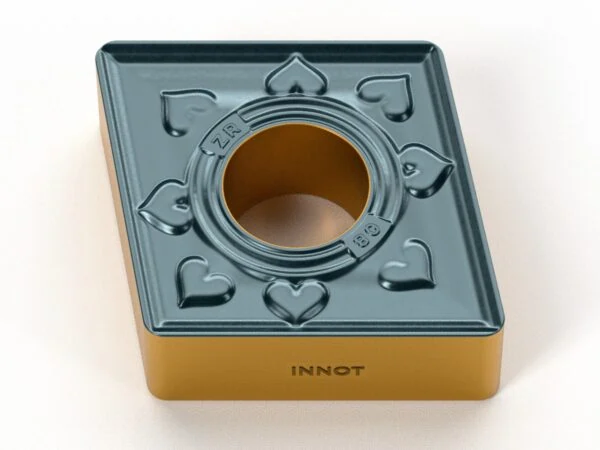
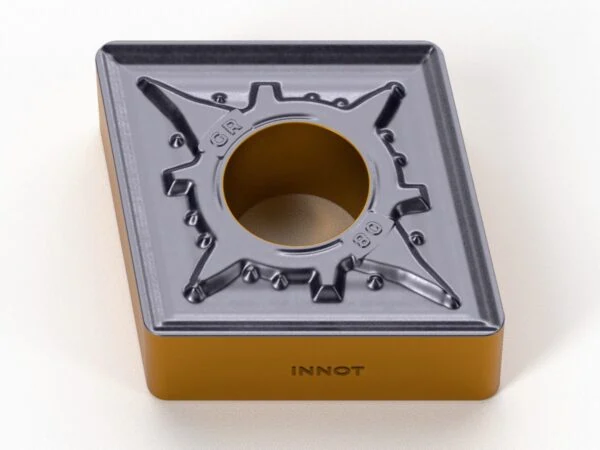
Rake face, islands and ribs guide the chip: it breaks at the right point, carries the heat away and the cutting edge lasts longer. Dedicated chipbreakers for finishing, semi-finishing and roughing.
- Finishing, medium and roughing
- Steels, stainless steels, cast irons, aluminium and superalloys
CVD and PVD coatings
Micro-grain carbide substrates and multilayer coatings: CVD alumina for steel and cast iron, sharp and tough PVD for stainless steels and superalloys, nano-coatings for hardened steels.
- Grades for ISO P · M · K · N · S · H
- Hardened steels up to 65 HRC
ISO designation, no lock-in
Standard ISO designations: INNOT inserts fit the toolholders you already use. Send us your code and we will tell you the equivalent within minutes.
Find the equivalent →Right cutting data, perfect chips
Turning in photorealistic 3D: the numbers you work out every day, on the part.
From cutting speed to spindle speed
The data sheet gives the cutting speed, the machine wants rpm: Ø60 bar at 200 m/min → 1,061 rpm. At 0.25 mm/rev the carriage feeds 265 mm/min.
n = Vc × 1000 / (π × D)The chip tells you if you are in the right window
Short, shaped like a 6 or a 9, curled by the chipbreaker: fn and ap are right. Long and tangled, or powdery: change feed, depth of cut or chipbreaker.
Q = Vc × ap × fnThe finish you want, before you turn
Nose radius 0.8 at 0.20 mm/rev: theoretical Ra 1.56 µm. With a larger radius you can feed faster for the same finish.
Ra ≈ fn² × 1000 / (32 × r)The right insert for your part
CNMG 120408-GR: negative 80° roughing insert, with the chipbreaker and grade chosen for your material. Set your cutting data with the free calculators.
From request to insert in the machine, in 3 steps
No minimum order and no cart to fill in: tell us what you need, we take care of the rest.
Choose or send us the code
Search the insert in the catalog or send us the ISO code, a drawing or a photo of the tool you use today. We will give you the INNOT equivalent.
Code, drawing or photoReceive the quote
We get back to you within 30 minutes with price, availability and the recommended grade for your material. For scheduled orders or larger batches we optimise the price.
Reply within 30 minutesConfirm and we ship
Confirm the order and we ship stock items within 24/48 h throughout Italy. Payment by bank transfer at 60-90 days, depending on volumes.
Shipping in 24/48 hOur most requested inserts
A selection from the INNOT range: a chipbreaker for every material and operation, with cutting data in every product sheet.
Solid carbide end mills and drills built around your part
Beyond the catalog, we make custom carbide end mills and drills to drawing: you specify dimensions and operation, we choose the rod, geometry and coating.
- Diameters from Ø1 to Ø32 mm, to the hundredth
- Lengths, reduced necks and radii on request
- Step drills and special profiles
- Internal coolant
- 4 carbide grades
- 15 coatings, from TiAlN to CVD diamond
Tools for every material, in every industry
From high-volume production to the toughest alloys: INNOT grades and chipbreakers chosen according to the material you machine.
Automotive and trucks
High volumes on shafts, hubs, transmissions and engine components. Highly wear-resistant CVD grades for fast, consistent cycles.
Aerospace
Nickel-based superalloys, Inconel and titanium. SF and SM chipbreakers with dedicated PVD grades to limit work hardening and notch wear.
Medical
Prostheses, implants and instruments in stainless steel and titanium. Sharp cutting edges and high-quality finishes for tight tolerances.
Railway
Wheels, axles and structural components. Robust inserts for heavy roughing with deep cuts and high feeds.
Hydraulics and energy
Valves, fittings, flanges and pump bodies in steel, stainless steel and superalloys. Solutions from roughing to finishing of sealing seats.
General engineering and moulds
Subcontract machining of small and medium batches. One versatile range for steels, stainless steels and cast irons, with advice on grade selection.
The right tool, first time.
We work with people who spend their day on the shop floor: shop supervisors, CAM programmers and CNC operators. That is why every INNOT insert has a complete technical data sheet and a technician who answers.
Ready-to-use cutting data
Cutting speed, feed and depth of cut for every chipbreaker, grade and material. Set them on the machine without searching elsewhere.
A grade for every material
CVD, PVD and cermet grades dedicated to steels, stainless steels, cast irons, aluminium, superalloys and hardened steels. For every insert we state the recommended grade.
Standard ISO designation
Shapes, sizes and radii according to ISO standards: INNOT inserts fit the toolholders you already use, without changing your tooling.
Direct technical support
Tell us the material, machine and operation: we help you choose shape, chipbreaker and grade. By phone, email or WhatsApp.
Everything you need to know
Answers to the questions shop managers and purchasing managers ask us most often.
Is there a minimum order?
No, you can order even a single box. For scheduled orders or larger batches we can however optimise the price: just mention it in your quote request.
How soon do I get the quote?
We get back to you within 30 minutes of your request, with price, availability and the recommended grade for your material.
What are the payment terms?
We work with bank transfer at 60-90 days. Terms are agreed according to business volumes.
How much does shipping cost and how long does it take?
For stock items we ship within 24/48 h throughout Italy. Above an order threshold shipping is free: we state it in the quote.
Can I try an insert before ordering it?
Yes. We offer free samples and testers to check the performance directly on your machine and your part. Request a tester
Are INNOT inserts compatible with my toolholders?
Yes. Shapes, sizes and radii follow the standard ISO designation: the inserts fit the toolholders you already use. Send us the code of your current insert and we will tell you the INNOT equivalent.
How do I choose the right grade and chipbreaker?
Every product sheet lists the cutting data by material, grade and working condition, with the recommended grade highlighted. For special cases we help you directly: tell us the material, machine and operation.
Can't find the answer? Call us on +39 375 786 1361 or write to info@innot-it.com
Do you have a code, a drawing or an insert to replace? Send it to us.
We reply within 30 minutes with the INNOT solution, price and availability. No minimum order.

Inserts and cutting tools for CNC machine shops. Dedicated grades for every ISO group, from steel to aluminium, from superalloys to hardened steels, with cutting data in every product sheet.
INNOT by Giammarco Turati
Via San Ponso, 57 – 10080 Pertusio (TO)
VAT No. IT13269100015
© 2026 INNOT by Giammarco Turati – VAT No. IT13269100015 – Pertusio (TO), Italy – Privacy Policy – Cookie Policy