
INNOT catalog
Inserts and tools catalog
Carbide turning and milling inserts, solid carbide end mills and drills, toolholders. Grades dedicated to every ISO group (steels, stainless steels, cast irons, aluminium, superalloys and hardened steels), cutting data in every product sheet and custom-made tools.
25products
Showing 1–24 of 25 results
Sort:
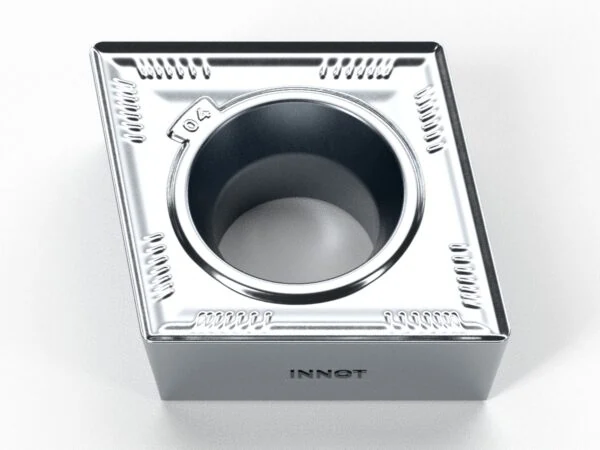
CCGT-AK
Available
NAluminiumFinishing
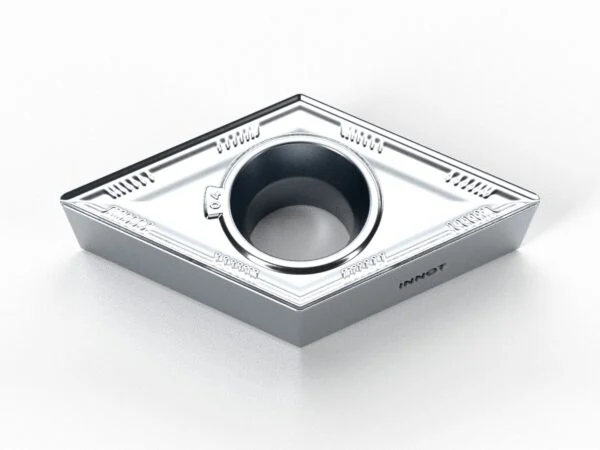
DCGT-AK
Available
NAluminiumFinishing
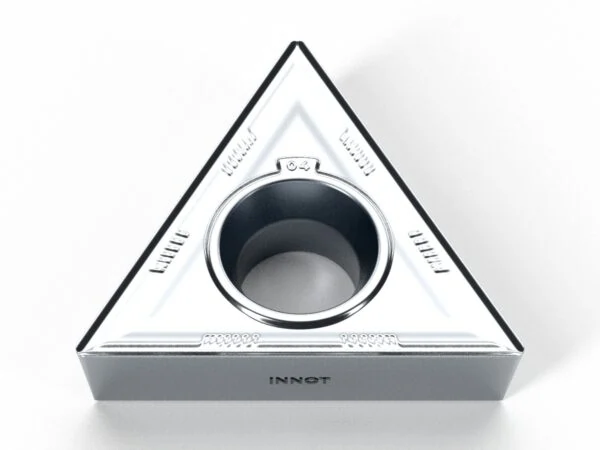
TCGT-AK
Available
NAluminiumFinishing
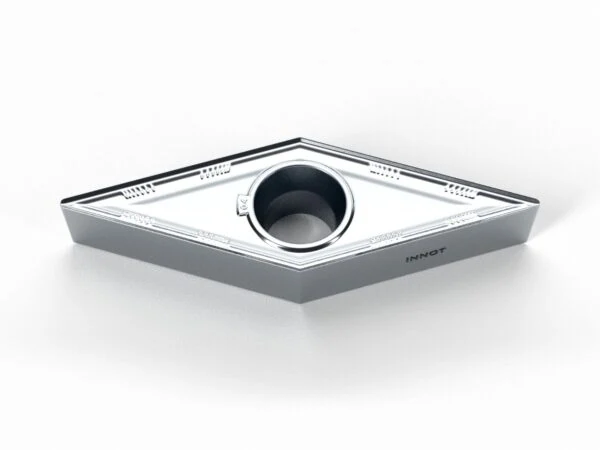
VBGT-AK
Available
NAluminiumFinishing
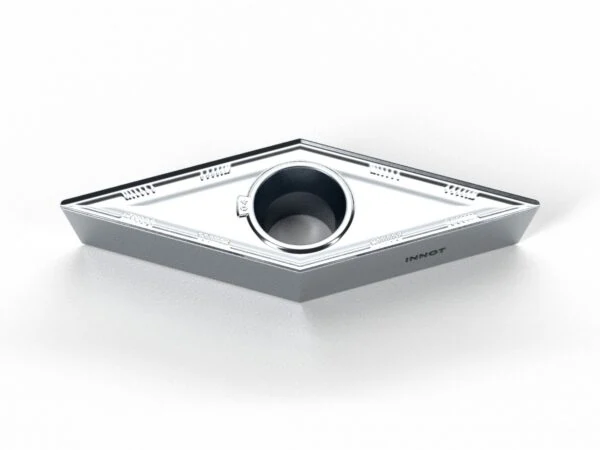
VCGT-AK
Available
NAluminiumFinishing
QPEB-AK
Available
NAluminiumSpecial
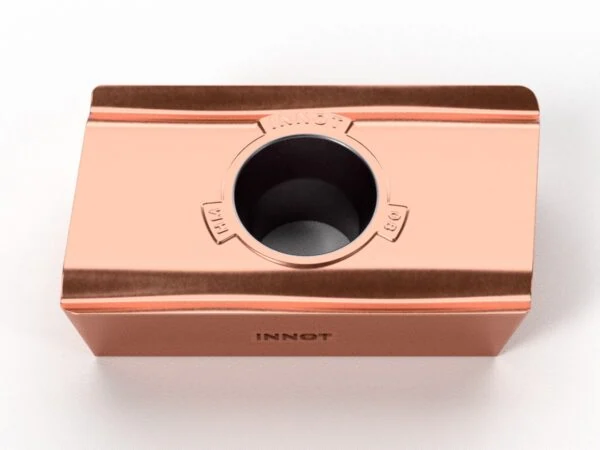
APMT-HM / APGT-AK
Available
HHardenedPSteelNAluminiumKCast ironMStainlessSSuperalloysSemi-finishing
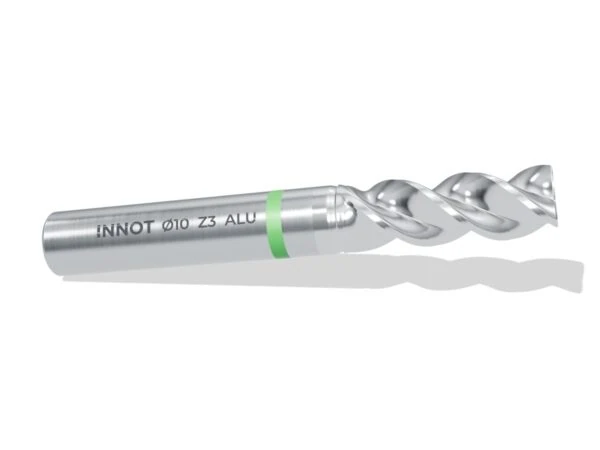
2- and 3-flute end mill for aluminium
Available
NAluminiumFinishing · Roughing
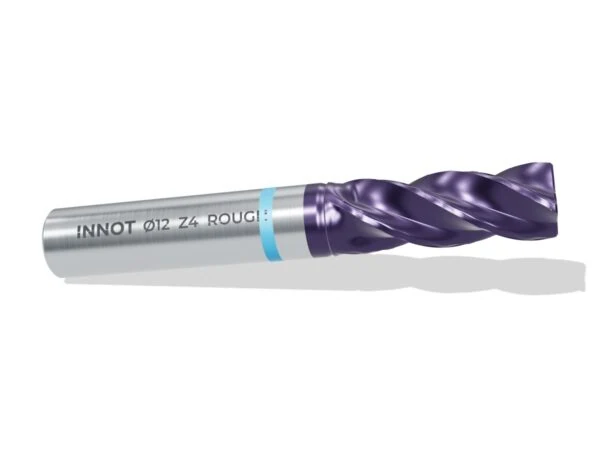
Roughing end mill with wavy cutting edge
Available
PSteelNAluminiumKCast ironRoughing
HHardenedPSteelNAluminiumKCast ironMStainlessFinishing · Semi-finishing
HHardenedPSteelNAluminiumKCast ironMStainlessFinishing · Semi-finishing
HHardenedPSteelNAluminiumKCast ironMStainlessFinishing · Semi-finishing
HHardenedPSteelNAluminiumKCast ironMStainlessFinishing · Semi-finishing
3×D solid carbide drill
Available
PSteelNAluminiumKCast ironMStainlessSSuperalloys
5×D solid carbide drill
Available
PSteelNAluminiumKCast ironMStainlessSSuperalloys
8×D solid carbide drill
Available
PSteelNAluminiumKCast ironMStainlessSSuperalloys
12×D solid carbide drill
Available
PSteelNAluminiumKCast ironMStainlessSSuperalloys
20×D solid carbide drill
Available
PSteelNAluminiumKCast ironMStainlessSSuperalloys
30×D solid carbide drill
Available
PSteelNAluminiumKCast ironMStainlessSSuperalloys
NAluminium
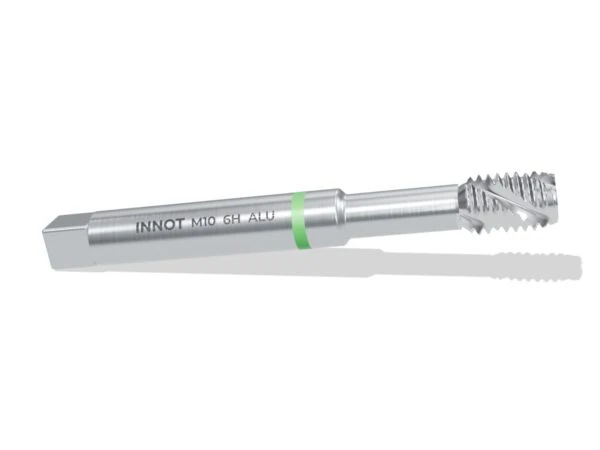
NAluminium
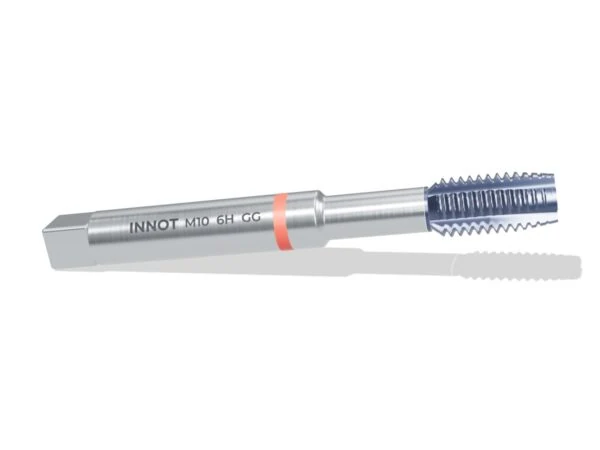
Cast iron tap – through and blind holes
Available
NAluminiumKCast iron
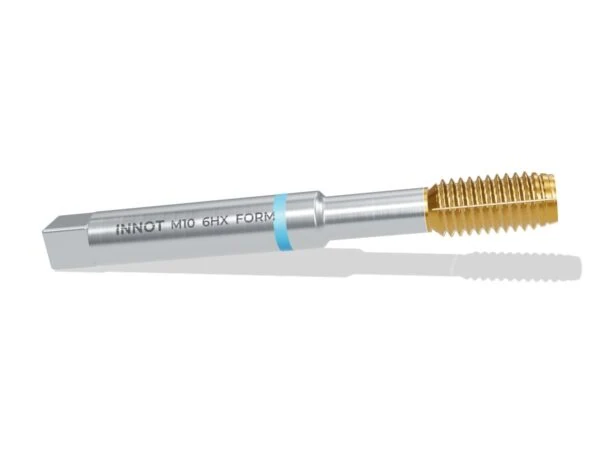
Forming tap – through and blind holes
Available
PSteelNAluminiumMStainless
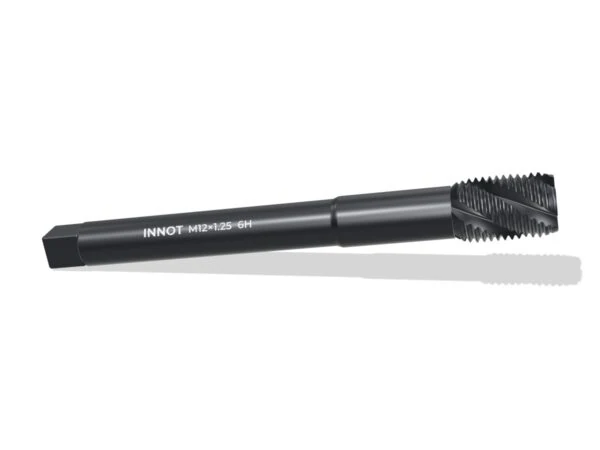
Taps for fine, pipe and inch threads
Available
PSteelNAluminiumKCast ironMStainless
Recently viewed
SPMT / APMT-MM
Available
HHardenedPSteelKCast ironMStainlessRoughing
SEKR / SEMR / SEEN
Available
HHardenedPSteelKCast ironMStainlessFace milling · Finishing
WNMG cast iron
Available
KCast ironSemi-finishing · Roughing
APKT-FM
Available
HHardenedPSteelKCast ironMStainlessSemi-finishing
TNMG-HQ
Available
PSteelFinishing · Semi-finishing






