
Turning Inserts
Negative inserts
Double-sided negative inserts: twice the cutting edges per insert and great strength. The choice for roughing and semi-finishing on medium and high-power lathes.
84inserts
Showing 1–24 of 84 results
Sort:
CNMA
Available
KCast ironRoughing
CNMG cast iron
Available
KCast ironSemi-finishing · Roughing
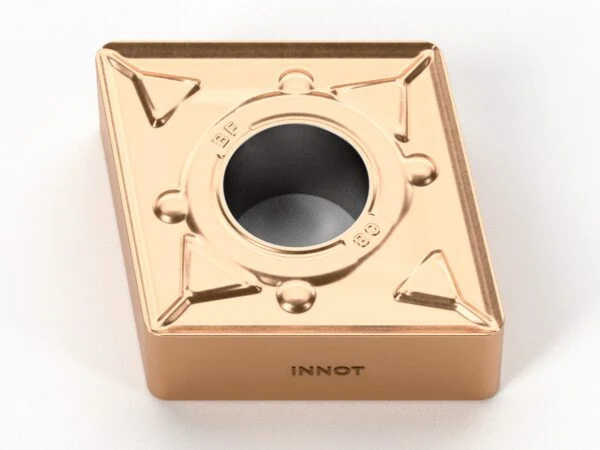
CNMG-BF
Available
MStainlessFinishing
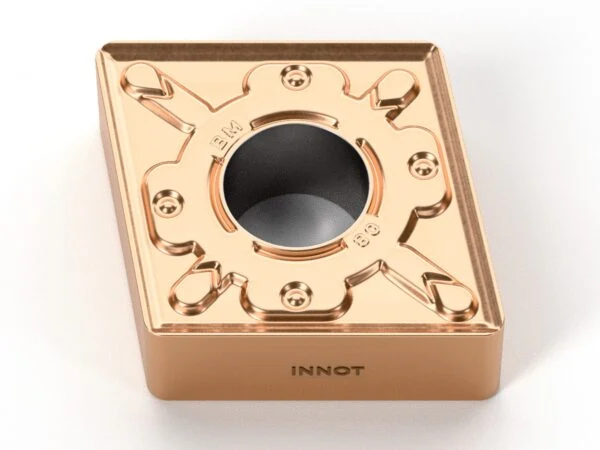
CNMG-BM
Available
MStainlessSemi-finishing
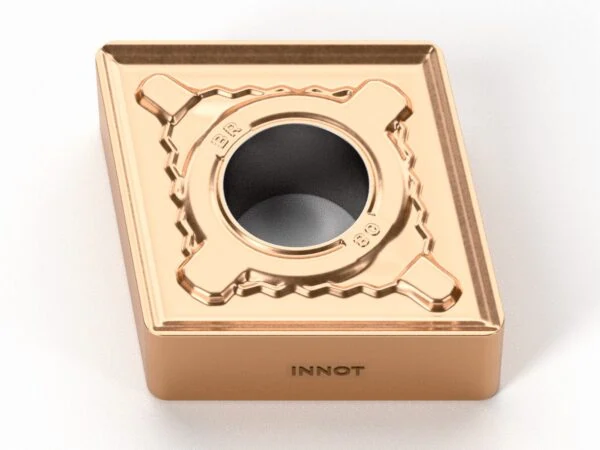
CNMG-BR
Available
MStainlessRoughing
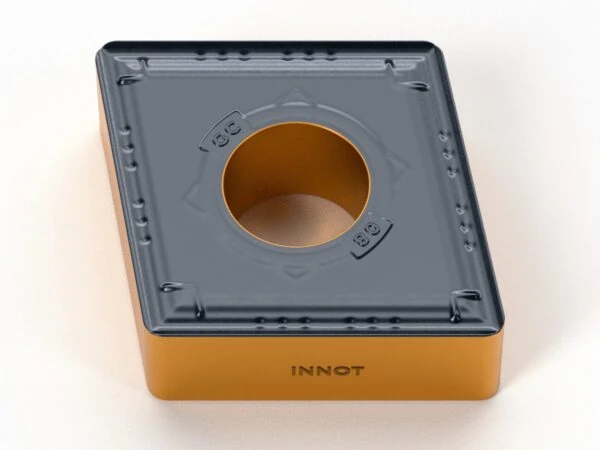
CNMG-GC
Available
PSteelFinishing
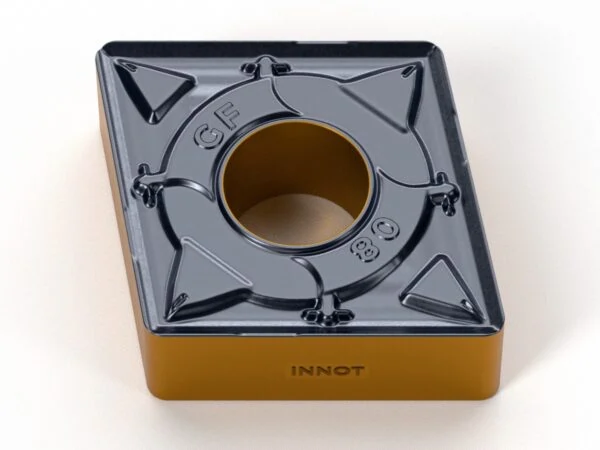
CNMG-GF
Available
PSteelFinishing
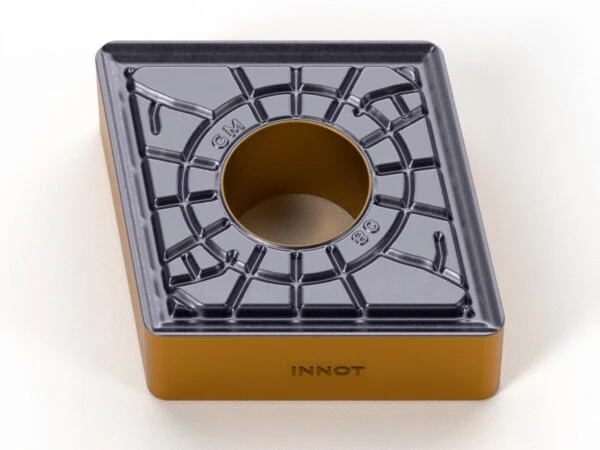
CNMG-GM
Available
PSteelSemi-finishing
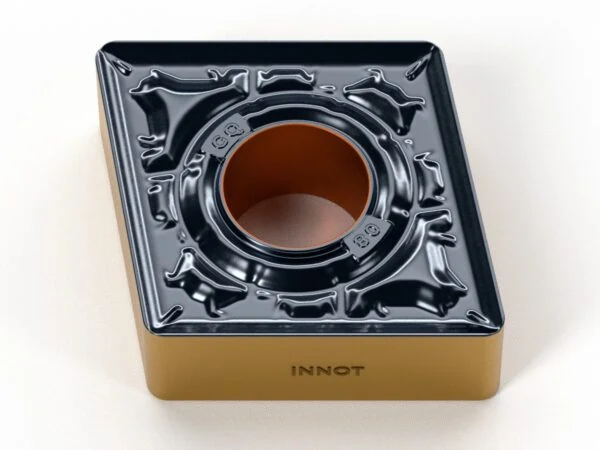
CNMG-GQ
Available
PSteelFinishing · Semi-finishing
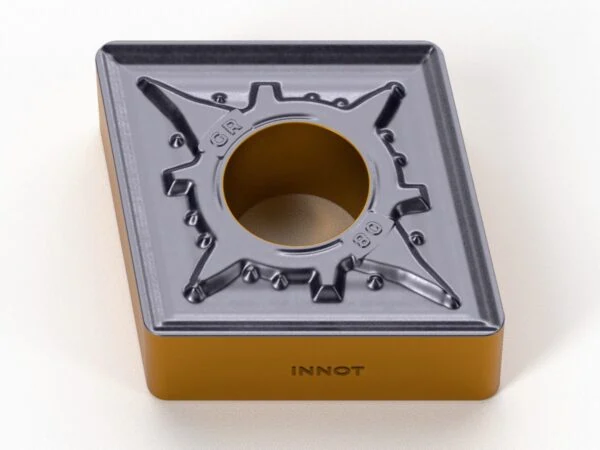
CNMG-GR
Available
PSteelRoughing
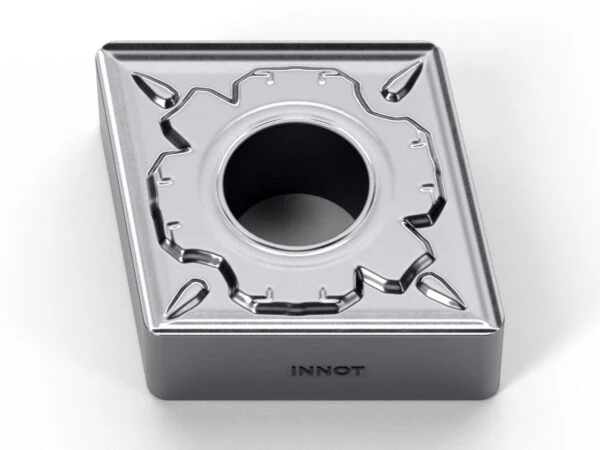
CNMG-HQ
Available
PSteelFinishing · Semi-finishing
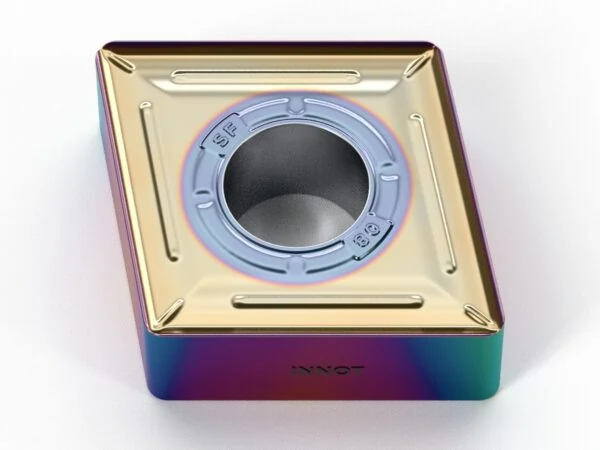
CNMG-SF
Available
SSuperalloysFinishing
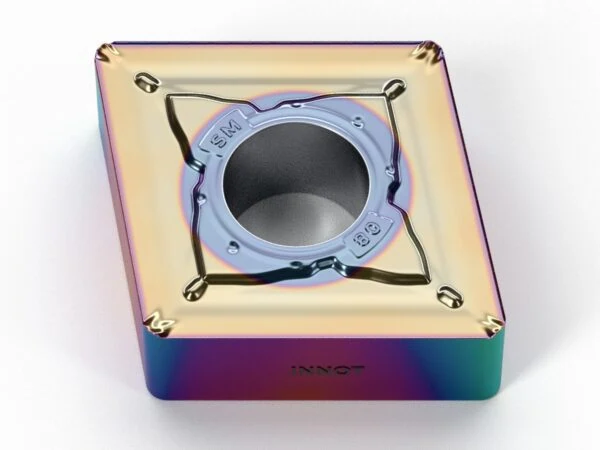
CNMG-SM
Available
SSuperalloysSemi-finishing · Roughing
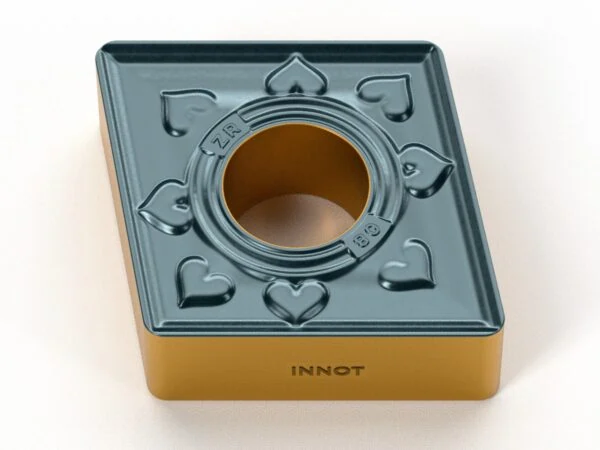
CNMG-ZR
Available
KCast ironFinishing · Semi-finishing · Roughing
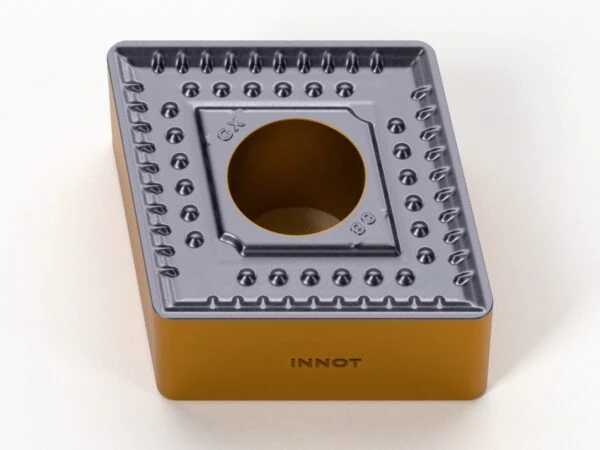
CNMM-GX
Available
PSteelHeavy-duty machining
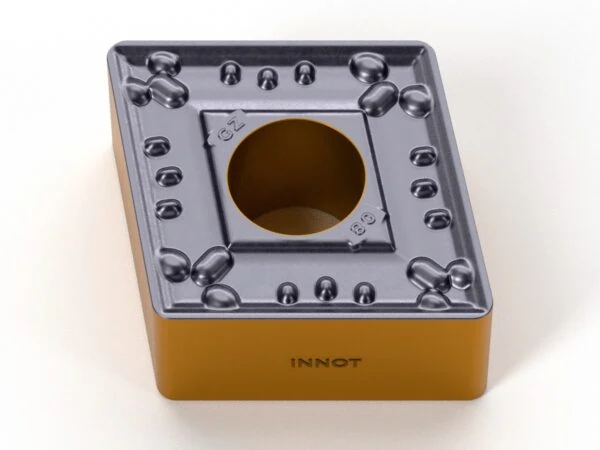
CNMM-GZ
Available
PSteelHeavy-duty machining
DNMA
Available
KCast ironRoughing
DNMG cast iron
Available
KCast ironSemi-finishing · Roughing
DNMG-BF
Available
MStainlessFinishing
DNMG-BM
Available
MStainlessSemi-finishing
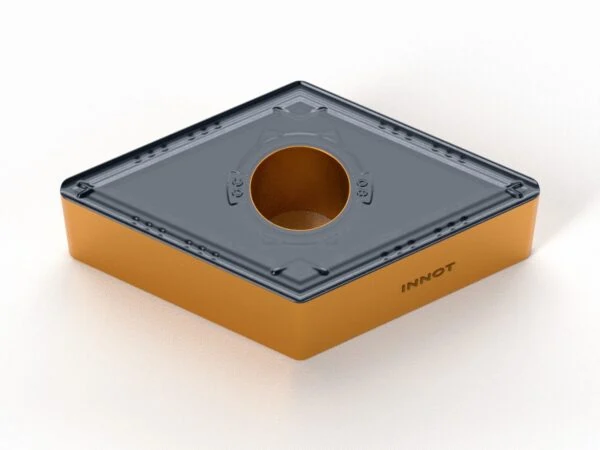
DNMG-GC
Available
PSteelFinishing
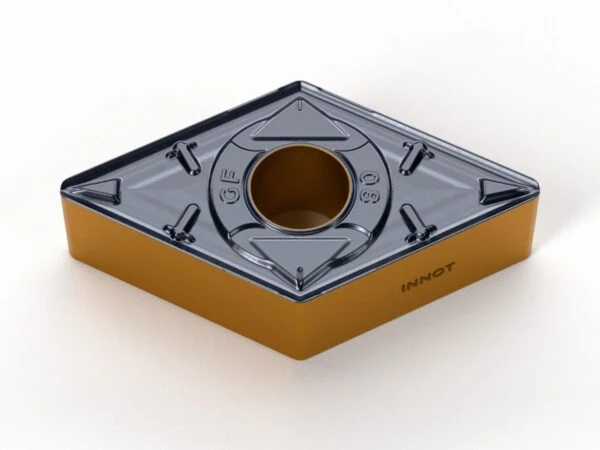
DNMG-GF
Available
PSteelFinishing
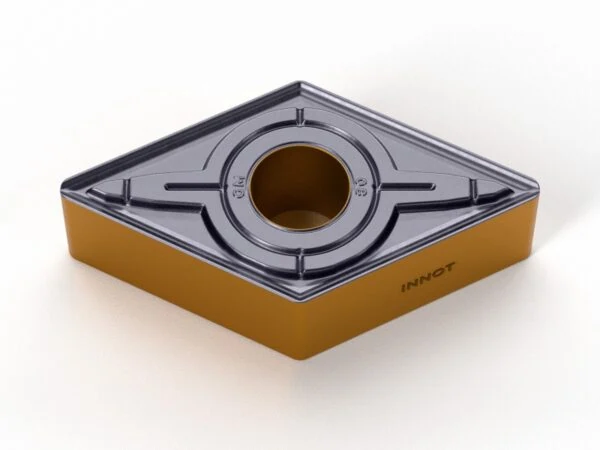
DNMG-GM
Available
PSteelSemi-finishing
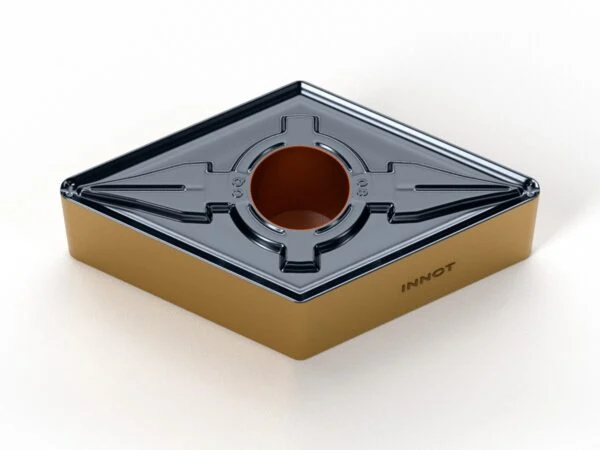
DNMG-GQ
Available
PSteelFinishing · Semi-finishing
INNOT guide
Negative turning inserts: strong and double-sided
Negative inserts have a 0° clearance and can be used on both sides: a CNMG offers 4 edges, a TNMG and a WNMG 6, an SNMG 8. The edge is strong and withstands high depths of cut and feeds, which makes them the first choice for roughing and general turning on stable lathes.
The shape depends on the profile to be turned: 80° (C and W) to turn and face with the same tool, 55° (D) and 35° (V) for profiling, 90° (S) and 60° (T) for roughing with the most edges.
Choose the familyCNMG / CNMA - 80° rhombicDNMG - 55° rhombicSNMG - 90° squareTNMG - 60° triangularVNMG - 35° rhombicWNMG - 80° trigon
Can't find the size or do you use another brand's code?Send us the code or the drawing: we reply with a quote within 30 minutes.
Recently viewed
45° and 75° toolholders for roughing
Available
PSteel
Roughing end mill with wavy cutting edge
Available
PSteelNAluminiumKCast ironRoughing
BLMP high-feed modular heads
Available






