
Turning Inserts
ISO carbide inserts for external and internal turning: double-sided negative inserts for heavy cuts, positive inserts for finishing and delicate parts. CVD, PVD and cermet grades for steel, stainless steel, cast iron and superalloys.
Showing 1–24 of 121 results
CNMA
CNMG cast iron
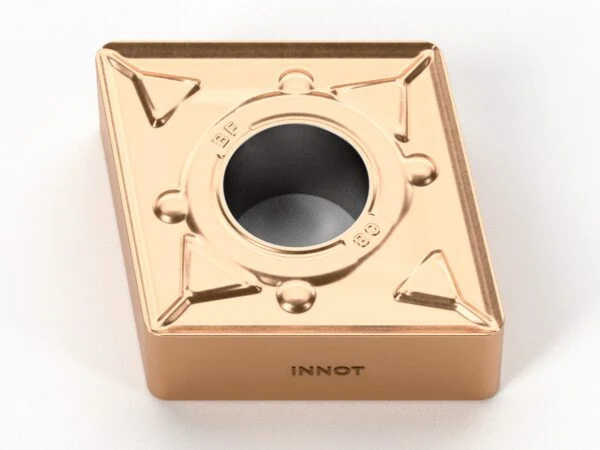
CNMG-BF
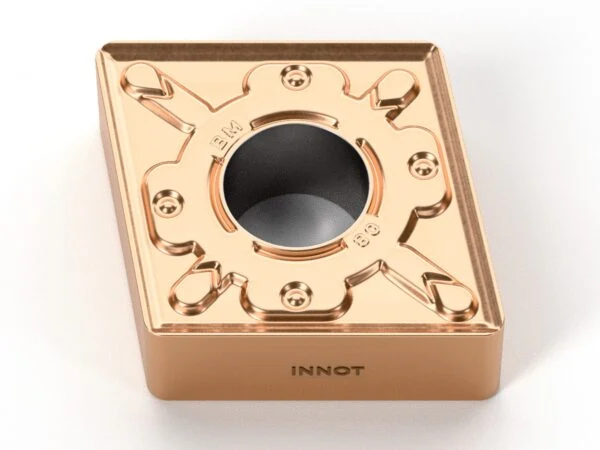
CNMG-BM
CNMG-BR
CNMG-GC
CNMG-GF
CNMG-GM
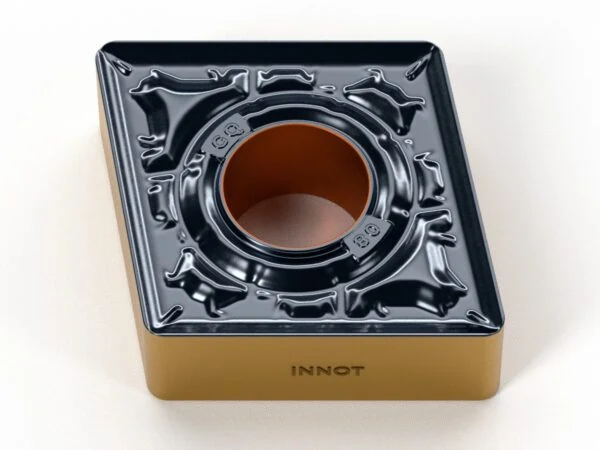
CNMG-GQ
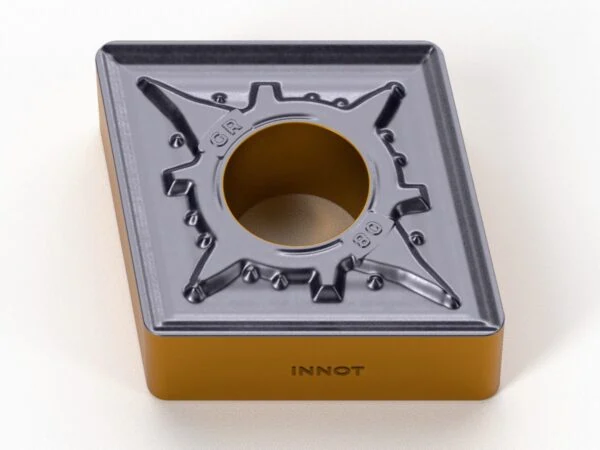
CNMG-GR
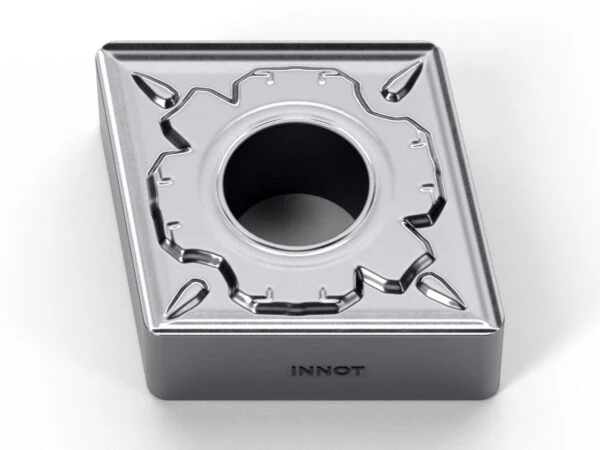
CNMG-HQ
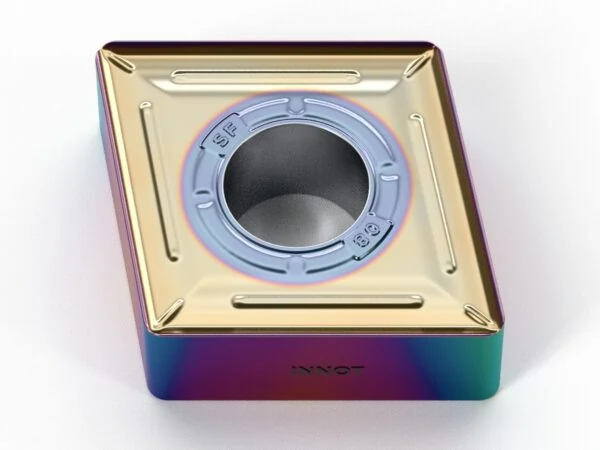
CNMG-SF
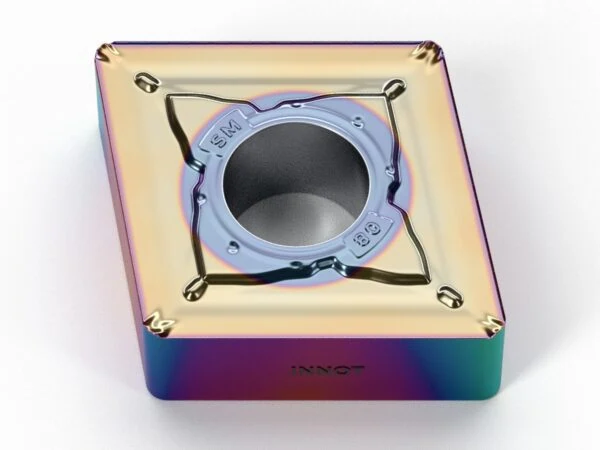
CNMG-SM
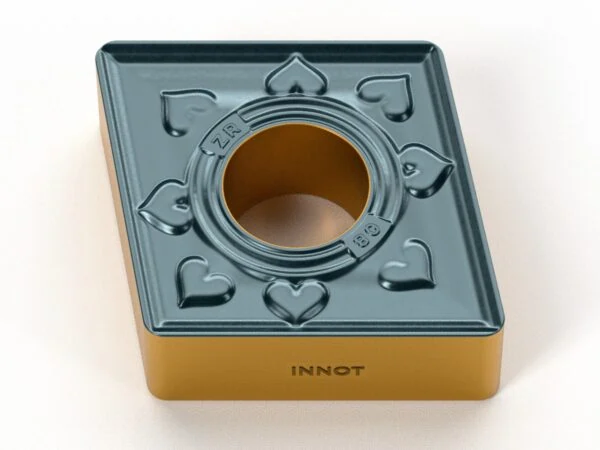
CNMG-ZR
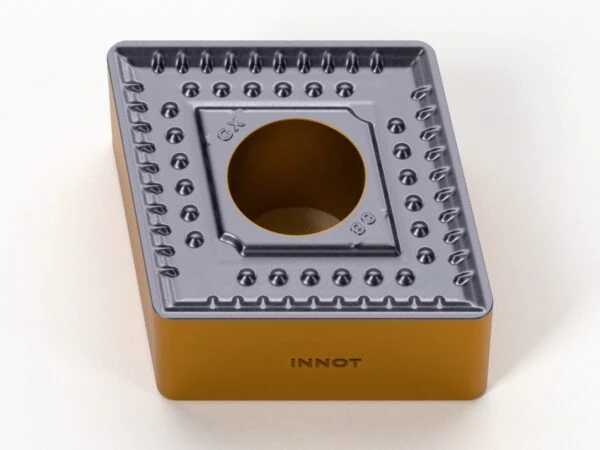
CNMM-GX
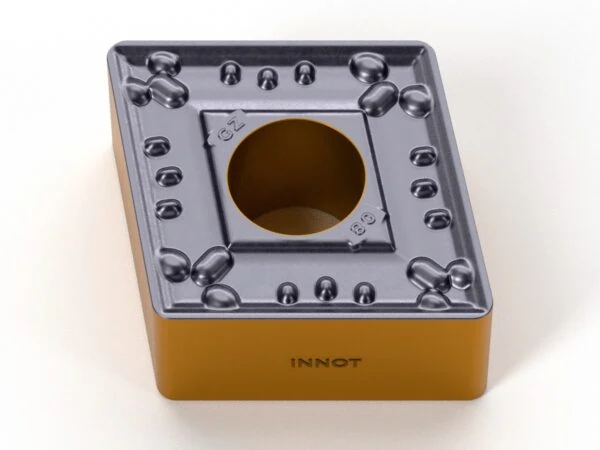
CNMM-GZ
DNMA
DNMG cast iron
DNMG-BF
DNMG-BM
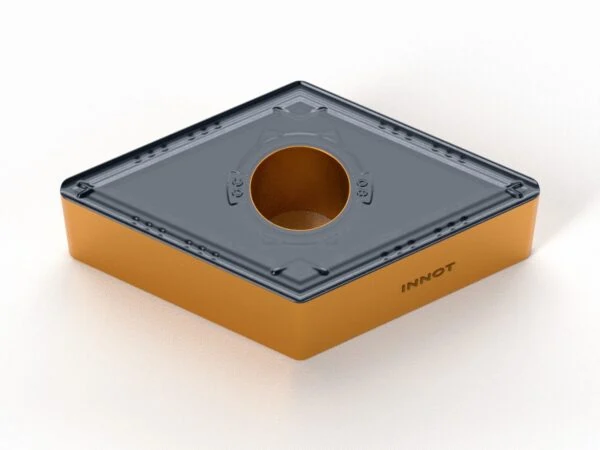
DNMG-GC
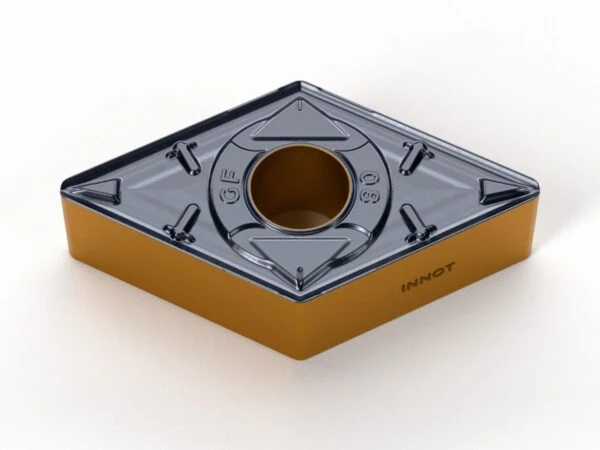
DNMG-GF
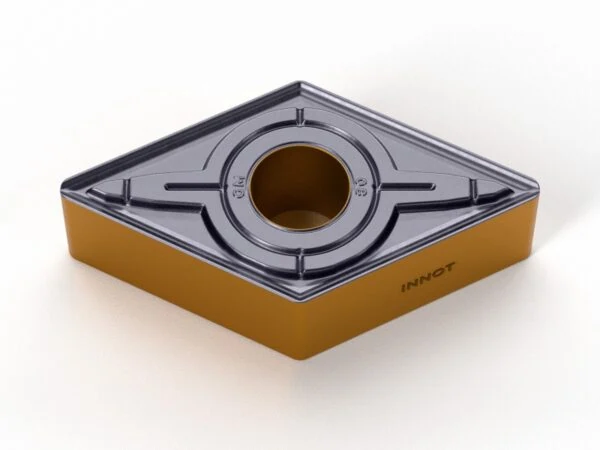
DNMG-GM
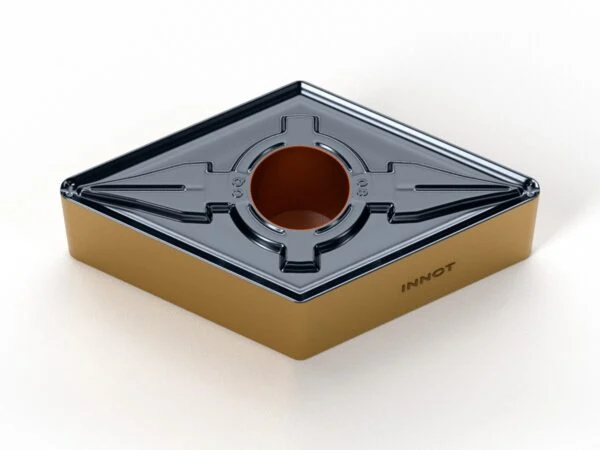
DNMG-GQ
Carbide turning inserts: how to choose the right one
INNOT turning inserts are ISO inserts in coated carbide and cermet for external and internal turning, profiling, parting and threading. Every product page lists sizes, nose radii, grades and recommended cutting data, so you can find the right insert for your material without trial and error.
Negative or positive?
Negative inserts (CNMG, DNMG, SNMG, TNMG, VNMG, WNMG) have a 0° clearance angle and are double-sided: they offer twice the cutting edges and a strong edge for roughing and heavy cuts. Positive inserts (CCMT, DCMT, SCMT, TCMT, VBMT, VCMT) have a 5° or 7° clearance: they cut with lower forces and are the right choice for finishing, small diameters, internal turning and thin-walled parts.
How to read the ISO code
In the code CNMG 120408, C is the shape (80° rhombic), N the clearance angle (0°), M the tolerance and G the insert type (hole and chipbreaker on both sides). Then come the cutting edge length (12), the thickness (04 = 4.76 mm) and the nose radius (08 = 0.8 mm).
Chipbreaker and grade
The chipbreaker decides how the chip forms and breaks: geometries for finishing (GF, GC, BF, SF), semi-finishing (GM, GQ, BM, SM) and roughing (GR, BR, GX, GZ). The carbide grade is chosen according to the ISO group of the material: P steel, M stainless steel, K cast iron, N aluminium, S superalloys and titanium, H hardened steel.
Frequently asked questions
Do INNOT inserts fit the toolholders I already use?
Yes. The inserts follow the ISO designation: an INNOT CNMG 120408 fits any toolholder for CNMG 12 inserts, whatever the brand.
Which nose radius should I choose?
Small radii (0.2–0.4 mm) for finishing and delicate parts, 0.8 mm as the universal choice, 1.2–1.6 mm for roughing and high feeds. A larger radius strengthens the edge but increases vibration.
Can I try an insert before ordering?
Yes, on request we send free test inserts so you can check tool life on your own job. Send us the code you use today and we will propose the INNOT equivalent.
Recently viewed
Custom step drill
NPT 60° threading inserts
95° external turning toolholders
BLMP (high feed)
Boring bars for internal turning






