Need help? Call us: (+39) 3757861361 or info@innot-it.com
Threading
Everything for the thread: carbide threading inserts for turning and taps for through and blind holes, chosen for the material. Metric, fine, pipe and inch, right- and left-hand, also custom made.
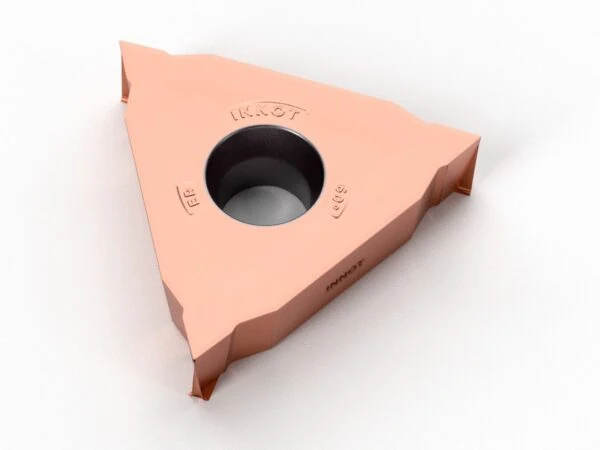
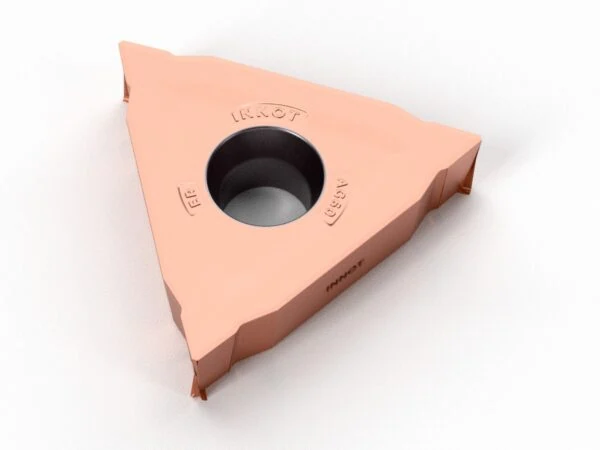
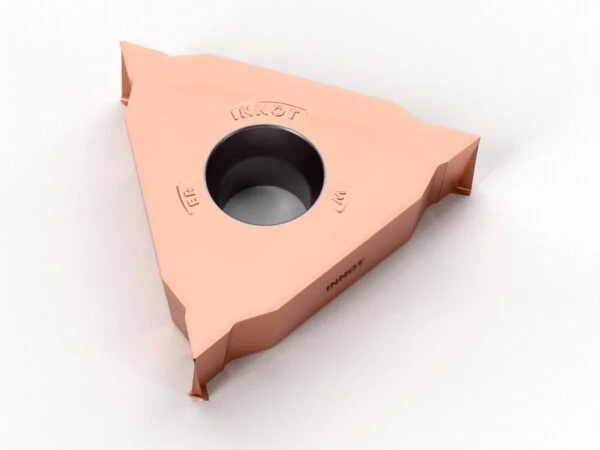
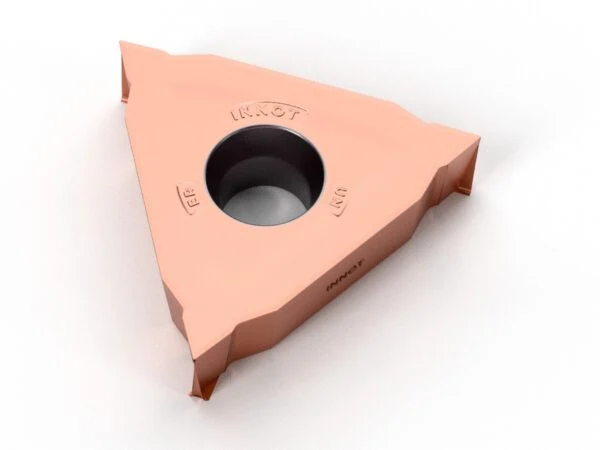
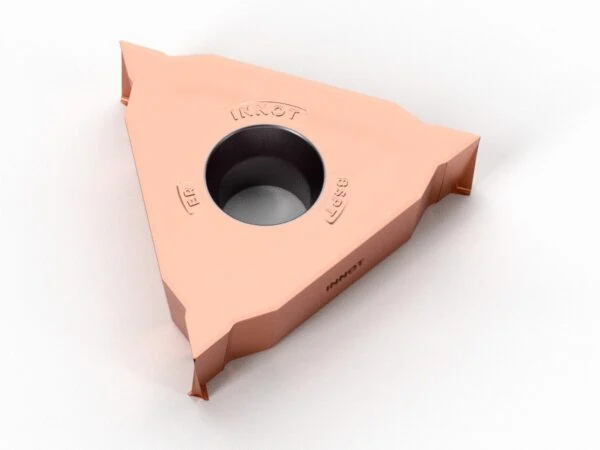
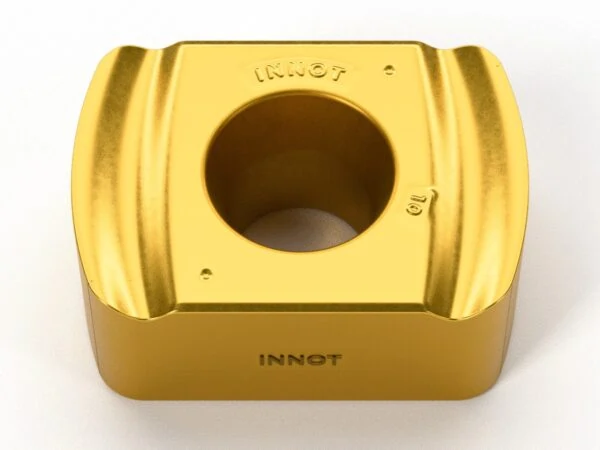
Full-profile inserts for ISO 60° metric threads: crest and root formed by the insert, finished thread without deburring.
Universal partial profile inserts: a single insert covers a range of pitches with a 55° or 60° angle. Ideal for small batches and different pitches.
Full-profile inserts for Whitworth 55° threads (BSW and BSF), with crest and root radius.
Full-profile inserts for UN 60° unified threads (UNC, UNF, UNEF), required in aerospace and hydraulics.
Inserts for BSPT (Rc / R) 55° pipe threads with 1:16 taper, for sealing fittings on gas, heating and water pipes.
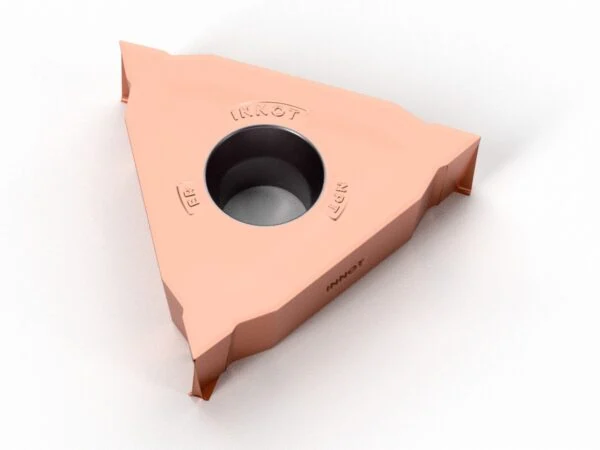
Inserts for NPT 60° taper threads with 1:16 taper, for pipes and sealing fittings to the American standard.
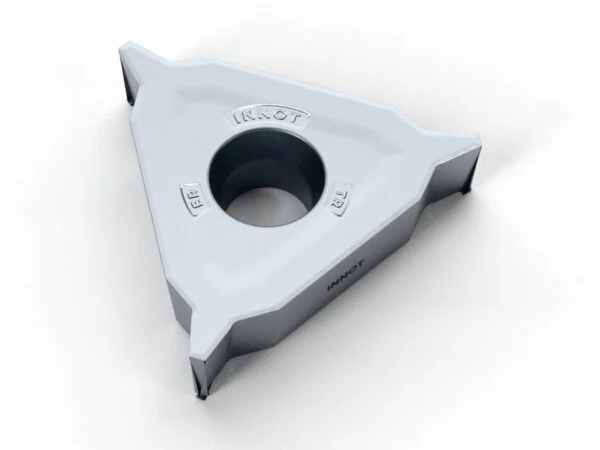
Inserts for ISO 30° trapezoidal threads (TR), used on lead screws, vices, presses and power transmissions.
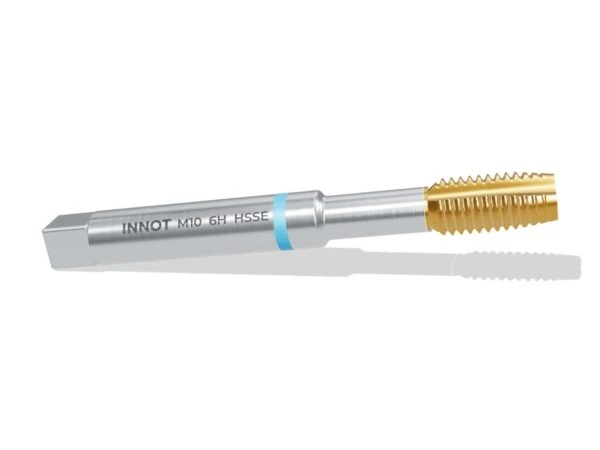
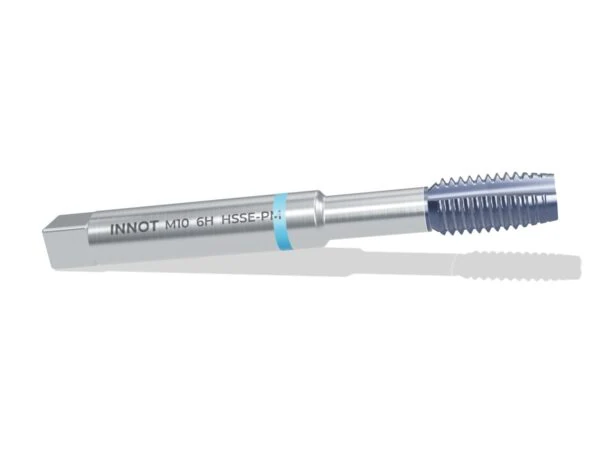
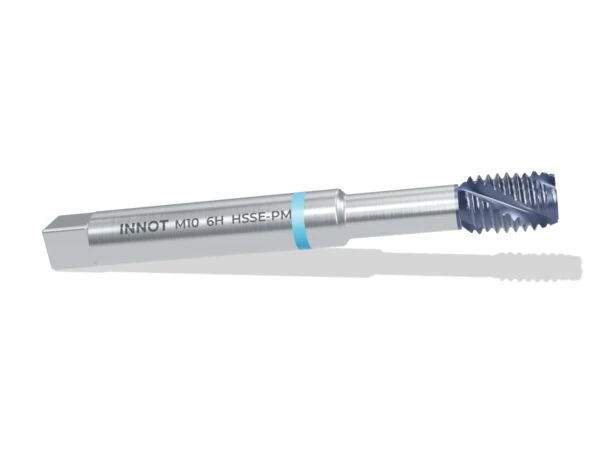
Spiral point tap for through holes in structural and annealed steels: the chip is pushed forward. TiN, 12 – 15° rake.
Spiral point tap for through holes in quenched and tempered and alloy steels: the chip is pushed forward. TiCN, 10 – 12° rake.
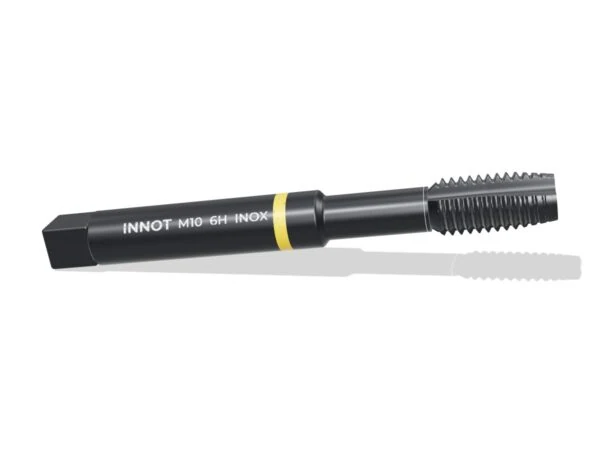
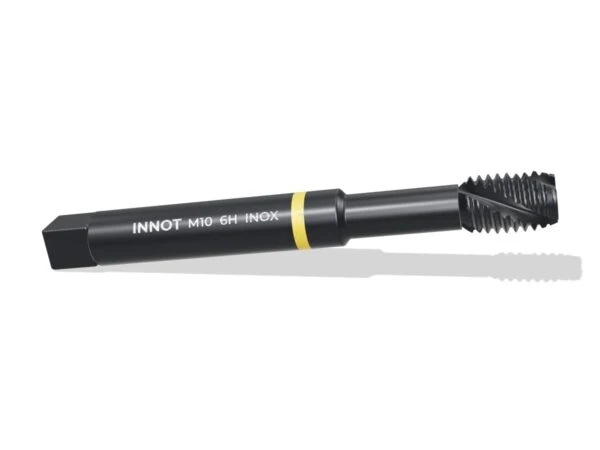
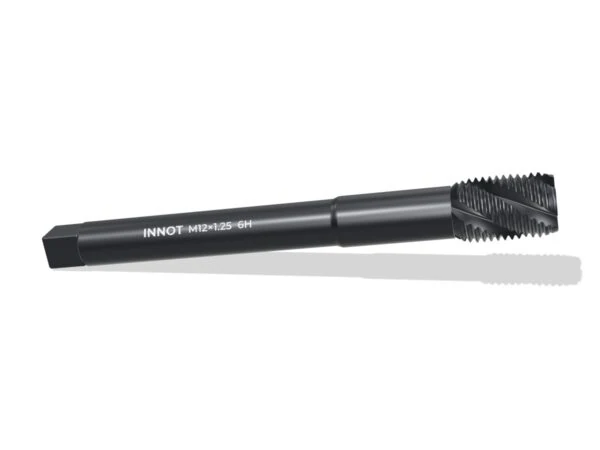
Spiral point tap for through holes in stainless steels: the chip is pushed forward. Steam oxide, 8 – 10° rake.
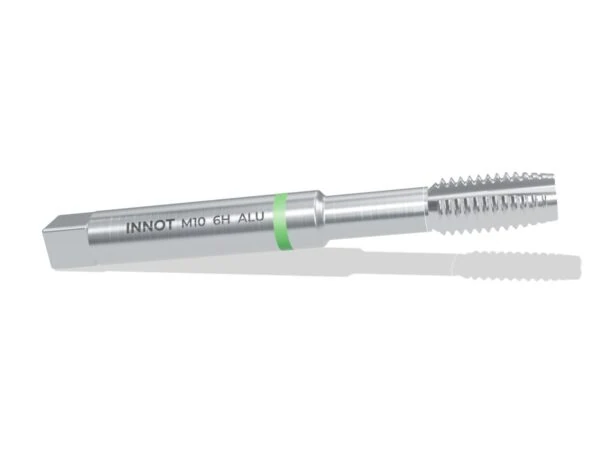
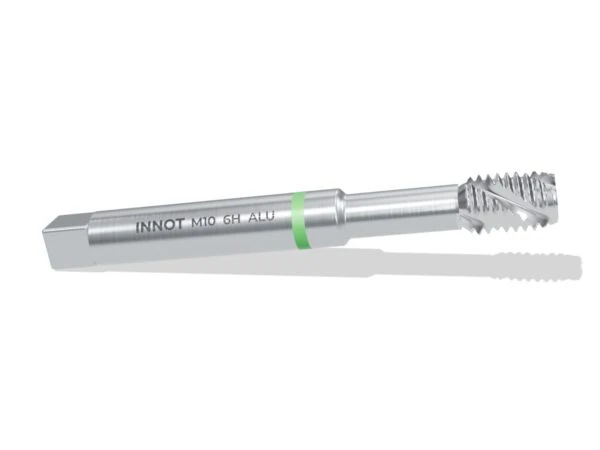
Spiral point tap for through holes in aluminium and light alloys: the chip is pushed forward. Bright, 20 – 25° rake.
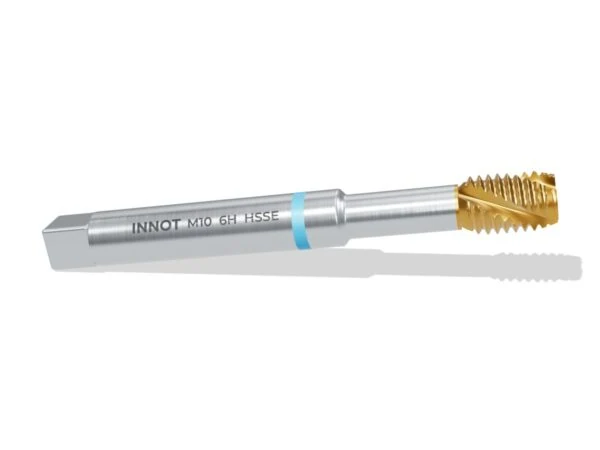
35° right-hand spiral flute tap for blind holes in structural and annealed steels: the chip flows back towards the shank. TiN, 12 – 15° rake.
40° right-hand spiral flute tap for blind holes in quenched and tempered and alloy steels: the chip flows back towards the shank. TiCN, 10 – 12° rake.
35° – 40° right-hand spiral flute tap for blind holes in stainless steels: the chip flows back towards the shank. Steam oxide, 8 – 10° rake.
45° right-hand spiral flute tap for blind holes in aluminium and light alloys: the chip flows back towards the shank. Bright, 20 – 25° rake.
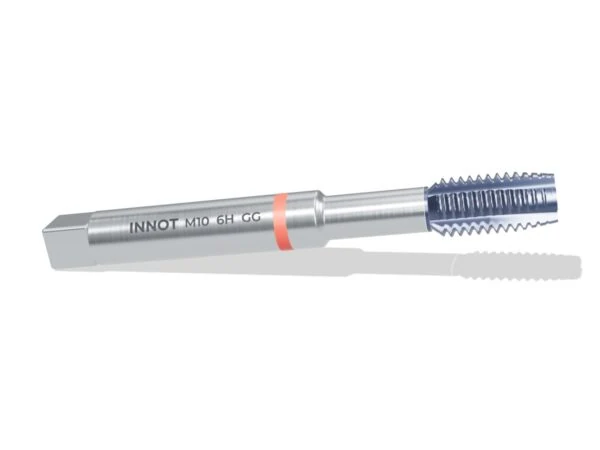
Straight flute tap for cast irons and short-chipping materials, in through and blind holes. Broken chips, TiCN against abrasion.
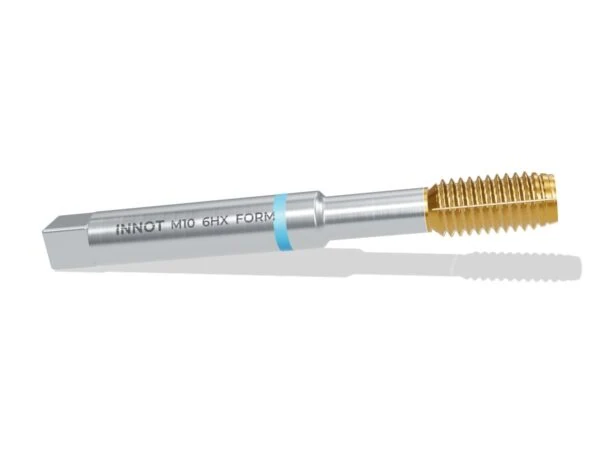
Fluteless tap that cold-forms the thread without chips: stronger and ideal for blind holes in steels, stainless steels and aluminium.
Metric fine, pipe G, Whitworth, UNC, UNF, UNEF, Pg and round, right- and left-hand: the same geometries for through and blind holes as the metric taps.
Custom tap
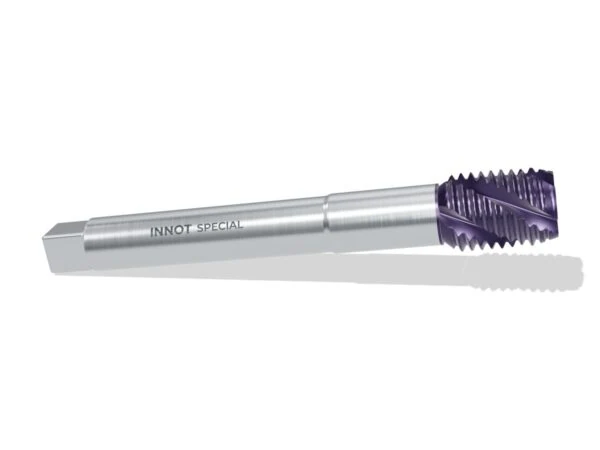
Taps made to drawing: profile, tolerance, lengths, coolant, HSS-E, PM or carbide substrate and coating chosen for your part.
Threading: taps and inserts for every thread
For thread turning INNOT offers partial-profile and full-profile inserts for ISO metric, Whitworth, UN, BSPT, NPT and trapezoidal threads. For threading holes there are taps for through holes, taps for blind holes and thread forming taps, in versions dedicated to steel, stainless steel, cast iron and aluminium.
Cutting tap or forming tap?
A cutting tap removes chips and works in almost every material. A forming tap shapes the thread by deformation, without chips: the thread is stronger and the tap lasts longer, but it needs a ductile material and a larger pre-drilled hole.
Partial or full profile?
A partial-profile insert covers a range of pitches with a single insert and is handy for small batches. A full-profile insert also forms the thread crest: it gives an exact profile and needs fewer passes.
Frequently asked questions
Do you make taps for special threads?
Yes: metric fine, BSP (G), Whitworth, UNC, UNF, UNEF, Pg and taps built to drawing with custom profile, tolerance and lengths.
Categories
- Turning Inserts (121)
- Negative inserts (84)
- CNMG / CNMA - 80° rhombic (16)
- DNMG - 55° rhombic (13)
- SNMG - 90° square (15)
- TNMG - 60° triangular (14)
- VNMG - 35° rhombic (12)
- WNMG - 80° trigon (14)
- Positive inserts (23)
- CCMT - 80° rhombic (4)
- DCMT - 55° rhombic (4)
- SCMT - 90° square (2)
- TCMT - 60° triangular (4)
- VBMT / VCMT - 35° rhombic (7)
- RCMX - Round (2)
- Parting and grooving (7)
- Negative inserts (84)
- Milling Inserts (24)
- Face milling (8)
- 90° square shoulder (5)
- High feed (3)
- Copy milling and profiling (7)
- Helical cutters (1)
- Solid Carbide End Mills (14)
- Drills (9)
- Solid carbide drills (7)
- Indexable drills (2)
- Threading (19)
- Threading inserts (7)
- Taps (12)
- Through hole taps (5)
- Blind hole taps (5)
- Forming taps (1)
- Special and custom threads (2)
- Toolholders and Chucks (15)
Recently viewed
BLMP (high feed)

Double-sided insert for high-feed cutters: from BLMP 04 to 13, up to 2 mm/tooth, for steels, stainless steels, superalloys and hardened steels up to 65 HRC.

Inserts and cutting tools for CNC machine shops. Dedicated grades for every ISO group, from steel to aluminium, from superalloys to hardened steels, with cutting data in every product sheet.
INNOT by Giammarco Turati
Via San Ponso, 57 – 10080 Pertusio (TO)
VAT No. IT13269100015
© 2026 INNOT by Giammarco Turati – VAT No. IT13269100015 – Pertusio (TO), Italy – Privacy Policy – Cookie Policy