
Turning cast iron: inserts and cutting data for grey and nodular iron
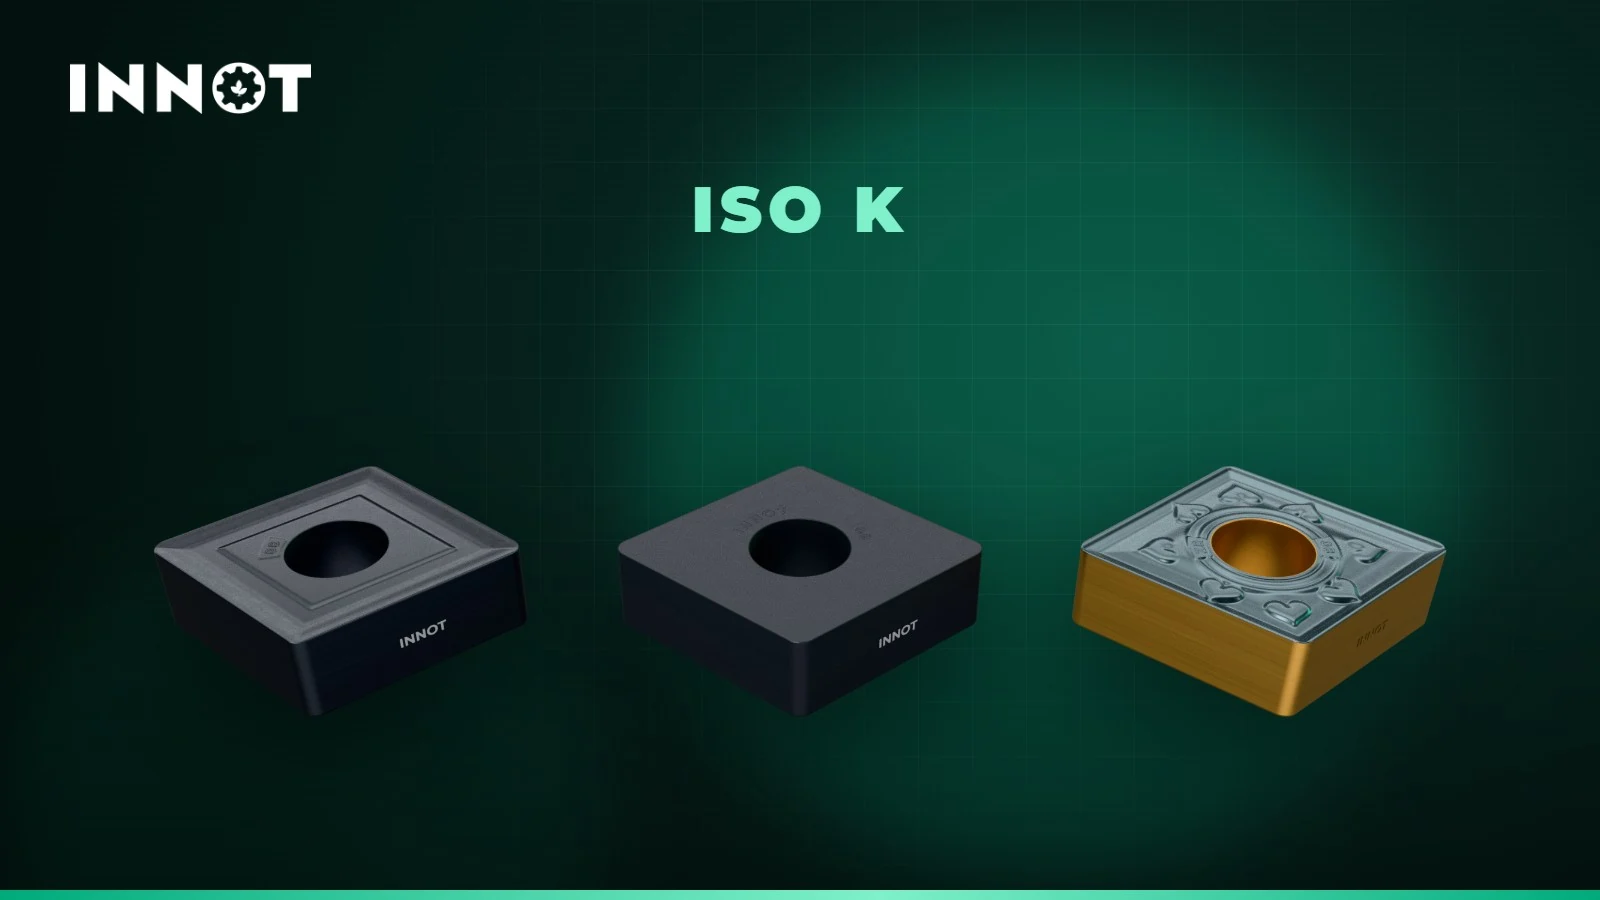
Cast iron is an ISO K material and behaves differently from steel. Grey cast iron (EN-GJL) contains flake graphite: it gives short, broken chips but is very abrasive and wears the insert flank. Nodular cast iron (EN-GJS) has graphite in nodules: it is tougher, gives longer chips and heats the cutting edge more.
This is why grades with a thick CVD coating that resists abrasion are needed: INNOT grades for cast iron have layers of TiN, TiCN and aluminium oxide (Al₂O₃).
Which insert to choose
| Insert | Grade | Cast iron | When to choose it |
|---|---|---|---|
| CNMG cast iron | IT6115 | Grey | Universal double-sided chipbreaker, from medium machining to roughing |
| Flat CNMA | IT6115 | Grey | No chipbreaker: the safest choice in unstable and interrupted cuts |
| CNMG-ZR | IT6215 | Nodular (also grey) | Sharp yet strong edge, low cutting forces, excellent in interrupted cuts |
Starting values
| Insert | Material | Vc (m/min) | fn (mm/rev) | ap (mm) |
|---|---|---|---|---|
| CNMG cast iron IT6115 | EN-GJL-200 / 300 (GG20, GG30) | 165–300 | 0.25–0.60 | 1.60–5.00 |
| CNMA IT6115 | EN-GJL-200 / 300 (GG20, GG30) | 155–285 | 0.20–0.60 | 2.50–6.00 |
| CNMG-ZR IT6215 | EN-GJS-400 / 500 (GGG40, GGG50) | 145–285 | 0.15–0.50 | 0.50–5.00 |
Indicative values in external turning, stable conditions. In difficult conditions reduce the maximum feed (down to 0.50 mm/rev with CNMG for cast iron and CNMA). All data by cutting condition are in the product pages.
Five tips from the shop floor
- Casting skin: the first pass must go below the skin. A depth of cut that just grazes the skin causes notch wear; better a deeper pass or varying the depth from one pass to the next.
- Coolant: grey cast iron is often machined dry. If you use coolant, it must be plentiful and continuous: intermittent jets cause thermal cracks.
- Flank wear: it is the normal wear on cast iron. If it grows too fast, reduce the cutting speed by 10–20%.
- Part edges: cast iron chips easily where the tool exits the cut; reduce the feed over the last few millimetres or add a chamfer.
- Interrupted cuts: prefer the flat CNMA insert or the ZR chipbreaker, with a nose radius of at least 0.8 mm.
Frequently asked questions
Can I use steel inserts on cast iron?
They work, but they last less: ISO K grades have a coating that better resists the abrasion of graphite. On nodular iron, which is closer to steel, the difference is smaller.
Are the same geometries available in other shapes?
Yes: INNOT cast iron inserts also come in D, S, T, V and W shapes for the most common toolholders. Find them in the negative inserts catalogue or request a quote.






