
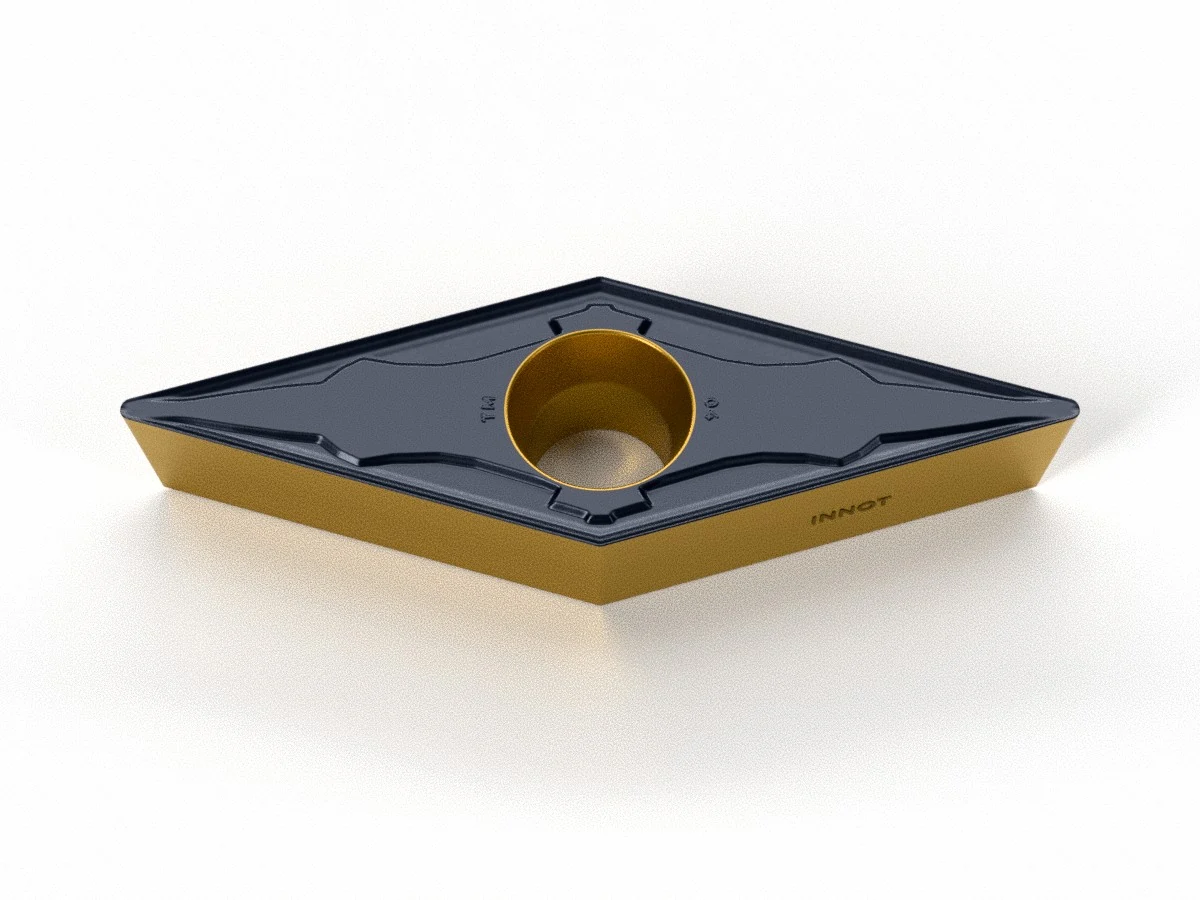
VCMT-TM
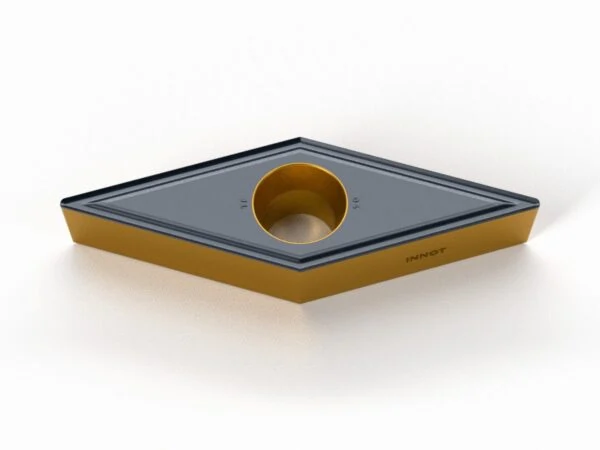
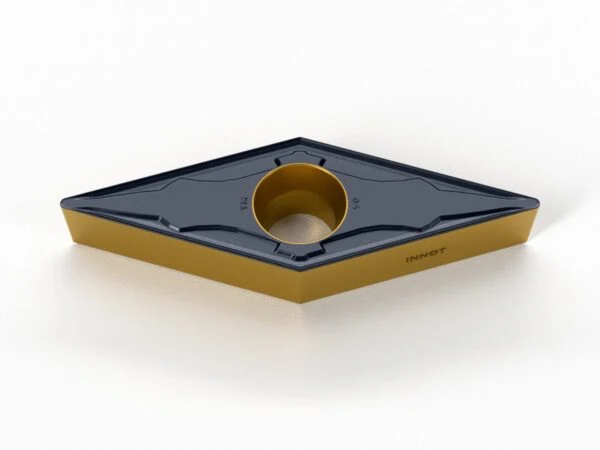
35° positive rhombic insert (VCMT) for semi-finishing of steels and stainless steels, external and boring, with TM chipbreaker and INNOT CVD and PVD grades.
Semi-finishing
CVD · PVD
★ IT8115 · IT8225 · IT7225
Technical data sheet PDFCutting data, sizes and grades
Want to try it first? Request a free tester

Description
ISO specifications
| ISO | RADIUS (RE) | AVAILABLE GRADES | CHIPBREAKER |
|---|---|---|---|
| VCMT1103 | 0.4 – 0.8 | IT8115 – IT8125 – IT8225 – IT7125 – IT7225 | TM |
| VCMT1604 | 0.4 – 0.8 – 1.2 | IT8115 – IT8125 – IT8225 – IT7125 – IT7225 | TM |
TM chipbreaker data sheet
| Operation | Semi-finishing |
| ISO material | P (steels), M (stainless steels) |
| Tolerance | M |
| Features | Chipbreaker for semi-finishing, suitable for external and internal turning of steels and stainless steels. 7° positive insert (shape V, 35° rhombic) with screw clamping: the slimmest tip in the range, for copy turning and profiling of grooves and radii. SVQC (107.5°) and SVUC (93°) type toolholders. |
Available INNOT grades
| Grade | ISO | Coating | Composition | Application |
|---|---|---|---|---|
| IT8115 ★ | P | CVD | TiN + MT-TiCN + Al₂O₃ | Continuous and lightly interrupted cuts. Finishing and semi-finishing of carbon and alloy steels. |
| IT8125 | P | CVD | TiN + MT-TiCN + Al₂O₃ | Interrupted and continuous cuts on steel. The reinforced substrate limits plastic deformation at high temperature. |
| IT8225 ★ | P | CVD | TiN + MT-TiCN + Al₂O₃ | First-choice grade for steel, very versatile. Multilayer coating with excellent wear resistance and toughness. |
| IT7125 | M | PVD | AlTiN | Universal grade for turning stainless steel in continuous and interrupted cuts. Smooth, low-friction coating, high nano-hardness and excellent oxidation resistance. |
| IT7225 ★ | M | PVD | AlTiSiN + TiSiN | First-choice grade for turning stainless steel. Nano-gradient coating on a sub-micron grain substrate: excellent wear resistance and toughness. |
★ Recommended grade for this chipbreaker. CVD and PVD = vapour deposition coatings (chemical and physical). ISO P = steels, ISO M = stainless steels.
Recommended cutting data
External turning of steels (ISO P) – TM chipbreaker
| Material | Condition | Vc (m/min) by grade | fn (mm/rev) | ap (mm) |
|---|---|---|---|---|
| Structural steels ≤ 180 HB (S235, C45…) |
Stable | IT8115: 215 – 415 IT8125: 190 – 355 IT8225: 205 – 375 |
0.15 – 0.35 | 0.50 – 3.00 |
| Structural steels ≤ 180 HB (S235, C45…) |
Average | IT8115: 200 – 405 IT8125: 185 – 350 IT8225: 195 – 360 |
0.15 – 0.30 | 0.50 – 3.00 |
| Structural steels ≤ 180 HB (S235, C45…) |
Difficult | IT8125: 185 – 350 IT8225: 195 – 360 |
0.15 – 0.25 | 0.50 – 3.00 |
| Carbon and alloy steels 180 – 280 HB (41Cr4, 42CrMo4…) |
Stable | IT8115: 215 – 415 IT8125: 190 – 355 IT8225: 205 – 375 |
0.15 – 0.35 | 0.50 – 3.00 |
| Carbon and alloy steels 180 – 280 HB (41Cr4, 42CrMo4…) |
Average | IT8115: 200 – 405 IT8125: 185 – 350 IT8225: 195 – 360 |
0.15 – 0.30 | 0.50 – 3.00 |
| Carbon and alloy steels 180 – 280 HB (41Cr4, 42CrMo4…) |
Difficult | IT8125: 185 – 350 IT8225: 195 – 360 |
0.15 – 0.25 | 0.50 – 3.00 |
| Quenched and tempered steels ≥ 280 HB | Stable | IT8115: 215 – 420 IT8225: 190 – 395 |
0.15 – 0.35 | 0.50 – 3.00 |
| Quenched and tempered steels ≥ 280 HB | Average | IT8115: 215 – 420 IT8225: 190 – 395 |
0.15 – 0.30 | 0.50 – 3.00 |
Guide values for the TM chipbreaker (positive inserts), given only for the grades available in this product.
External turning of stainless steel (ISO M) – TM chipbreaker
| Material | Condition | Vc (m/min) by grade | fn (mm/rev) | ap (mm) |
|---|---|---|---|---|
| Austenitic stainless steel ≤ 200 HB (AISI 304, 316…) |
Stable | IT7125: 80 – 150 IT7225: 80 – 150 |
0.15 – 0.35 | 0.50 – 3.00 |
| Austenitic stainless steel ≤ 200 HB (AISI 304, 316…) |
Average | IT7125: 80 – 150 IT7225: 80 – 150 |
0.15 – 0.30 | 0.50 – 3.00 |
| Austenitic stainless steel ≤ 200 HB (AISI 304, 316…) |
Difficult | IT7125: 80 – 150 IT7225: 80 – 150 |
0.15 – 0.25 | 0.50 – 3.00 |
| Martensitic stainless steel > 200 HB (AISI 431, 420…) |
Stable | IT7125: 70 – 140 IT7225: 70 – 140 |
0.15 – 0.35 | 0.50 – 3.00 |
| Martensitic stainless steel > 200 HB (AISI 431, 420…) |
Average | IT7125: 70 – 140 IT7225: 70 – 140 |
0.15 – 0.30 | 0.50 – 3.00 |
| Martensitic stainless steel > 200 HB (AISI 431, 420…) |
Difficult | IT7125: 70 – 140 IT7225: 70 – 140 |
0.15 – 0.25 | 0.50 – 3.00 |
Guide values for the TM chipbreaker (positive inserts), given only for the grades available in this product.
Internal turning / boring (ISO P)
| Material | Operation | Cut | RE | Vc (m/min) min – recomm. – max |
ap (mm) min – recomm. – max |
fn (mm/rev) min – recomm. – max |
|---|---|---|---|---|---|---|
| Low carbon / low alloy ≤ 300 HB |
Precision finishing | Continuous | 0.4 | 250 – 300 – 350 | 0.05 – 0.3 – 0.5 | 0.03 – 0.1 – 0.15 |
| Interrupted | 120 – 170 – 220 | 0.05 – 0.3 – 0.5 | 0.03 – 0.1 – 0.15 | |||
| Finishing | Continuous | 0.4 – 0.8 | 200 – 250 – 300 | 0.2 – 0.5 – 1.0 | 0.05 – 0.1 – 0.2 | |
| Interrupted | 150 – 200 – 250 | 0.2 – 0.5 – 1.0 | 0.05 – 0.1 – 0.2 | |||
| Finishing – semi-roughing | Continuous | 0.4 – 0.8 | 150 – 200 – 250 | 0.5 – 1.0 – 2.0 | 0.1 – 0.15 – 0.25 | |
| Interrupted | 100 – 150 – 200 | 0.5 – 1.0 – 1.5 | 0.1 – 0.15 – 0.2 | |||
| Semi-roughing | Continuous | 0.4 – 0.8 | 100 – 150 – 200 | 1.0 – 1.5 – 2.5 | 0.1 – 0.15 – 0.3 | |
| Interrupted | 80 – 120 – 150 | 1.0 – 1.5 – 2.0 | 0.1 – 0.15 – 0.2 | |||
| Medium carbon / medium alloy ≤ 300 HB |
Precision finishing | Continuous | 0.4 | 150 – 200 – 250 | 0.05 – 0.3 – 0.5 | 0.03 – 0.1 – 0.15 |
| Interrupted | 120 – 140 – 170 | 0.05 – 0.3 – 0.5 | 0.03 – 0.1 – 0.15 | |||
| Finishing | Continuous | 0.4 – 0.8 | 150 – 200 – 250 | 0.2 – 0.5 – 1.0 | 0.05 – 0.1 – 0.2 | |
| Interrupted | 120 – 180 – 200 | 0.2 – 0.5 – 1.0 | 0.05 – 0.1 – 0.2 | |||
| Finishing – semi-roughing | Continuous | 0.4 – 0.8 | 120 – 180 – 220 | 0.5 – 1.0 – 2.0 | 0.1 – 0.15 – 0.25 | |
| Interrupted | 100 – 150 – 200 | 0.5 – 1.0 – 1.5 | 0.1 – 0.15 – 0.2 | |||
| Semi-roughing | Continuous | 0.4 – 0.8 | 100 – 150 – 200 | 1.0 – 1.5 – 2.5 | 0.1 – 0.15 – 0.3 | |
| Interrupted | 80 – 120 – 150 | 1.0 – 1.5 – 2.0 | 0.1 – 0.15 – 0.2 | |||
| High carbon / alloy ≤ 280 HB |
Precision finishing | Continuous | 0.4 | 120 – 150 – 180 | 0.05 – 0.3 – 0.5 | 0.03 – 0.1 – 0.15 |
| Interrupted | 110 – 130 – 160 | 0.05 – 0.3 – 0.5 | 0.03 – 0.1 – 0.15 | |||
| Finishing | Continuous | 0.4 – 0.8 | 120 – 150 – 180 | 0.2 – 0.5 – 1.0 | 0.05 – 0.1 – 0.2 | |
| Interrupted | 100 – 120 – 150 | 0.2 – 0.5 – 1.0 | 0.05 – 0.1 – 0.2 | |||
| Finishing – semi-roughing | Continuous | 0.4 – 0.8 | 120 – 150 – 180 | 0.5 – 1.0 – 2.0 | 0.1 – 0.15 – 0.25 | |
| Interrupted | 100 – 120 – 150 | 0.5 – 1.0 – 1.5 | 0.1 – 0.15 – 0.2 | |||
| Semi-roughing | Continuous | 0.4 – 0.8 | 100 – 120 – 150 | 1.0 – 1.5 – 2.5 | 0.1 – 0.15 – 0.3 | |
| Interrupted | 80 – 100 – 120 | 1.0 – 1.5 – 2.0 | 0.1 – 0.15 – 0.2 |
Recommended grades: IT8115 – IT8225. Minimum machining diameter: Ø10 mm. ap = radial depth of cut.
Internal turning / boring (ISO M)
| Material | Operation | Cut | RE | Vc (m/min) min – recomm. – max |
ap (mm) min – recomm. – max |
fn (mm/rev) min – recomm. – max |
|---|---|---|---|---|---|---|
| Austenitic stainless steel ≤ 220 HB |
Finishing | Continuous | 0.4 – 0.8 | 120 – 150 – 180 | 0.2 – 0.5 – 0.8 | 0.05 – 0.08 – 0.1 |
| Interrupted | 100 – 120 – 150 | 0.2 – 0.5 – 0.8 | 0.05 – 0.08 – 0.1 | |||
| Semi-finishing | Continuous | 0.4 – 0.8 | 120 – 150 – 180 | 0.5 – 1.0 – 1.5 | 0.05 – 0.1 – 0.2 | |
| Interrupted | 100 – 120 – 150 | 0.5 – 1.0 – 1.5 | 0.05 – 0.1 – 0.2 | |||
| Precipitation-hardening stainless steel ≤ 300 HB |
Finishing | Continuous | 0.4 – 0.8 | 80 – 100 – 120 | 0.2 – 0.7 – 1.0 | 0.05 – 0.1 – 0.15 |
| Interrupted | 60 – 80 – 100 | 0.2 – 0.7 – 1.0 | 0.05 – 0.1 – 0.15 | |||
| Semi-finishing | Continuous | 0.4 – 0.8 | 80 – 100 – 120 | 0.5 – 1.0 – 1.5 | 0.05 – 0.1 – 0.2 | |
| Interrupted | 60 – 80 – 100 | 0.5 – 1.0 – 1.5 | 0.05 – 0.1 – 0.2 |
Recommended grades: IT7125 – IT7225. Guide values for positive inserts, machining diameter over Ø10 mm. ap = radial depth of cut.
You may also like
Recently viewed
SNMG-BR
30×D solid carbide drill
Face mills
CCMT-HQ
QPMB-RM






