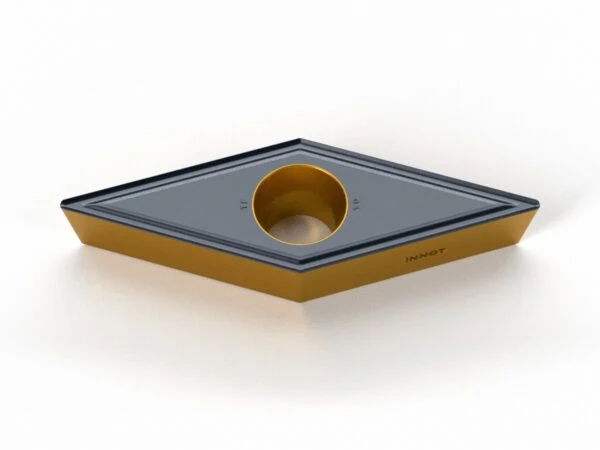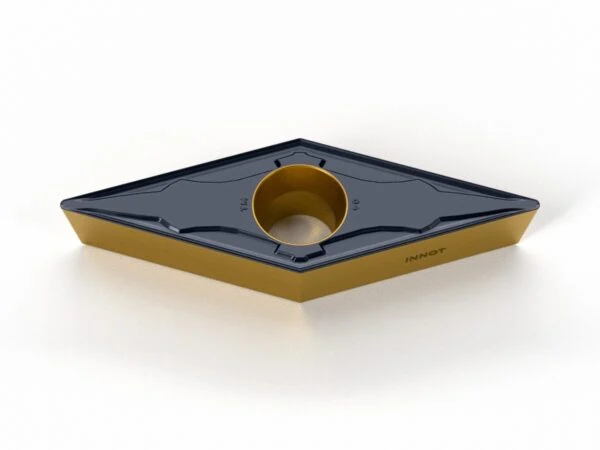
VCGT-AK
Ground 35° positive rhombic insert (VCGT) for turning aluminium, with AK chipbreaker and INNOT uncoated carbide grades.
ISO N
Finishing
Uncoated
★ ITK10
Finishing
Uncoated
★ ITK10
Technical data sheet PDFCutting data, sizes and grades
Want to try it first? Request a free tester

Description
ISO specifications
| ISO | RADIUS (RE) | AVAILABLE GRADES | CHIPBREAKER |
|---|---|---|---|
| VCGT1103 | 0.2 – 0.4 | ITK10 – ITK20 | AK |
| VCGT1604 | 0.2 – 0.4 – 0.8 | ITK10 – ITK20 | AK |
AK chipbreaker data sheet
| Operation | Finishing |
| ISO material | N (aluminium alloys and non-ferrous metals) |
| Tolerance | G (ground insert) |
| Features | Chipbreaker for machining aluminium alloys. The large top and bottom rake angle makes the cutting edge sharper: cutting is faster and lighter, with effective chip breaking. Tolerance G (ground insert) for greater accuracy. 7° positive insert (shape V, 35° rhombic) with screw clamping: the slimmest tip in the range, for copy turning and profiling of grooves and radii. SVQC (107.5°) and SVUC (93°) type toolholders. |
Available INNOT grades
| Grade | ISO | Coating | Composition | Application |
|---|---|---|---|---|
| ITK10 ★ | N | Uncoated | Fine-grain carbide | First-choice grade for turning aluminium alloys. Uncoated carbide with a fine, uniform grain matrix: high transverse rupture strength and good wear resistance. |
| ITK20 | N | Uncoated | Carbide | Universal grade for turning aluminium alloys. Uncoated carbide with excellent wear resistance, better chipping resistance, great versatility and reliability. |
★ Recommended grade for this chipbreaker. Uncoated carbide, with a sharp cutting edge for gummy materials. ISO N = aluminium and non-ferrous metals.
Recommended cutting data
External turning of aluminium (ISO N) – AK chipbreaker
| Material | Condition | Vc (m/min) by grade | fn (mm/rev) | ap (mm) |
|---|---|---|---|---|
| Aluminium alloys and non-ferrous metals | Stable | ITK10: 300 – 700 ITK20: 300 – 700 |
0.10 – 0.30 | 0.50 – 3.00 |
| Aluminium alloys and non-ferrous metals | Average | ITK10: 300 – 700 ITK20: 300 – 700 |
0.10 – 0.25 | 0.50 – 3.00 |
| Aluminium alloys and non-ferrous metals | Difficult | ITK10: 300 – 700 ITK20: 300 – 700 |
0.10 – 0.20 | 0.50 – 3.00 |
Guide values for the AK chipbreaker (positive inserts), given only for the grades available in this product.
Internal turning / boring (ISO N)
| Material | Operation | Cut | RE | Vc (m/min) min – recomm. – max |
ap (mm) min – recomm. – max |
fn (mm/rev) min – recomm. – max |
|---|---|---|---|---|---|---|
| Copper, copper alloys, aluminium (Si < 10%) ≤ 100 HB |
High-speed finishing (bright surface) | Continuous | 0.4 – 0.8 | 200 – 400 – 1000 | 0.05 – 0.1 – 0.3 | 0.05 – 0.1 – 0.15 |
| Finishing | Continuous | 0.4 – 0.8 | 100 – 200 – 400 | 0.05 – 0.5 – 1.0 | 0.03 – 0.1 – 0.2 | |
| Interrupted | 100 – 200 – 400 | 0.05 – 0.5 – 1.0 | 0.03 – 0.1 – 0.2 |
Recommended grades: ITK10 – ITK20. Guide values for positive inserts, machining diameter over Ø10 mm. ap = radial depth of cut.
Depth of cut and insert size. The AK chipbreaker range goes up to ap 3 mm. The 35° shape has the slimmest tip in the range: with VCGT11 (11 mm cutting edge) keep the depth of cut within about 1/4 of the edge, i.e. about 2.5 mm. With VCGT16 (16.5 mm cutting edge) the full range can be used.
You may also like