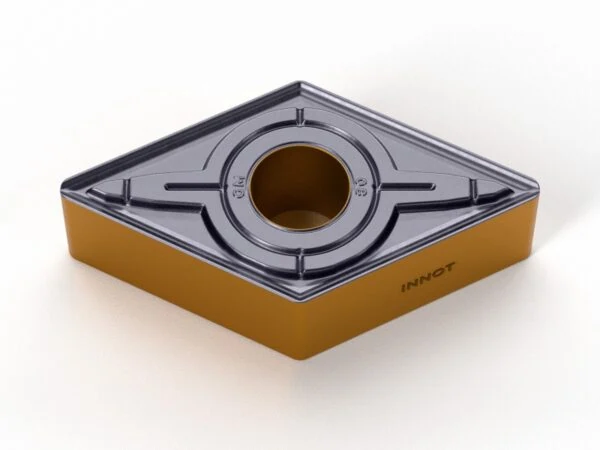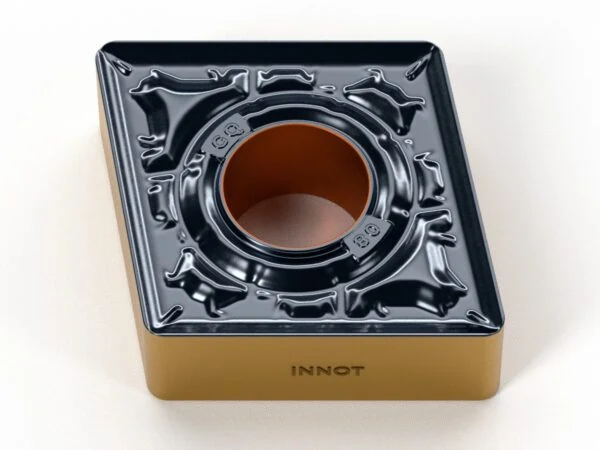
TNMG-BR
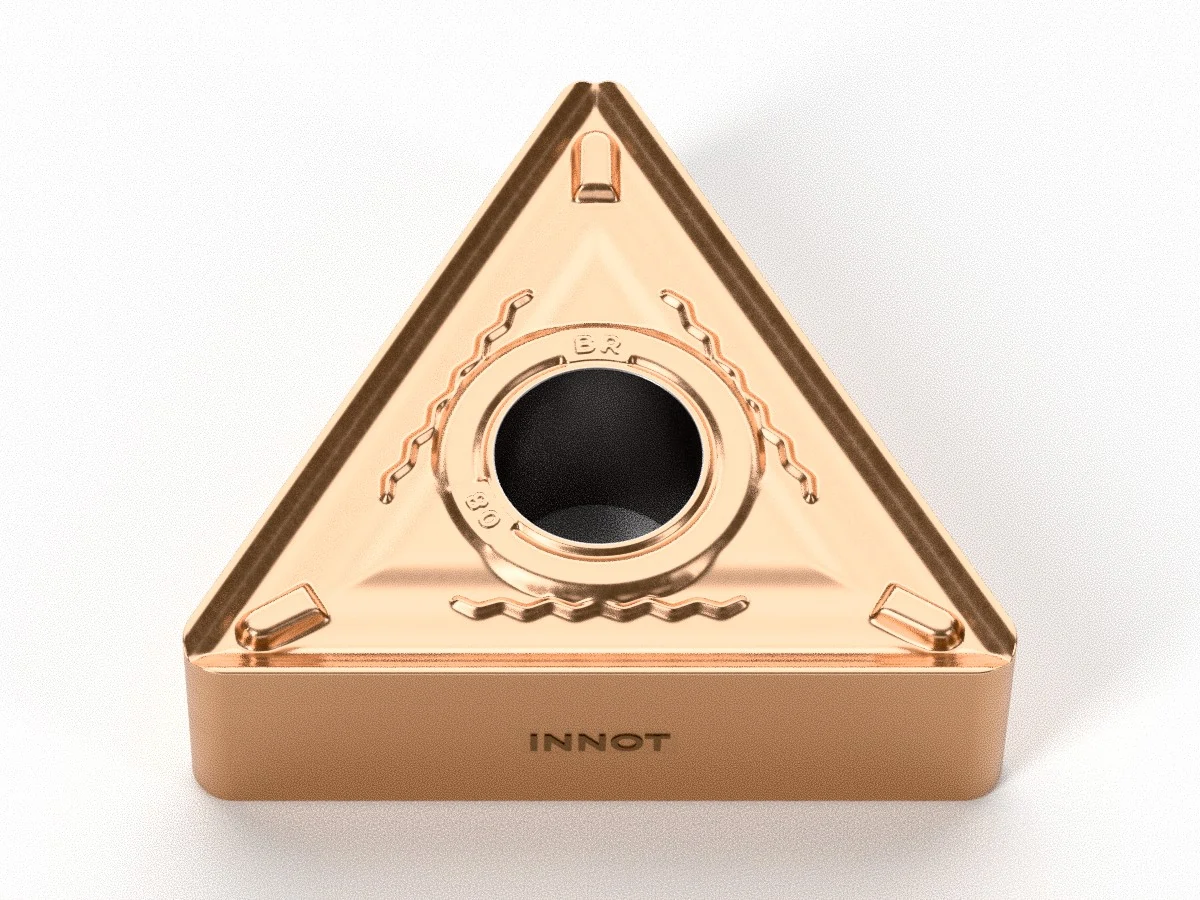
60° negative triangular insert for roughing stainless steels, with BR chipbreaker and INNOT PVD grades.
Roughing
PVD
★ IT7225
Technical data sheet PDFCutting data, sizes and grades
Want to try it first? Request a free tester

Description
ISO specifications
| ISO | RADIUS (RE) | AVAILABLE GRADES | CHIPBREAKER |
|---|---|---|---|
| TNMG1604 | 0.8 – 1.2 | IT7125 – IT7225 | BR |
BR chipbreaker data sheet
| Operation | Roughing |
| ISO material | M (stainless steels) |
| Tolerance | M |
| Features | Chipbreaker for roughing stainless steel. The optimised high-strength profile makes it suitable for interrupted cuts and light-load roughing; depths of cut and feeds in the cutting data table. 60° triangular shape: 6 usable cutting edges (3 per side), very versatile for longitudinal turning and facing with a wide choice of toolholders. |
Available INNOT grades
| Grade | ISO | Coating | Composition | Application |
|---|---|---|---|---|
| IT7125 | M | PVD | AlTiN | Universal grade for turning stainless steel in continuous and interrupted cuts. Smooth, low-friction coating, high nano-hardness and excellent oxidation resistance. |
| IT7225 ★ | M | PVD | AlTiSiN + TiSiN | First-choice grade for turning stainless steel. Nano-gradient coating on a sub-micron grain substrate: excellent wear resistance and toughness. |
★ Recommended grade for this chipbreaker. PVD = physical vapour deposition coating. ISO M = stainless steels.
Recommended cutting data
External turning of stainless steel (ISO M) – BR chipbreaker
Recommended cutting data by material and cutting condition (stable, average, difficult).
| Material | Condition | Vc (m/min) by grade | fn (mm/rev) | ap (mm) |
|---|---|---|---|---|
| Austenitic stainless steel ≤ 200 HB (AISI 304, 316…) |
Stable | IT7125: 80 – 150 IT7225: 80 – 150 |
0.18 – 0.66 | 1.70 – 7.00 |
| Austenitic stainless steel ≤ 200 HB (AISI 304, 316…) |
Average | IT7125: 80 – 150 IT7225: 80 – 150 |
0.18 – 0.61 | 1.70 – 7.00 |
| Austenitic stainless steel ≤ 200 HB (AISI 304, 316…) |
Difficult | IT7125: 80 – 150 IT7225: 80 – 150 |
0.18 – 0.56 | 1.70 – 7.00 |
| Martensitic stainless steel > 200 HB (AISI 431, 420…) |
Stable | IT7225: 70 – 140 | 0.18 – 0.66 | 1.70 – 7.00 |
| Martensitic stainless steel > 200 HB (AISI 431, 420…) |
Average | IT7225: 70 – 140 | 0.18 – 0.61 | 1.70 – 7.00 |
| Martensitic stainless steel > 200 HB (AISI 431, 420…) |
Difficult | IT7225: 70 – 140 | 0.18 – 0.56 | 1.70 – 7.00 |
Guide values for the BR chipbreaker. On martensitic stainless steel only IT7225 is recommended.
Internal turning (boring) of stainless steel (ISO M) – BR chipbreaker
Starting values for internal turning with a boring bar, derived from this insert's external turning data: cutting speed −15%, feed −20%, maximum depth of cut −40%. Negative inserts are mounted on boring bars for bores from about Ø 25 mm upwards (Ø 32–40 mm for the larger sizes).
| Material | Condition | Vc (m/min) by grade | fn (mm/rev) | ap (mm) |
|---|---|---|---|---|
| Austenitic stainless steel ≤ 200 HB (AISI 304, 316…) |
Stable | IT7125: 70 – 130 IT7225: 70 – 130 |
0.14 – 0.53 | 1.70 – 4.20 |
| Austenitic stainless steel ≤ 200 HB (AISI 304, 316…) |
Average | IT7125: 70 – 130 IT7225: 70 – 130 |
0.14 – 0.49 | 1.70 – 4.20 |
| Austenitic stainless steel ≤ 200 HB (AISI 304, 316…) |
Difficult | IT7125: 70 – 130 IT7225: 70 – 130 |
0.14 – 0.45 | 1.70 – 4.20 |
| Martensitic stainless steel > 200 HB (AISI 431, 420…) |
Stable | IT7225: 60 – 120 | 0.14 – 0.53 | 1.70 – 4.20 |
| Martensitic stainless steel > 200 HB (AISI 431, 420…) |
Average | IT7225: 60 – 120 | 0.14 – 0.49 | 1.70 – 4.20 |
| Martensitic stainless steel > 200 HB (AISI 431, 420…) |
Difficult | IT7225: 60 – 120 | 0.14 – 0.45 | 1.70 – 4.20 |
With a boring bar overhang above 3 times the diameter (steel bar) or 5 times (carbide or anti-vibration bar), reduce speed and feed further. Use the bar's internal coolant to clear the chips.
Grade selection by cutting condition
| Cutting condition | Recommended grade |
|---|---|
| Stable (continuous cut) | IT7225 |
| Average | IT7225 / IT7125 |
| Difficult (interrupted cut) | IT7125 |
IT7225 allows higher cutting speeds; IT7125 offers greater toughness in interrupted cuts.
You may also like