
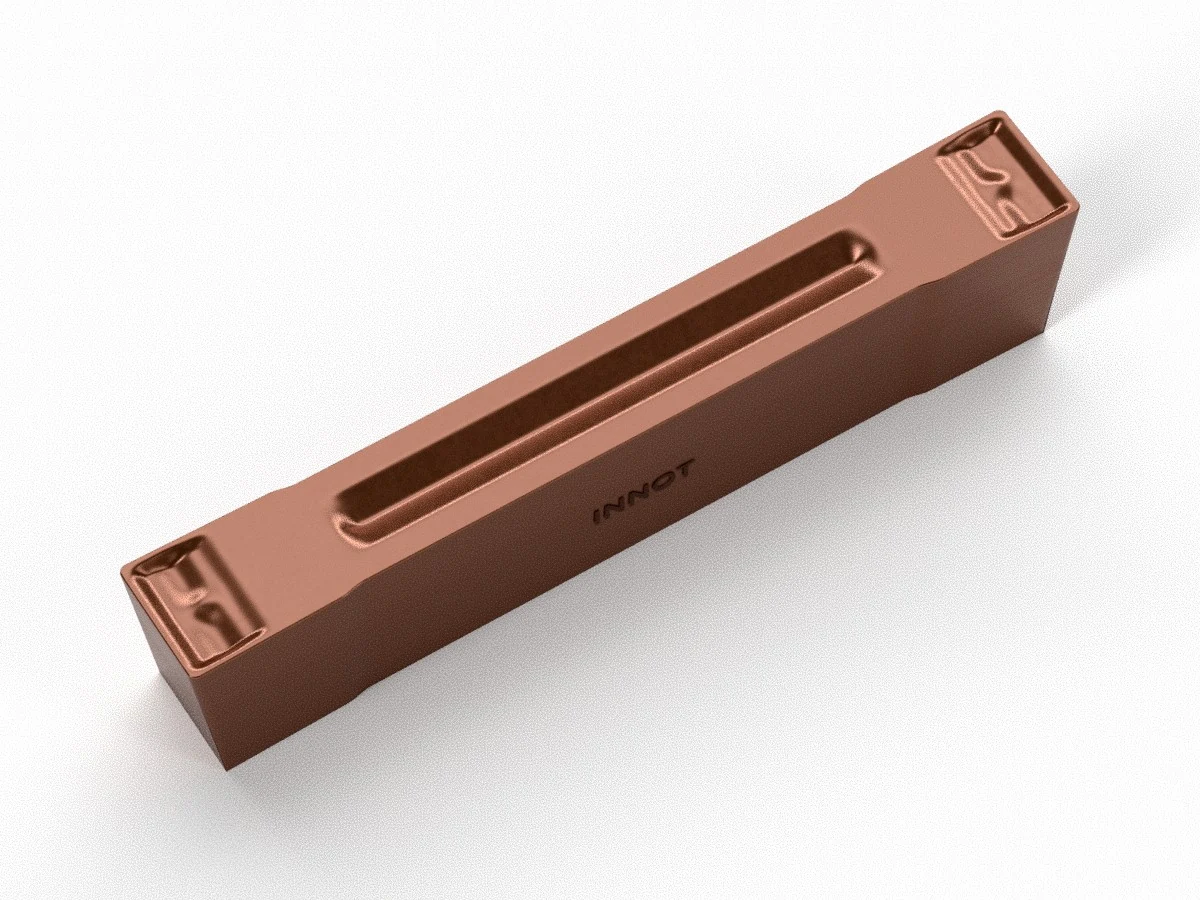
QCMB-GT
Double-ended insert for high-feed parting and grooving, with GT chipbreaker and INNOT CVD, PVD and cermet grades.
ISO P
ISO M
ISO K
Parting and grooving
High feed
★ IT8225 · IT7225
Technical data sheet PDFCutting data, sizes and grades
Want to try it first? Request a free tester

Description
Specifications
| Code | Width CW | Corner radius RE | INSL | Available grades |
|---|---|---|---|---|
| QCMB1502-GT | 1.5 mm (+0.05/0) | 0.2 | 16.0 | IT8225 – IT6115 – IT7125 – IT7225 – ITC10 |
| QCMB2002-GT | 2.0 mm (+0.05/0) | 0.2 | 16.0 | IT8225 – IT6115 – IT7125 – IT7225 – ITC10 |
| QCMB2502-GT | 2.5 mm (+0.05/0) | 0.2 | 18.5 | IT8225 – IT6115 – IT7125 – IT7225 – ITC10 |
| QCMB3002-GT | 3.0 mm (+0.05/0) | 0.2 | 21.0 | IT8225 – IT6115 – IT7125 – IT7225 – ITC10 |
| QCMB4002-GT | 4.0 mm (+0.05/0) | 0.2 | 21.0 | IT8225 – IT6115 – IT7125 – IT7225 – ITC10 |
| QCMB5003-GT | 5.0 mm (+0.05/0) | 0.3 | 26.0 | IT8225 – IT6115 – IT7125 – IT7225 – ITC10 |
| QCMB6003-GT | 6.0 mm (+0.05/0) | 0.3 | 26.0 | IT8225 – IT6115 – IT7125 – IT7225 – ITC10 |
CW = cutting width, RE = corner radius, INSL = insert length (mm).
GT chipbreaker data sheet
| Operation | Parting and grooving |
| ISO material | P (steels), M (stainless steels), K (cast irons) |
| Type | Two cutting edges |
| Tolerance | M |
| Features | Geometry designed for high-feed parting and grooving: narrow, controlled chips even at high feeds, for shorter cycle times. |
| Compatible toolholders | Toolholders for external and face grooves, boring bars for internal grooves |
Available INNOT grades
| Grade | ISO | Coating | Composition | Application |
|---|---|---|---|---|
| IT8225 ★ | P | CVD | TiN + MT-TiCN + Al₂O₃ | First-choice grade for steel, very versatile. Multilayer coating with excellent wear resistance and toughness. |
| IT6115 | K | CVD | TiN + MT-TiCN + Al₂O₃ | First-choice grade for turning cast iron. Thicker black CVD coating with special post-coating treatment: excellent wear resistance and toughness. Also suitable for roughing high-strength steels. |
| IT7125 | M | PVD | AlTiN | Universal grade for turning stainless steel in continuous and interrupted cuts. Smooth, low-friction coating, high nano-hardness and excellent oxidation resistance. |
| IT7225 ★ | M | PVD | AlTiSiN + TiSiN | First-choice grade for turning stainless steel. Nano-gradient coating on a sub-micron grain substrate: excellent wear resistance and toughness. |
| ITC10 | P | Cermet | Uncoated | New-generation, very stable cermet: ideal for finishing low-carbon steels and wherever high surface quality is needed. Hard, compact surface, excellent chemical stability, wear and chipping resistance. |
★ Recommended grade for this insert. CVD = chemical vapour deposition coating, PVD = physical vapour deposition coating.
Recommended cutting data
Parting and grooving – cutting speed
Cutting speed Vc (m/min) as a function of feed fn (mm/rev)
| Material | HB | Rm (N/mm²) | IT8225 | IT7225 | IT6115 | ||||||
|---|---|---|---|---|---|---|---|---|---|---|---|
| fn 0.1 | fn 0.3 | fn 0.5 | fn 0.1 | fn 0.3 | fn 0.5 | fn 0.1 | fn 0.3 | fn 0.5 | |||
| NON-ALLOY STEELS | |||||||||||
| C≤0.25% – Annealed | 125 | 428 | 280 | 200 | 130 | 260 | 180 | 120 | – | – | – |
| 0.25<C≤0.55% – Annealed | 190 | 639 | 240 | 160 | 115 | 200 | 140 | 105 | – | – | – |
| 0.25<C≤0.55% – Quenched and tempered | 210 | 708 | 130 | 115 | 100 | 120 | 110 | 100 | – | – | – |
| C>0.55% – Annealed | 190 | 639 | 145 | 130 | 115 | 130 | 120 | 110 | – | – | – |
| C>0.55% – Quenched and tempered | 300 | 1013 | 115 | 100 | 80 | 110 | 95 | 70 | – | – | – |
| Short-chipping – Annealed | 220 | 745 | 130 | 115 | 100 | 120 | 105 | 90 | – | – | – |
| LOW-ALLOY STEELS | |||||||||||
| Annealed | 175 | 591 | 280 | 200 | 130 | 170 | 135 | 120 | – | – | – |
| Quenched and tempered | 300 | 1013 | 115 | 100 | 80 | 105 | 90 | 70 | – | – | – |
| Quenched and tempered | 380 | 1282 | 170 | 90 | 70 | 160 | 80 | 60 | – | – | – |
| STAINLESS STEELS | |||||||||||
| Ferritic / martensitic – Annealed | 200 | 675 | – | – | – | 200 | 150 | 105 | – | – | – |
| Martensitic – Quenched and tempered | 330 | 1114 | – | – | – | 150 | 115 | 70 | – | – | – |
| Austenitic – Solution annealed | 200 | 675 | – | – | – | 185 | 155 | 125 | – | – | – |
| Precipitation-hardening austenitic (PH) | 300 | 1013 | – | – | – | 165 | 135 | 95 | – | – | – |
| Austenitic-ferritic (duplex) | 230 | 778 | – | – | – | 145 | 110 | 85 | – | – | – |
| CAST IRONS | |||||||||||
| Ferritic malleable | 200 | 400 | – | – | – | – | – | – | 220 | 160 | 80 |
| Pearlitic malleable | 260 | 700 | – | – | – | – | – | – | 115 | 90 | 65 |
| Grey – low strength | 180 | 200 | – | – | – | – | – | – | 260 | 220 | 150 |
| Grey – high strength / austenitic | 245 | 350 | – | – | – | – | – | – | 240 | 200 | 130 |
| Ferritic ductile | 155 | 400 | – | – | – | – | – | – | 160 | 130 | 80 |
| Pearlitic ductile | 265 | 700 | – | – | – | – | – | – | 145 | 110 | 80 |
| Compacted graphite iron (CGI) | 230 | 400 | – | – | – | – | – | – | 150 | 120 | 90 |
Guide values for machining with coolant. For parting and internal grooving reduce the speed by 30–50%. When parting, as you approach the centre of the part, reduce the feed by 30%.
Tips for use
- Parting off: when approaching the centre reduce the feed by 30% for longer life and a better finish; keep the tool overhang to a minimum.
- External grooving and side turning: with depths over 0.5 mm work in radial passes (up to 0.75 × insert width), retract 0.1 mm, then an axial pass.
- Wide grooves: make side-by-side stepped plunges, then finish the bottom and the flanks.
- Face grooves: start from the largest diameter and move inwards; for finishing machine the bottom and the outer diameter first, then the inner one.
- Internal grooves: work from the inside outwards to help the chip out.
You may also like
Recently viewed
VNMG-GF






