
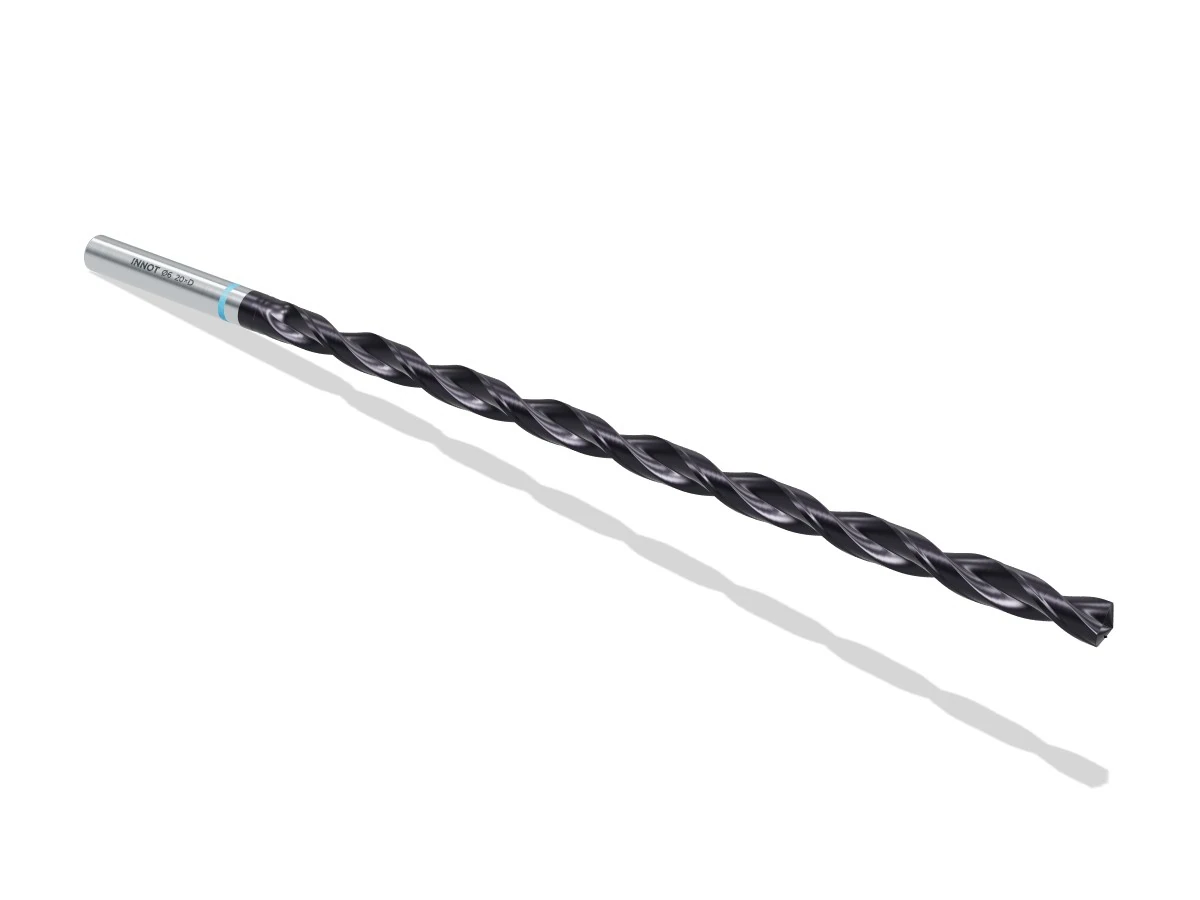
20×D solid carbide drill
Drill for very deep holes up to 20 times the diameter: double-margin geometry for hole straightness and high-pressure coolant.
ISO P
ISO M
ISO K
ISO N
ISO S
ISO H
20×D
Ø 3–14 mm
135° point
Technical data sheet PDFCutting data, sizes and grades
Want to try it first? Request a free tester

Description
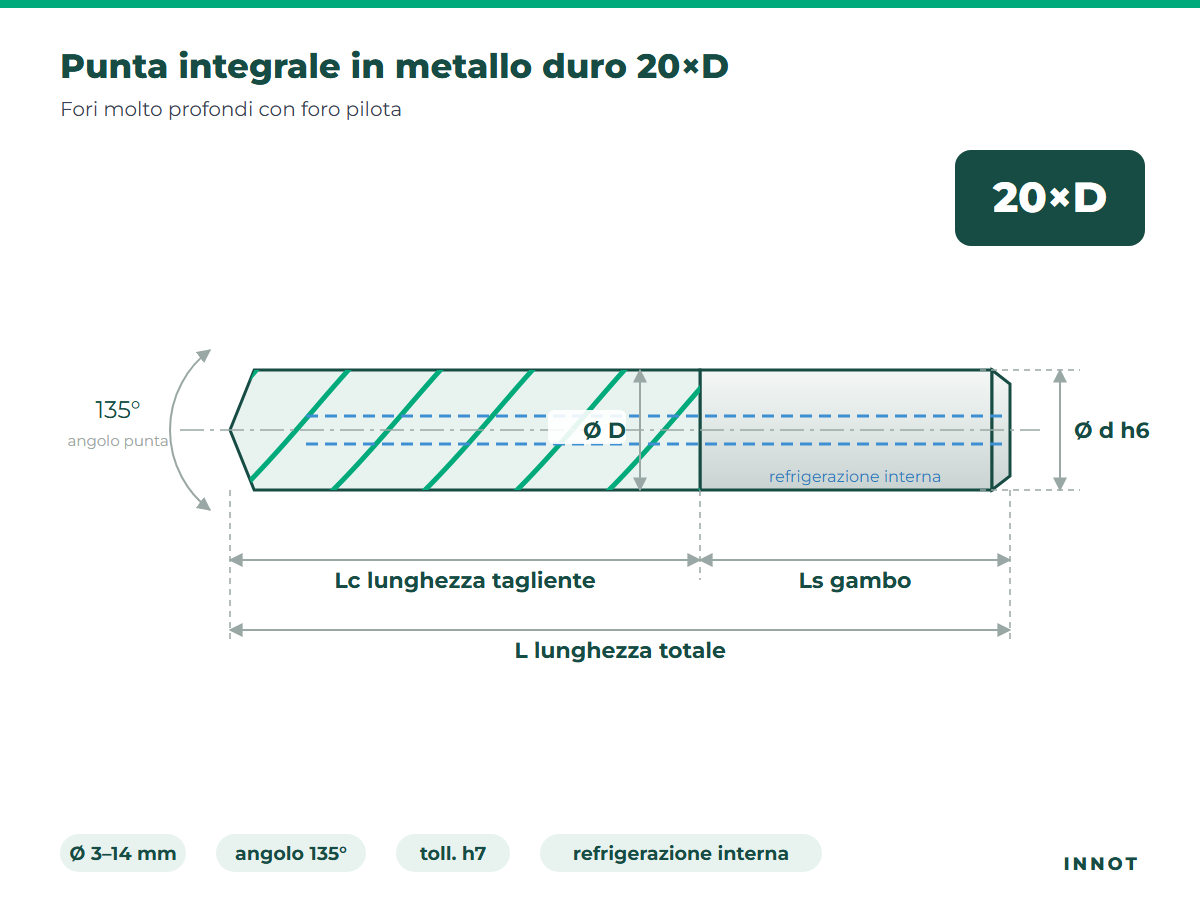
Technical drawing
Reference dimensions
| Drill Ø D | Ø d shank | L overall | Lc cutting length | Ls shank |
|---|---|---|---|---|
| Ø 3 | 6 | 110 | 70 | 36 |
| Ø 4 | 6 | 136 | 96 | 36 |
| Ø 5 | 6 | 158 | 118 | 36 |
| Ø 6 | 6 | 180 | 140 | 36 |
| Ø 8 | 8 | 223 | 183 | 36 |
| Ø 10 | 10 | 272 | 228 | 40 |
| Ø 12 | 12 | 325 | 275 | 45 |
| Ø 14 | 14 | 367 | 318 | 45 |
Dimensions in mm. All intermediate diameters are available, also to the hundredth (e.g. Ø6.8 for M8 or Ø10.2 for M12): shank and lengths follow the diameter range.
Features
| Drilling depth | up to 20×D (20 times the diameter) |
| Diameters | Ø 3 – 14 mm, in 0.01 mm steps |
| Point angle | 135° self-centring, double margin |
| Ø D tolerance | h7 |
| Shank | Cylindrical h6 (DIN 6535 HA); with Weldon flat on request |
| Coolant | Internal, two helical channels |
| ISO materials | P steels, M stainless steels, K cast irons, N aluminium, S superalloys and titanium, H hardened: rod and coating are chosen for the material |
| Construction | Standard (deep-hole series) or custom made: lengths, steps, chamfers and angles to drawing |
Tips for use
- Drill a pilot hole 1.5–2×D deep with a short drill of the same diameter.
- Enter the pilot hole at low speed and without coolant, then start the coolant and the working speed.
- Recommended coolant pressure: at least 20 bar (better 40 bar or more beyond 20×D).
Coatings
All coatings are available on this tool, also in custom versions:
TiNTiCNTiAlNAlTiNAlCrNTiSiNAlTiSiNAlCrSiNCrNZrNTiB2DLCta-CCVD diamondUncoatedNeed a different drill?
Diameter, length, step, angle, coolant, carbide rod and coating: configure the drill and receive the quote within 30 minutes.
You may also like
Custom step drill
Available
30×D solid carbide drill
Available
PSteelNAluminiumKCast ironMStainlessSSuperalloys
Indexable drills 2×D – 5×D
Available
3×D solid carbide drill
Available
PSteelNAluminiumKCast ironMStainlessSSuperalloys
5×D solid carbide drill
Available
PSteelNAluminiumKCast ironMStainlessSSuperalloys
Recently viewed
12×D solid carbide drill
Available
PSteelNAluminiumKCast ironMStainlessSSuperalloys






