
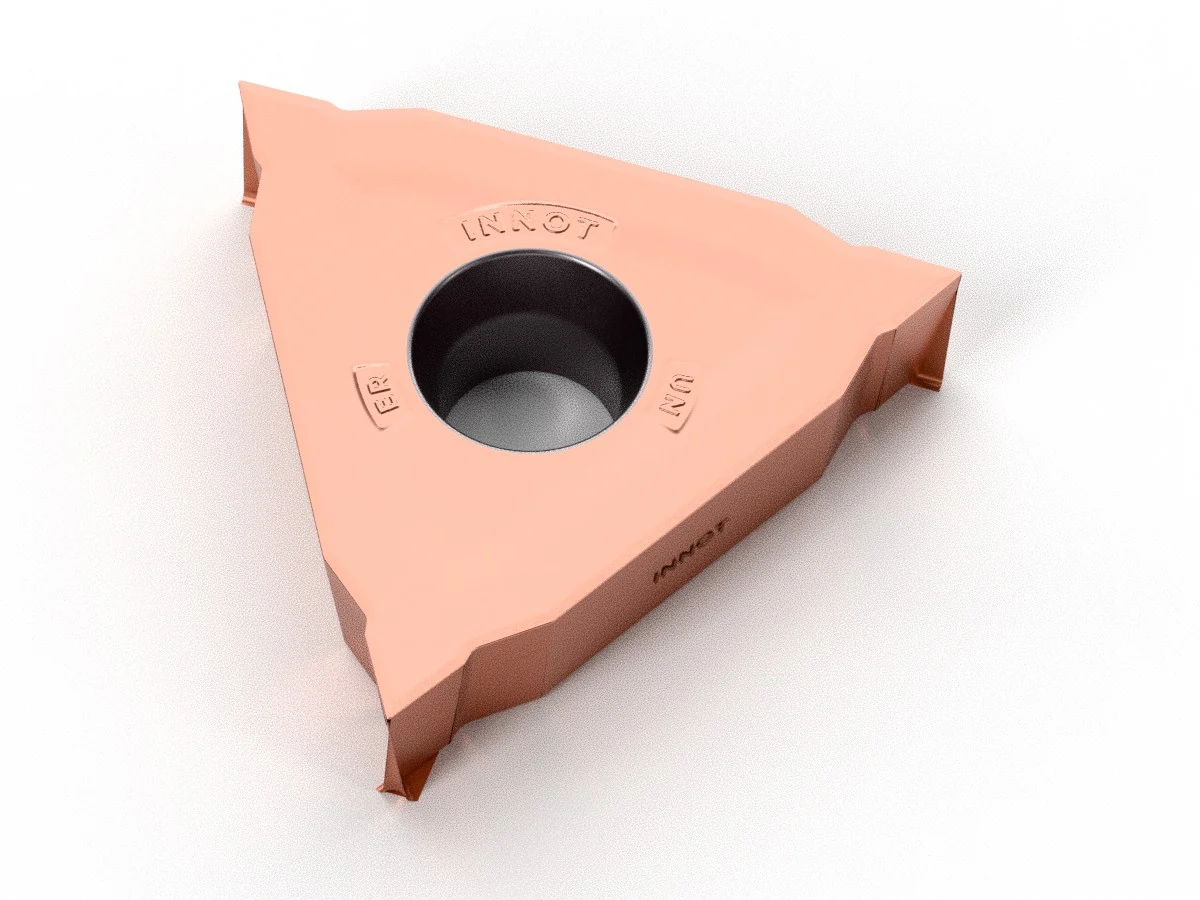
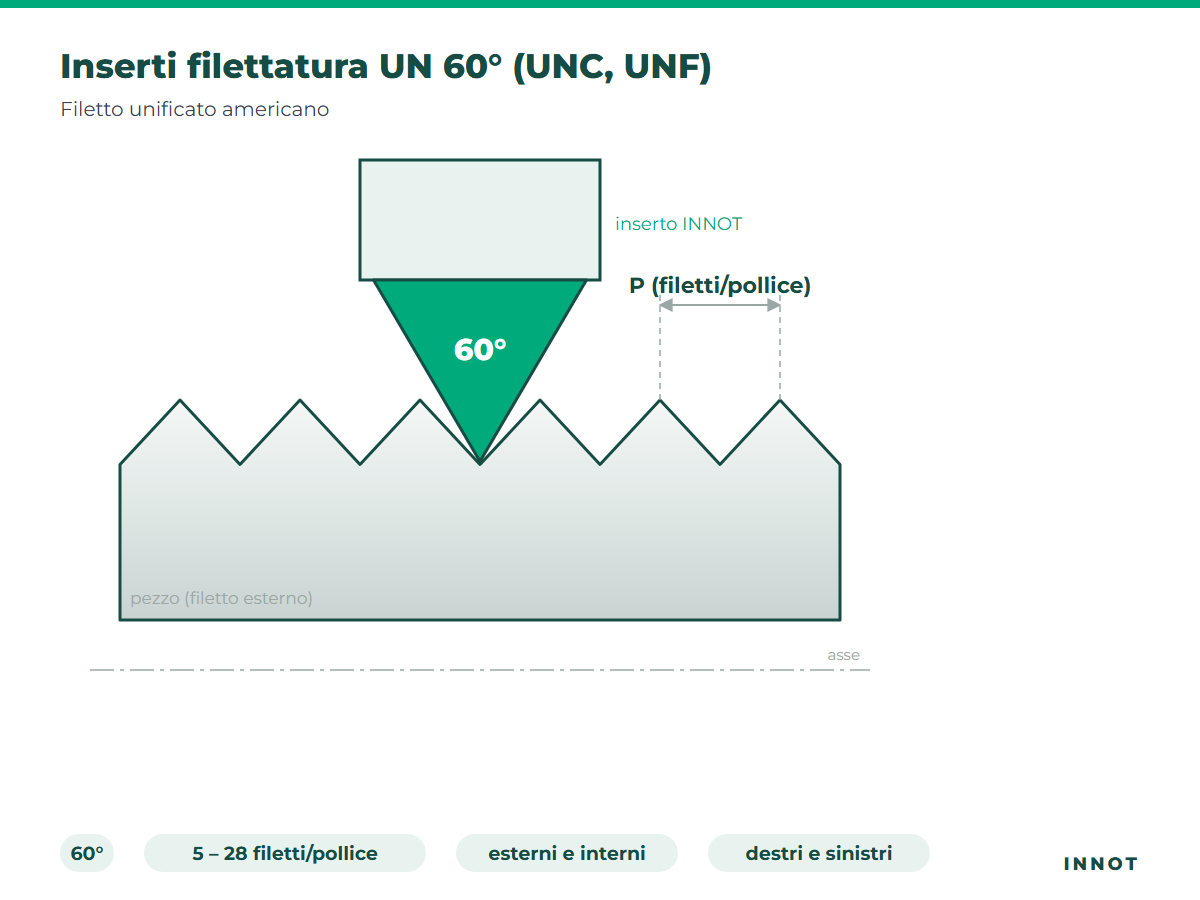
UN 60° threading inserts (UNC, UNF)
Full-profile inserts for UN 60° unified threads (UNC, UNF, UNEF), required in aerospace and hydraulics.
ISO P
ISO M
ISO S
Threading
5 – 28 threads per inch
★ IT5225
Technical data sheet PDFCutting data, sizes and grades
Want to try it first? Request a free tester
Fits on

Description
Profile
Range
| Profile | 60° |
| Pitch range | 5 – 28 threads per inch |
| Type | External (E) and internal (I), right-hand (R) and left-hand (L) |
| Insert size | Inscribed circle 6.35 (11), 9.525 (16) and 12.70 mm (22); 3.97 and 4.76 mm for small internal bores |
| Construction | Sintered with chipbreaker, or precision ground (P) for tight tolerances and finish |
| Typical application | Aerospace, hydraulics and components for the American market. |
Available INNOT grades
| Grade | ISO | Coating | Composition | Application |
|---|---|---|---|---|
| IT5225 ★ | P · M · S | PVD | Multilayer PVD | First-choice grade for threading: steels, stainless steels and superalloys, excellent resistance to profile wear. |
| IT5125 | P · M · S | PVD | Multilayer PVD | Tough grade for threading in unstable conditions and interrupted cuts on steels, stainless steels and superalloys. |
★ Recommended grade. On request also CVD grades for steels and cast irons, uncoated carbide for aluminium and cermet for finishing.
Tips for use
- Decreasing depth of cut: lighter passes as you approach the thread root.
- Flank infeed (modified infeed at 3–5° on the flank) for better chip control and longer insert life.
- Choose the shim according to the thread helix angle: flanks that do not rub and a correct profile.
Which insert for your thread?
Tell us the thread (e.g. M20×2.5 external or 1/2″ NPT internal), material and toolholder: we tell you insert and grade with the quote.
You may also like
CNMM-GX
Available
PSteelHeavy-duty machining
DNMG-BM
Available
MStainlessSemi-finishing
DNMG-SM
Available
SSuperalloysSemi-finishing · Roughing
DNMG-GM
Available
PSteelSemi-finishing
CNMG cast iron
Available
KCast ironSemi-finishing · Roughing
Recently viewed
XNMX / XNGX
Available
HHardenedPSteelKCast ironMStainlessSSuperalloysFace milling · Finishing
NPT 60° threading inserts
Available
PSteelMStainlessSSuperalloysSpecial






