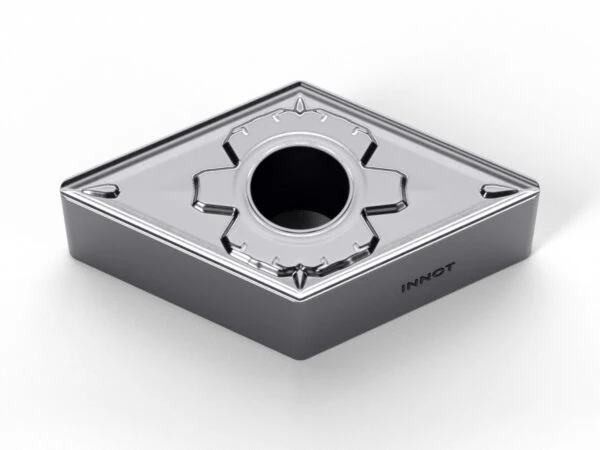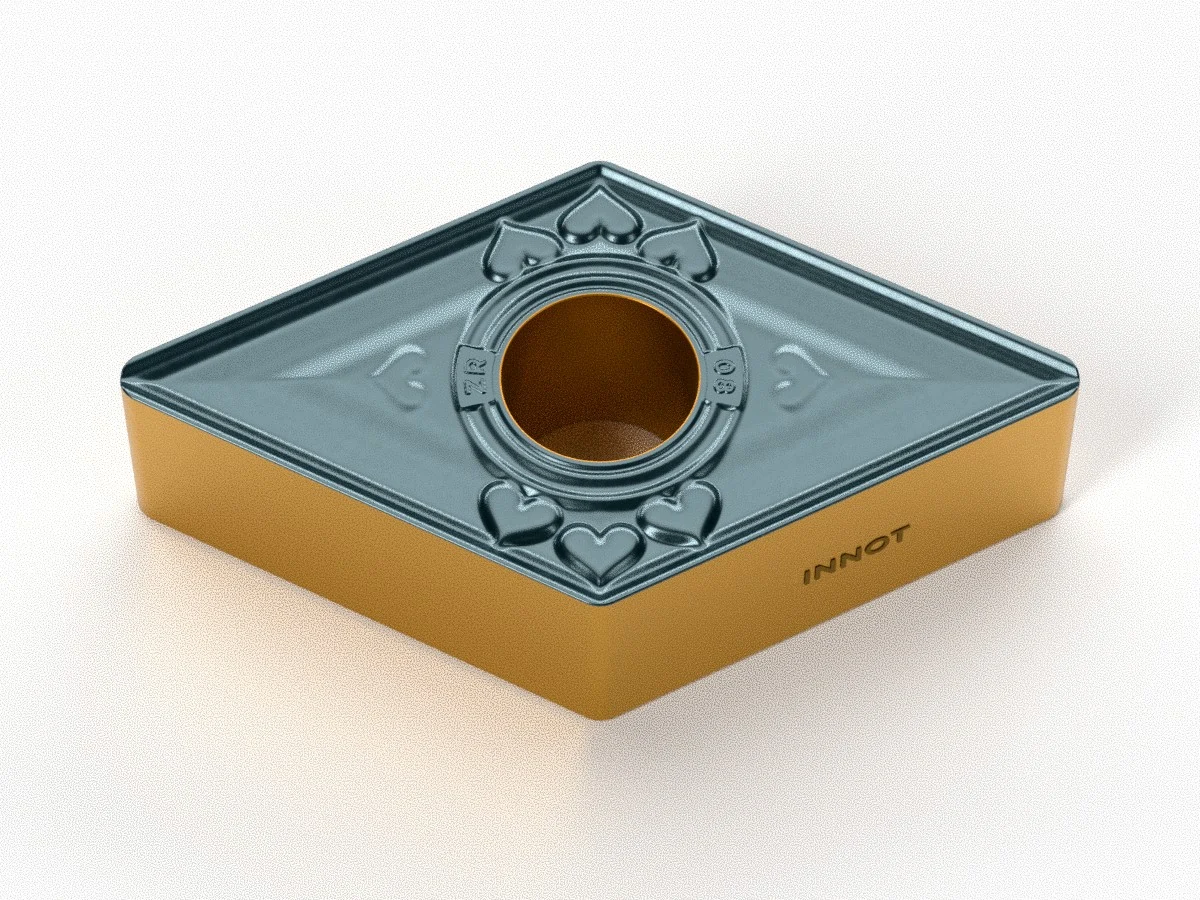
DNMG-ZR
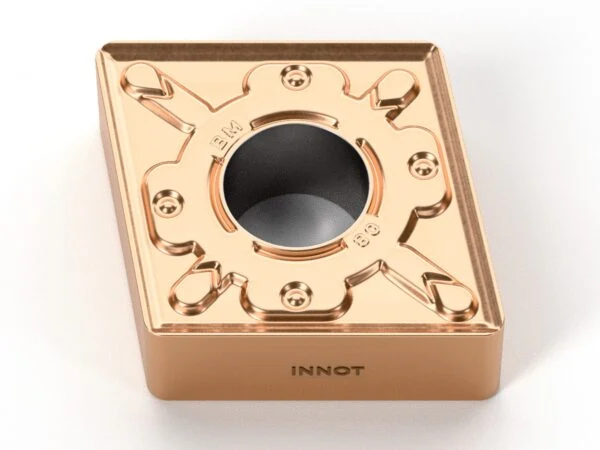
55° negative insert for turning ductile cast iron, with ZR chipbreaker and CVD grade IT6215.
Finishing – roughing
CVD
★ IT6215
Technical data sheet PDFCutting data, sizes and grades
Want to try it first? Request a free tester

Description
ISO specifications
| ISO | RADIUS (RE) | AVAILABLE GRADES | CHIPBREAKER |
|---|---|---|---|
| DNMG1504 | 0.4 – 0.8 – 1.2 | IT6215 | ZR |
| DNMG1506 | 0.4 – 0.8 – 1.2 | IT6215 | ZR |
ZR chipbreaker data sheet
| Operation | Finishing – roughing |
| ISO material | K (ductile cast iron, also suitable for grey cast iron) |
| Tolerance | M |
| Features | Chipbreaker developed for ductile cast iron: it balances sharpness and edge strength, with low cutting forces and high quality. It ensures excellent reliability even with heavy impacts and is also suitable for turning grey cast iron, with great versatility and wear resistance. 55° rhombic shape: a slimmer tip than the 80°, ideal for profiling, copy turning and contour turning with access to shoulders. |
Available INNOT grades
| Grade | ISO | Coating | Composition | Application |
|---|---|---|---|---|
| IT6215 ★ | K | CVD | TiN + MT-TiCN + Al₂O₃ | First-choice grade for ductile cast iron. Second-generation CVD coating with greater cohesion between layers, preventing flaking; the post-coating treatment increases impact resistance. Particularly suitable for interrupted cuts. |
★ Recommended grade for this chipbreaker. CVD = chemical vapour deposition coating. ISO K = cast irons.
Recommended cutting data
External turning of ductile cast iron (ISO K) – ZR chipbreaker
Recommended cutting data by material and cutting condition.
| Material | Condition | Vc (m/min) by grade | fn (mm/rev) | ap (mm) |
|---|---|---|---|---|
| Ductile cast iron ≤ 450 MPa (GGG40, GGG50 – EN-GJS-400, EN-GJS-500) |
Stable | IT6215: 145 – 285 | 0.15 – 0.50 | 0.50 – 5.00 |
| Ductile cast iron ≤ 450 MPa (GGG40, GGG50 – EN-GJS-400, EN-GJS-500) |
Average | IT6215: 145 – 285 | 0.15 – 0.50 | 0.50 – 5.00 |
| Ductile cast iron ≤ 450 MPa (GGG40, GGG50 – EN-GJS-400, EN-GJS-500) |
Difficult | IT6215: 145 – 285 | 0.15 – 0.50 | 0.50 – 5.00 |
Guide values. The ZR chipbreaker is also suitable for grey cast iron.
Internal turning (boring) of ductile cast iron (ISO K) – ZR chipbreaker
Starting values for internal turning with a boring bar, derived from this insert's external turning data: cutting speed −15%, feed −20%, maximum depth of cut −40%. Negative inserts are mounted on boring bars for bores from about Ø 25 mm upwards (Ø 32–40 mm for the larger sizes).
| Material | Condition | Vc (m/min) by grade | fn (mm/rev) | ap (mm) |
|---|---|---|---|---|
| Ductile cast iron ≤ 450 MPa (GGG40, GGG50 – EN-GJS-400, EN-GJS-500) |
Stable | IT6215: 125 – 240 | 0.12 – 0.40 | 0.50 – 3.00 |
| Ductile cast iron ≤ 450 MPa (GGG40, GGG50 – EN-GJS-400, EN-GJS-500) |
Average | IT6215: 125 – 240 | 0.12 – 0.40 | 0.50 – 3.00 |
| Ductile cast iron ≤ 450 MPa (GGG40, GGG50 – EN-GJS-400, EN-GJS-500) |
Difficult | IT6215: 125 – 240 | 0.12 – 0.40 | 0.50 – 3.00 |
With a boring bar overhang above 3 times the diameter (steel bar) or 5 times (carbide or anti-vibration bar), reduce speed and feed further. Use the bar's internal coolant to clear the chips.
Cutting data on ductile cast iron EN-GJS-600 (GGG60) – IT6215
Guide values by type of operation.
| Condition | Operation | Vc (m/min) | fn (mm/rev) | ap (mm) |
|---|---|---|---|---|
| Stable | Finishing | 230 – 365 | 0.10 – 0.30 | 0.2 – 1.0 |
| Stable | Semi-finishing | 210 – 335 | 0.20 – 0.35 | 0.5 – 1.5 |
| Stable | Roughing | 195 – 315 | 0.25 – 0.40 | 1.0 – 3.0 |
| Average / Difficult | Finishing | 205 – 335 | 0.10 – 0.30 | 0.2 – 1.0 |
| Average / Difficult | Semi-finishing | 190 – 305 | 0.20 – 0.35 | 0.5 – 1.5 |
| Average / Difficult | Roughing | 180 – 285 | 0.25 – 0.40 | 1.0 – 3.0 |
You may also like