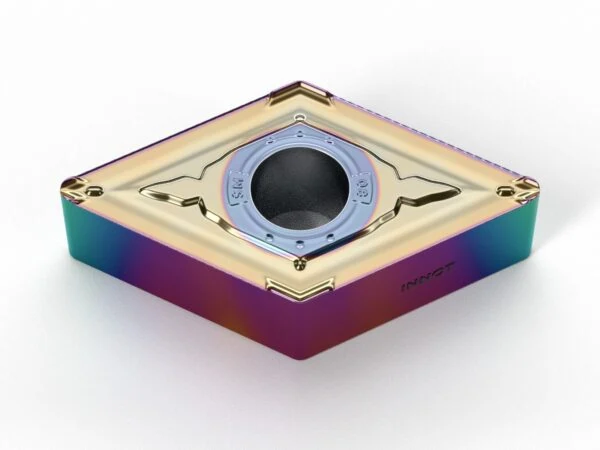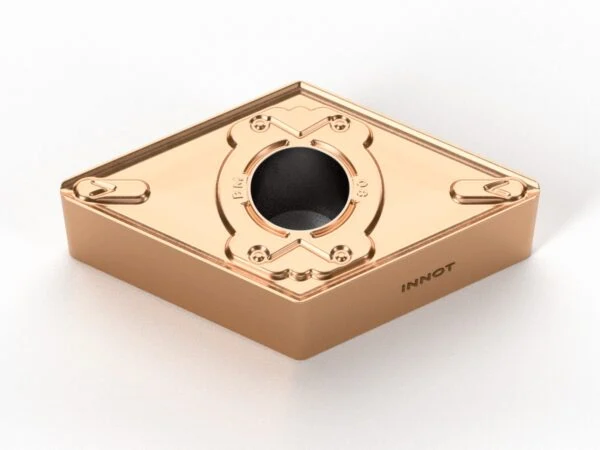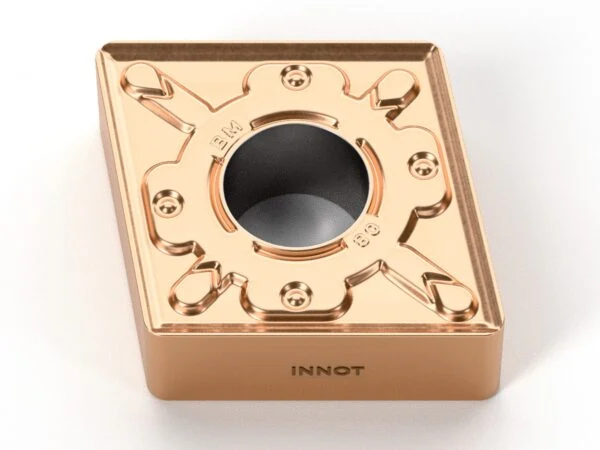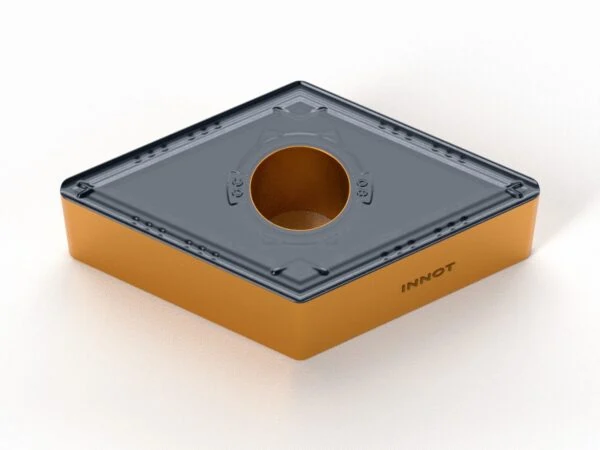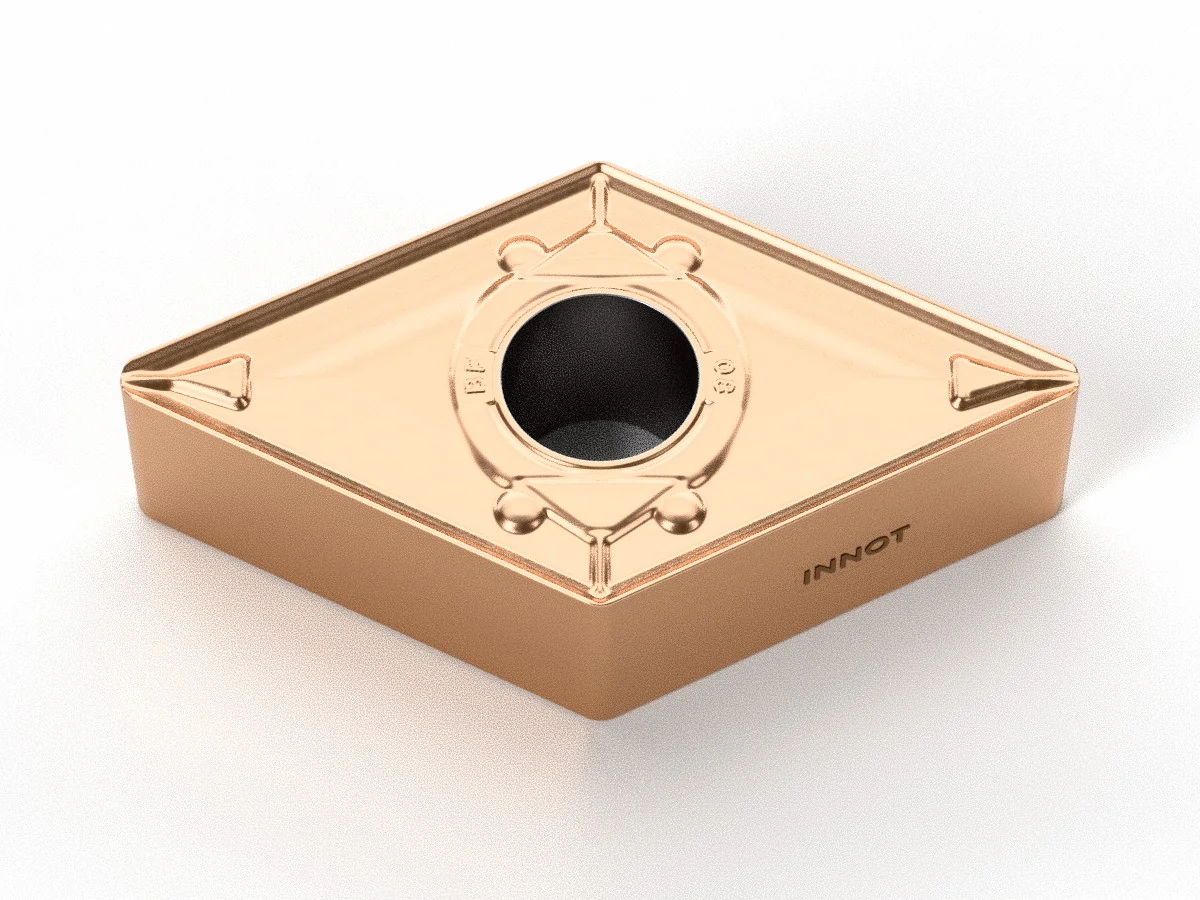
DNMG-BF
55° negative insert for finishing stainless steels, with BF chipbreaker and INNOT PVD grades.
Finishing
PVD
★ IT7225
Technical data sheet PDFCutting data, sizes and grades
Want to try it first? Request a free tester

Description
ISO specifications
| ISO | RADIUS (RE) | AVAILABLE GRADES | CHIPBREAKER |
|---|---|---|---|
| DNMG1504 | 0.4 – 0.8 | IT7125 – IT7225 | BF |
| DNMG1506 | 0.4 – 0.8 | IT7125 – IT7225 | BF |
BF chipbreaker data sheet
| Operation | Finishing |
| ISO material | M (stainless steels) |
| Tolerance | M |
| Features | Chipbreaker dedicated to finishing stainless steel. Low cutting forces and excellent chip control. The sharp cutting edge is the ideal solution for finishing with small depths of cut, limiting work hardening of the material. 55° rhombic shape: a slimmer tip than the 80°, ideal for profiling, copy turning and contour turning with access to shoulders. |
Available INNOT grades
| Grade | ISO | Coating | Composition | Application |
|---|---|---|---|---|
| IT7125 | M | PVD | AlTiN | Universal grade for turning stainless steel in continuous and interrupted cuts. Smooth, low-friction coating, high nano-hardness and excellent oxidation resistance. |
| IT7225 ★ | M | PVD | AlTiSiN + TiSiN | First-choice grade for turning stainless steel. Nano-gradient coating on a sub-micron grain substrate: excellent wear resistance and toughness. |
★ Recommended grade for this chipbreaker. PVD = physical vapour deposition coating. ISO M = stainless steels.
Recommended cutting data
External turning of stainless steel (ISO M) – BF chipbreaker
Recommended cutting data by material and cutting condition (stable, average, difficult).
| Material | Condition | Vc (m/min) by grade | fn (mm/rev) | ap (mm) |
|---|---|---|---|---|
| Austenitic stainless steel ≤ 200 HB (AISI 304, 316…) |
Stable | IT7125: 95 – 185 IT7225: 95 – 185 |
0.08 – 0.30 | 0.20 – 2.00 |
| Austenitic stainless steel ≤ 200 HB (AISI 304, 316…) |
Average | IT7125: 95 – 185 IT7225: 95 – 185 |
0.08 – 0.25 | 0.20 – 2.00 |
| Martensitic stainless steel > 200 HB (AISI 431, 420…) |
Stable | IT7225: 85 – 175 | 0.08 – 0.30 | 0.20 – 2.00 |
| Martensitic stainless steel > 200 HB (AISI 431, 420…) |
Average | IT7225: 85 – 175 | 0.08 – 0.25 | 0.20 – 2.00 |
Guide values for the BF chipbreaker. On martensitic stainless steel only IT7225 is recommended.
Internal turning (boring) of stainless steel (ISO M) – BF chipbreaker
Starting values for internal turning with a boring bar, derived from this insert's external turning data: cutting speed −15%, feed −20%, maximum depth of cut −40%. Negative inserts are mounted on boring bars for bores from about Ø 25 mm upwards (Ø 32–40 mm for the larger sizes).
| Material | Condition | Vc (m/min) by grade | fn (mm/rev) | ap (mm) |
|---|---|---|---|---|
| Austenitic stainless steel ≤ 200 HB (AISI 304, 316…) |
Stable | IT7125: 80 – 155 IT7225: 80 – 155 |
0.06 – 0.24 | 0.20 – 1.20 |
| Austenitic stainless steel ≤ 200 HB (AISI 304, 316…) |
Average | IT7125: 80 – 155 IT7225: 80 – 155 |
0.06 – 0.20 | 0.20 – 1.20 |
| Martensitic stainless steel > 200 HB (AISI 431, 420…) |
Stable | IT7225: 70 – 150 | 0.06 – 0.24 | 0.20 – 1.20 |
| Martensitic stainless steel > 200 HB (AISI 431, 420…) |
Average | IT7225: 70 – 150 | 0.06 – 0.20 | 0.20 – 1.20 |
With a boring bar overhang above 3 times the diameter (steel bar) or 5 times (carbide or anti-vibration bar), reduce speed and feed further. Use the bar's internal coolant to clear the chips.
Grade selection by cutting condition
| Cutting condition | Recommended grade |
|---|---|
| Stable (continuous cut) | IT7225 |
| Average | IT7225 / IT7125 |
| Difficult (interrupted cut) | IT7125 |
IT7225 allows higher cutting speeds; IT7125 offers greater toughness in interrupted cuts.
You may also like