
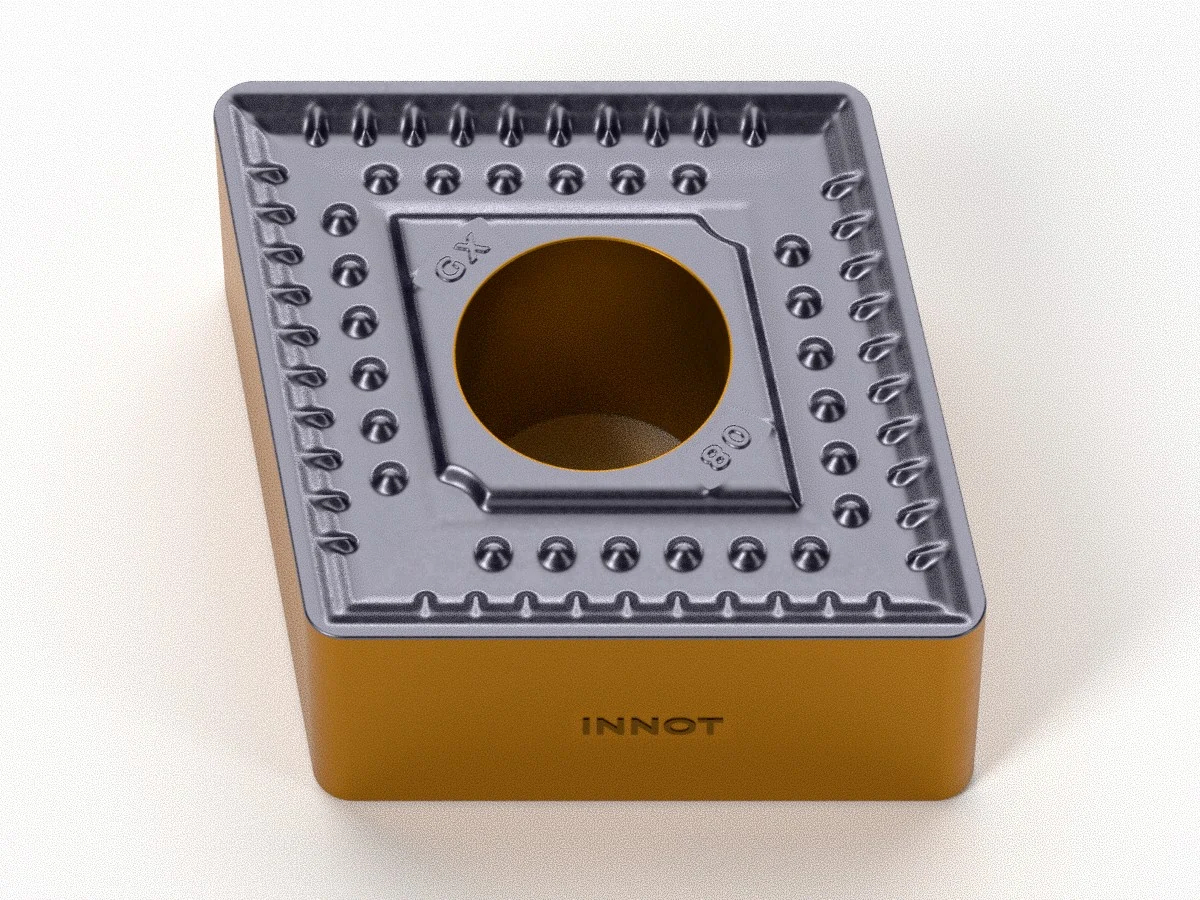
CNMM-GX
80° negative insert for heavy roughing of steels, with GX chipbreaker and INNOT CVD grades. For the deepest cuts and the highest feeds.
Heavy roughing
CVD
★ IT8115 · IT8225
Technical data sheet PDFCutting data, sizes and grades
Want to try it first? Request a free tester

Description
ISO specifications
| ISO | RADIUS (RE) | AVAILABLE GRADES | CHIPBREAKER |
|---|---|---|---|
| CNMM1906 | 0.8 – 1.2 – 1.6 – 2.4 | IT8115 – IT8125 – IT8225 – IT8135 | GX |
| CNMM2507 | 1.6 – 2.4 – 3.2 | IT8115 – IT8125 – IT8225 – IT8135 | GX |
| CNMM2509 | 1.6 – 2.4 – 3.2 | IT8115 – IT8125 – IT8225 – IT8135 | GX |
GX chipbreaker data sheet
| Operation | Heavy roughing |
| ISO material | P (non-alloy, alloy and tool steels) |
| Tolerance | M |
| Features | Chipbreaker for the heaviest operations. The variable chamfer and the special chipbreaker design ensure excellent chip control; the strong cutting edge withstands heavy impacts. Suitable for depths of cut up to 13 mm and feeds up to 1.3 mm/rev. |
Available INNOT grades
| Grade | ISO | Coating | Composition | Application |
|---|---|---|---|---|
| IT8115 ★ | P | CVD | TiN + MT-TiCN + Al₂O₃ | Continuous and lightly interrupted cuts. Finishing and semi-finishing of carbon and alloy steels. |
| IT8125 | P | CVD | TiN + MT-TiCN + Al₂O₃ | Interrupted and continuous cuts on steel. The reinforced substrate limits plastic deformation at high temperature. |
| IT8225 ★ | P | CVD | TiN + MT-TiCN + Al₂O₃ | First-choice grade for steel, very versatile. Multilayer coating with excellent wear resistance and toughness. |
| IT8135 | P | CVD | TiN + MT-TiCN + Al₂O₃ | Grade for turning steel with heavy impacts. High-toughness substrate and reinforced binder phase: excellent impact resistance in heavily interrupted cuts. |
★ Recommended grade for this chipbreaker. CVD = chemical vapour deposition coating. ISO P = steels.
Recommended cutting data
Heavy external turning of steels (ISO P) – GX chipbreaker
Recommended cutting data by material and cutting condition.
| Material | Condition | Vc (m/min) by grade | fn (mm/rev) | ap (mm) |
|---|---|---|---|---|
| Steels ≤ 280 HB (S235, C45, 41Cr4, 42CrMo4…) |
Stable | IT8115: 135 – 220 IT8125: 80 – 140 IT8225: 80 – 160 |
0.40 – 1.20 | 4.50 – 13.00 |
| Steels ≤ 280 HB (S235, C45, 41Cr4, 42CrMo4…) |
Average | IT8115: 100 – 180 IT8125: 100 – 160 IT8225: 115 – 170 |
0.40 – 1.15 | 4.50 – 13.00 |
| Steels ≤ 280 HB (S235, C45, 41Cr4, 42CrMo4…) |
Difficult | IT8115: 60 – 180 IT8125: 60 – 160 IT8225: 60 – 170 |
0.40 – 1.10 | 4.50 – 13.00 |
| Quenched and tempered steels ≥ 280 HB | Stable | IT8115: 120 – 220 IT8225: 120 – 210 |
0.70 – 1.30 | 4.00 – 12.00 |
| Quenched and tempered steels ≥ 280 HB | Average | IT8115: 80 – 220 IT8225: 80 – 210 |
0.70 – 1.25 | 4.00 – 12.00 |
Guide values. IT8135 is the grade for heavy impacts and heavily interrupted cuts: cutting data on request.
Heavy internal turning (boring) of steels (ISO P) – GX chipbreaker
Starting values for internal turning with a boring bar, derived from this insert's external turning data: cutting speed −15%, feed −20%, maximum depth of cut −40%. Negative inserts are mounted on boring bars for bores from about Ø 25 mm upwards (Ø 32–40 mm for the larger sizes). Heavy roughing needs rigid boring bars in large bores, indicatively above Ø 60 mm.
| Material | Condition | Vc (m/min) by grade | fn (mm/rev) | ap (mm) |
|---|---|---|---|---|
| Steels ≤ 280 HB (S235, C45, 41Cr4, 42CrMo4…) |
Stable | IT8115: 115 – 185 IT8125: 70 – 120 IT8225: 70 – 135 |
0.32 – 0.96 | 4.50 – 7.80 |
| Steels ≤ 280 HB (S235, C45, 41Cr4, 42CrMo4…) |
Average | IT8115: 85 – 155 IT8125: 85 – 135 IT8225: 100 – 145 |
0.32 – 0.92 | 4.50 – 7.80 |
| Steels ≤ 280 HB (S235, C45, 41Cr4, 42CrMo4…) |
Difficult | IT8115: 50 – 155 IT8125: 50 – 135 IT8225: 50 – 145 |
0.32 – 0.88 | 4.50 – 7.80 |
| Quenched and tempered steels ≥ 280 HB | Stable | IT8115: 100 – 185 IT8225: 100 – 180 |
0.56 – 1.04 | 4.00 – 7.20 |
| Quenched and tempered steels ≥ 280 HB | Average | IT8115: 70 – 185 IT8225: 70 – 180 |
0.56 – 1.00 | 4.00 – 7.20 |
With a boring bar overhang above 3 times the diameter (steel bar) or 5 times (carbide or anti-vibration bar), reduce speed and feed further. Use the bar's internal coolant to clear the chips.
You may also like
CNMG cast iron
CNMG-GR
DNMG-BF
DNMG-HQ
DNMG-BM
Recently viewed
SNMM-GX
SNMM-GZ
CNMG cast iron
RCKT-FM
CNMG-HQ






