
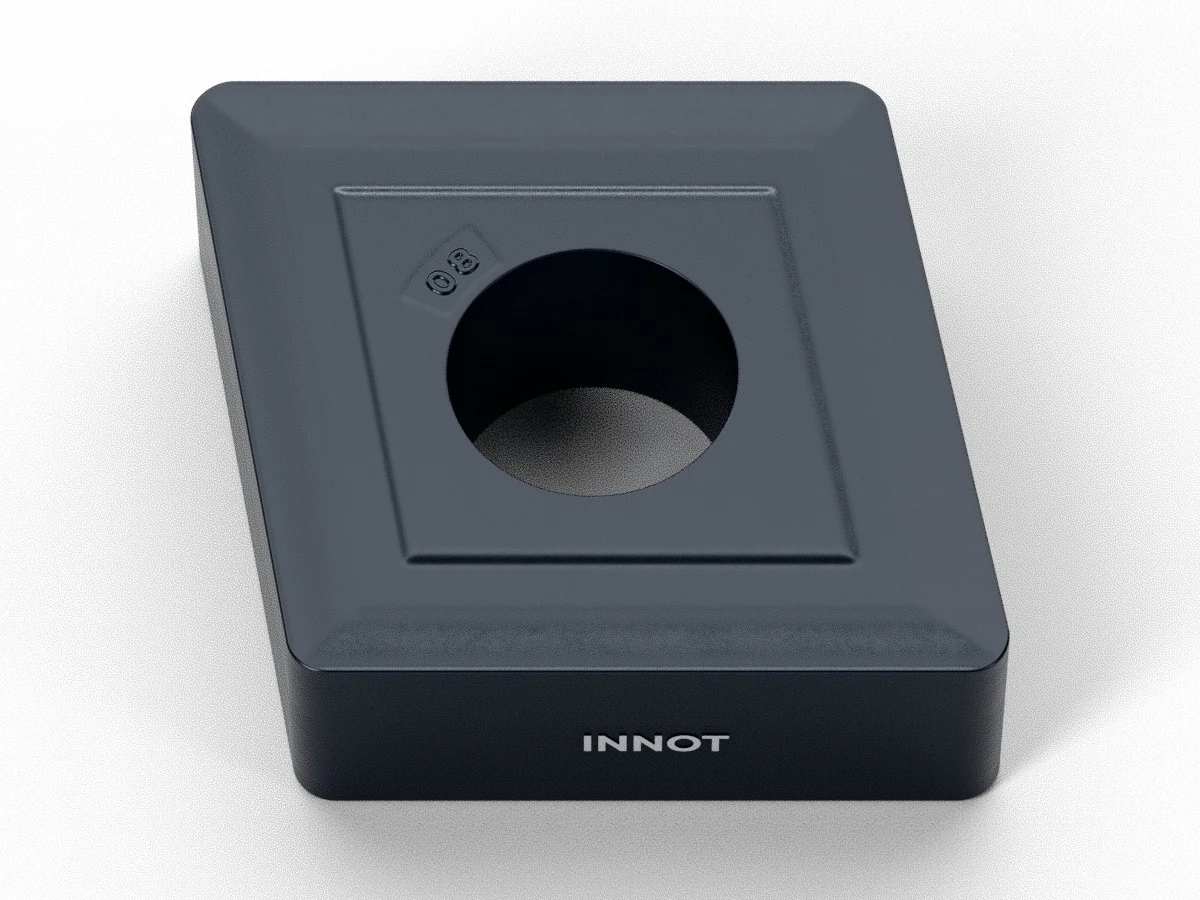
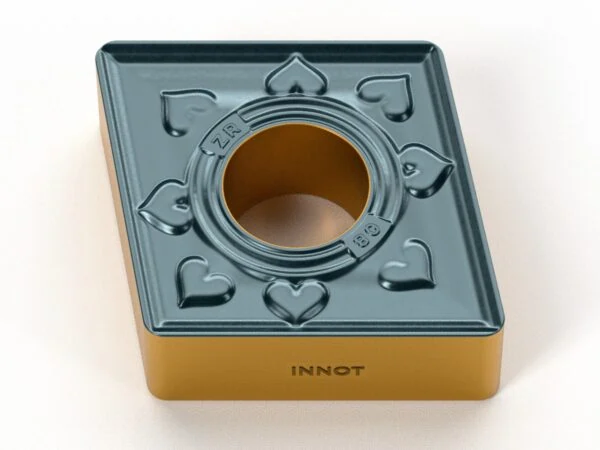
CNMG cast iron
80° negative insert for turning cast iron, with universal double-sided chipbreaker and CVD grade IT6115.
Medium – roughing
CVD
★ IT6115
Technical data sheet PDFCutting data, sizes and grades
Want to try it first? Request a free tester

Description
ISO specifications
| ISO | RADIUS (RE) | AVAILABLE GRADES | CHIPBREAKER |
|---|---|---|---|
| CNMG1204 | 0.4 – 0.8 – 1.2 – 1.6 | IT6115 | Universal cast iron |
| CNMG1606 | 0.8 – 1.2 – 1.6 | IT6115 | Universal cast iron |
| CNMG1906 | 1.2 – 1.6 | IT6115 | Universal cast iron |
Universal cast iron chipbreaker data sheet
| Operation | Medium – roughing |
| ISO material | K (grey cast iron) |
| Tolerance | M |
| Features | Universal chipbreaker for machining ISO K materials. Double-sided insert, particularly suitable for turning grey cast iron, with a wide application range. |
Available INNOT grades
| Grade | ISO | Coating | Composition | Application |
|---|---|---|---|---|
| IT6115 ★ | K | CVD | TiN + MT-TiCN + Al₂O₃ | First-choice grade for turning cast iron. Thicker black CVD coating with special post-coating treatment: excellent wear resistance and toughness. Also suitable for roughing high-strength steels. |
★ Recommended grade for this chipbreaker. CVD = chemical vapour deposition coating. ISO K = cast irons.
Recommended cutting data
External turning of cast iron (ISO K)
Recommended cutting data for grey cast iron, strength ≤ 350 MPa.
| Material | Condition | Vc (m/min) by grade | fn (mm/rev) | ap (mm) |
|---|---|---|---|---|
| Grey cast iron (GG20, GG30 – EN-GJL-200, EN-GJL-300) |
Stable | IT6115: 165 – 300 | 0.25 – 0.60 | 1.60 – 5.00 |
| Grey cast iron (GG20, GG30 – EN-GJL-200, EN-GJL-300) |
Average | IT6115: 165 – 300 | 0.25 – 0.55 | 1.60 – 5.00 |
| Grey cast iron (GG20, GG30 – EN-GJL-200, EN-GJL-300) |
Difficult | IT6115: 165 – 300 | 0.25 – 0.50 | 1.60 – 5.00 |
Guide values. IT6115 can also be used for roughing high-strength steels.
Internal turning (boring) of cast iron (ISO K)
Starting values for internal turning with a boring bar, derived from this insert's external turning data: cutting speed −15%, feed −20%, maximum depth of cut −40%. Negative inserts are mounted on boring bars for bores from about Ø 25 mm upwards (Ø 32–40 mm for the larger sizes).
| Material | Condition | Vc (m/min) by grade | fn (mm/rev) | ap (mm) |
|---|---|---|---|---|
| Grey cast iron (GG20, GG30 – EN-GJL-200, EN-GJL-300) |
Stable | IT6115: 140 – 255 | 0.20 – 0.48 | 1.60 – 3.00 |
| Grey cast iron (GG20, GG30 – EN-GJL-200, EN-GJL-300) |
Average | IT6115: 140 – 255 | 0.20 – 0.44 | 1.60 – 3.00 |
| Grey cast iron (GG20, GG30 – EN-GJL-200, EN-GJL-300) |
Difficult | IT6115: 140 – 255 | 0.20 – 0.40 | 1.60 – 3.00 |
With a boring bar overhang above 3 times the diameter (steel bar) or 5 times (carbide or anti-vibration bar), reduce speed and feed further. Use the bar's internal coolant to clear the chips.
You may also like
Recently viewed
CNMG-ZR






