
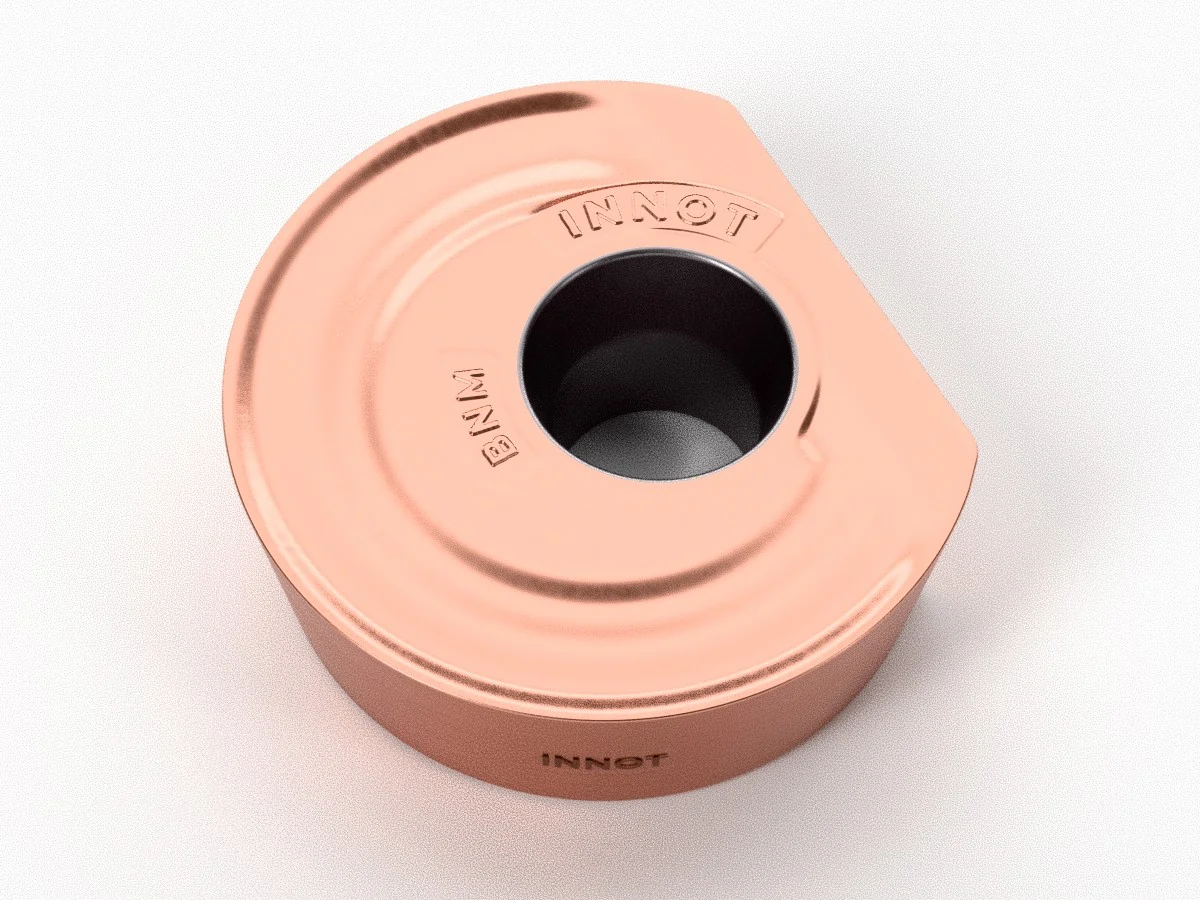
BNM (ball nose)
Ball nose insert for copy milling cutters, from Ø12 to Ø32 mm, for finishing moulds and 3D surfaces.
ISO P
ISO M
ISO K
ISO H
Copy milling and profiling
Finishing
★ IT5210
Technical data sheet PDFCutting data, sizes and grades
Want to try it first? Request a free tester
Fits on

Description
Specifications
| Code | Ø (W1) | S | D1 | RE | APMX |
|---|---|---|---|---|---|
| BNM1203-S | 12 | 3 | 3.5 | 6 | 6 |
| BNM1604-S | 16 | 4 | 4 | 8 | 8 |
| BNM2005-S | 20 | 5 | 5 | 10 | 10 |
| BNM2506-S | 25 | 6 | 6 | 12.5 | 12.5 |
| BNM3007-S | 30 | 7 | 8 | 15 | 15 |
| BNM3207-S | 32 | 7 | 8 | 16 | 16 |
| BNM2005 | 20 | 5 | 5 | 10 | 10 |
| BNM2506 | 25 | 6 | 6 | 12.5 | 12.5 |
| BNM3007 | 30 | 7 | 8 | 15 | 15 |
| BNM3207 | 32 | 7 | 8 | 16 | 16 |
Dimensions in mm. IC = inscribed circle, S = thickness, D1 = hole, BS = wiper flat, RE = corner radius, AN = clearance angle, APMX = maximum depth of cut.
Technical data
| Operation | Milling – Copy milling and profiling |
| Shape | Ball nose |
| ISO material | P (steels), M (stainless steels), K (cast irons), H (hardened steels) |
| Features | Full-radius insert for ball nose cutters: 3D profiles, moulds and free-form surfaces. -S version with chipbreaker. |
| Compatible cutters | Indexable cutters with BNM seat: send us your cutter code and we will check compatibility. |
Available INNOT grades
| Grade | ISO | Coating | Composition | Application |
|---|---|---|---|---|
| IT5210 ★ | P · H | PVD | AlTiN + TiSiN | Milling of hardened steels 50–65 HRC. Coating with high thermal stability and oxidation resistance: withstands the most severe cutting temperatures. |
| IT5220 | P · M · K | PVD | AlTiN + TiSiN | Universal grade for steels, stainless steels and cast irons up to 40–50 HRC. Double-layer coating: strength, toughness and protection against edge chipping. |
| IT5130 | P · M | PVD | AlTiN | High-efficiency milling of steels and stainless steels below 30 HRC. Specially formulated substrate that reduces the risk of chipping, with a latest-generation nano coating. |
★ Recommended grade. Other grades are available on request.
Cutting data and tips for use
Preferably climb mill with the tool tilted by 10–15° to avoid cutting with the insert centre (zero speed).
You may also like
SZMX
Available
HHardenedPSteelKCast ironMStainlessFace milling · Roughing
ODMT / ODKT
Available
HHardenedPSteelKCast ironMStainlessFace milling
SDKT-SM
Available
PSteelKCast ironMStainlessSSuperalloysRoughing
RPMT-HM / RPMW
Available
HHardenedPSteelKCast ironMStainlessSSuperalloysSemi-finishing · Roughing
SNGX-ZNN / SNMX
Available
HHardenedPSteelKCast ironMStainlessFace milling · Semi-finishing






