Need help? Call us: (+39) 3757861361 or info@innot-it.com
Indexable drills
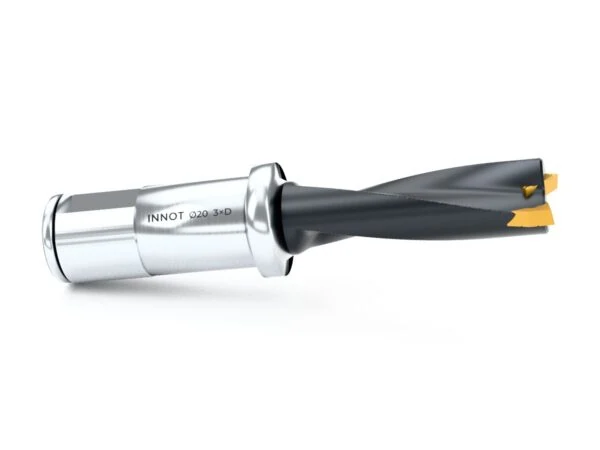
Indexable insert drills from Ø16 to Ø60 mm, from 2 to 5 times the diameter: one body, economical inserts.
Drill body with indexable inserts for holes from Ø16 to Ø60 mm: when the insert wears, you only change the insert.
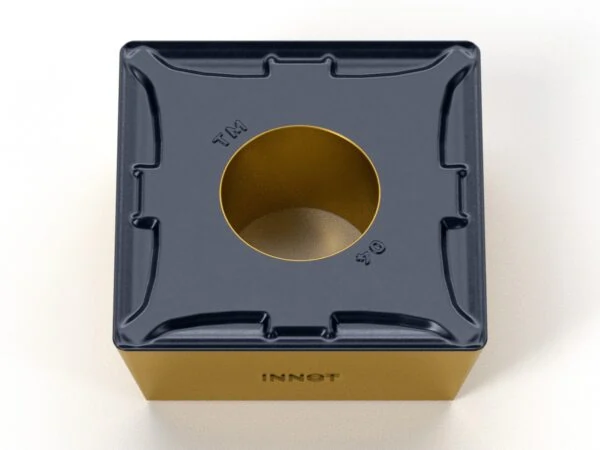
Indexable inserts for indexable drills: 4-edge WCMX with chipbreaker for drilling and SPMG for larger diameters.
Indexable drills
INNOT indexable drills cover holes from Ø16 to Ø60 mm with depths from 2×D to 5×D. They carry interchangeable WCMX inserts with 4 edges or SPMG inserts: when the edge is worn you change the insert while the drill body stays on the machine.
They are the most economical solution for large-diameter holes in series production.
Categories
- Turning Inserts (121)
- Negative inserts (84)
- CNMG / CNMA - 80° rhombic (16)
- DNMG - 55° rhombic (13)
- SNMG - 90° square (15)
- TNMG - 60° triangular (14)
- VNMG - 35° rhombic (12)
- WNMG - 80° trigon (14)
- Positive inserts (23)
- CCMT - 80° rhombic (4)
- DCMT - 55° rhombic (4)
- SCMT - 90° square (2)
- TCMT - 60° triangular (4)
- VBMT / VCMT - 35° rhombic (7)
- RCMX - Round (2)
- Parting and grooving (7)
- Negative inserts (84)
- Milling Inserts (24)
- Face milling (8)
- 90° square shoulder (5)
- High feed (3)
- Copy milling and profiling (7)
- Helical cutters (1)
- Solid Carbide End Mills (14)
- Drills (9)
- Solid carbide drills (7)
- Indexable drills (2)
- Threading (19)
- Threading inserts (7)
- Taps (12)
- Through hole taps (5)
- Blind hole taps (5)
- Forming taps (1)
- Special and custom threads (2)
- Toolholders and Chucks (15)
Recently viewed
Full-profile inserts for ISO 60° metric threads: crest and root formed by the insert, finished thread without deburring.
Toolholders for 93° profiling: the narrow tip of 55° and 35° inserts reaches grooves, fillets and undercut profiles.
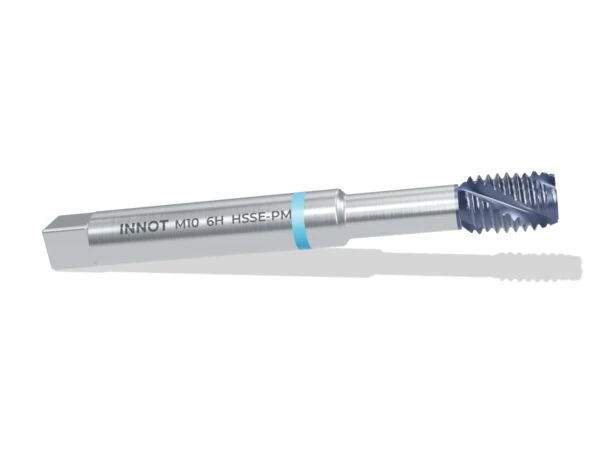
40° right-hand spiral flute tap for blind holes in quenched and tempered and alloy steels: the chip flows back towards the shank. TiCN, 10 – 12° rake.
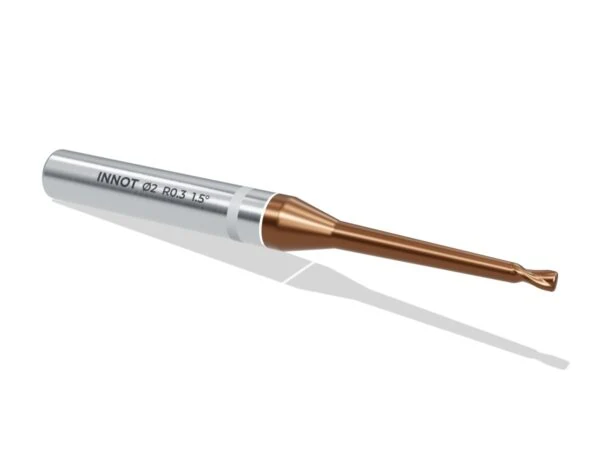
Torus end mill with reinforced tapered neck: the neck follows the draft angle of the walls, is more rigid and vibrates less in deep mould machining, up to 65 HRC.

Inserts and cutting tools for CNC machine shops. Dedicated grades for every ISO group, from steel to aluminium, from superalloys to hardened steels, with cutting data in every product sheet.
INNOT by Giammarco Turati
Via San Ponso, 57 – 10080 Pertusio (TO)
VAT No. IT13269100015
© 2026 INNOT by Giammarco Turati – VAT No. IT13269100015 – Pertusio (TO), Italy – Privacy Policy – Cookie Policy