Need help? Call us: (+39) 3757861361 or info@innot-it.com
Toolholders and Chucks
Turning and milling toolholders chosen by operation: toolholders, boring bars, blades, indexable cutters and chucks for INNOT inserts. Tell us machine and connection: we propose the right tool.
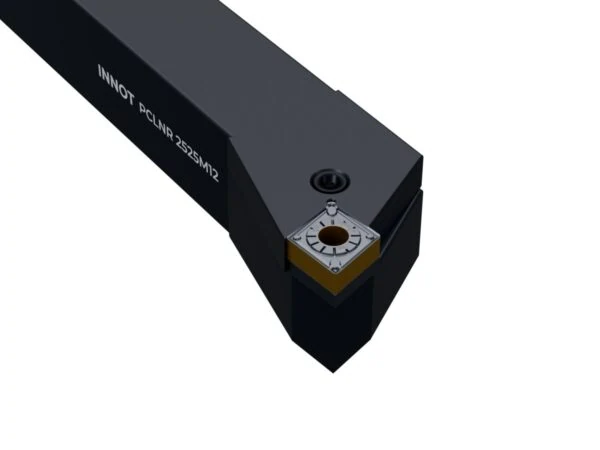
Toolholders for 95° external turning: the same tool turns longitudinally and faces. Lever or clamp locking for negative inserts, screw clamping for positive inserts.
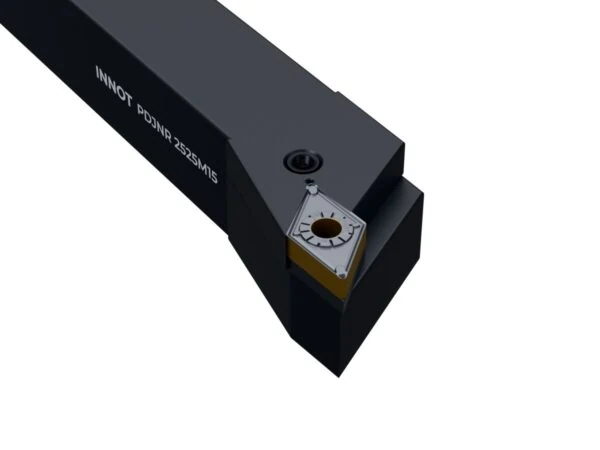
Toolholders for 93° profiling: the narrow tip of 55° and 35° inserts reaches grooves, fillets and undercut profiles.
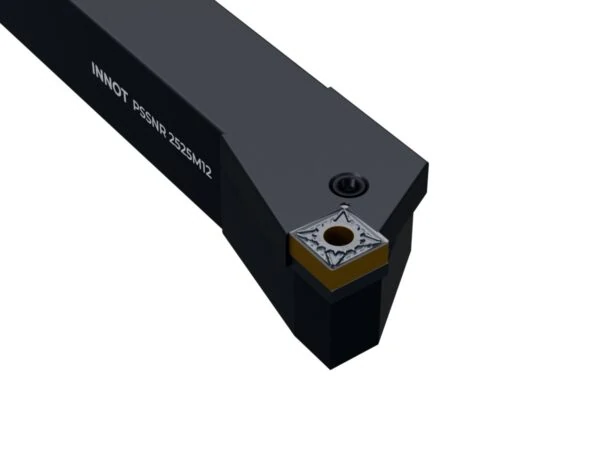
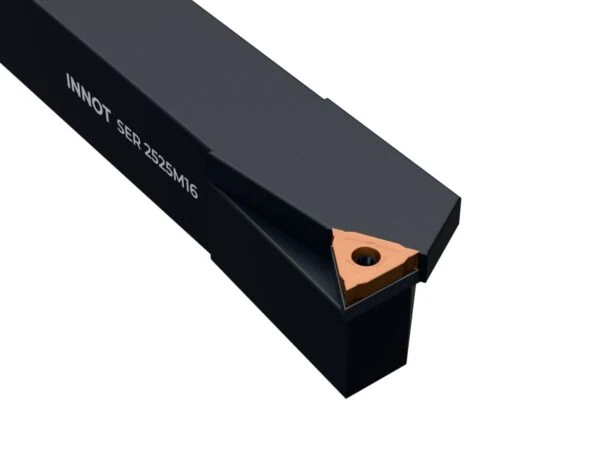
Toolholders with 45° or 75° lead angle for square and triangular inserts: the chip gets thinner and the cutting edge withstands deep cuts.
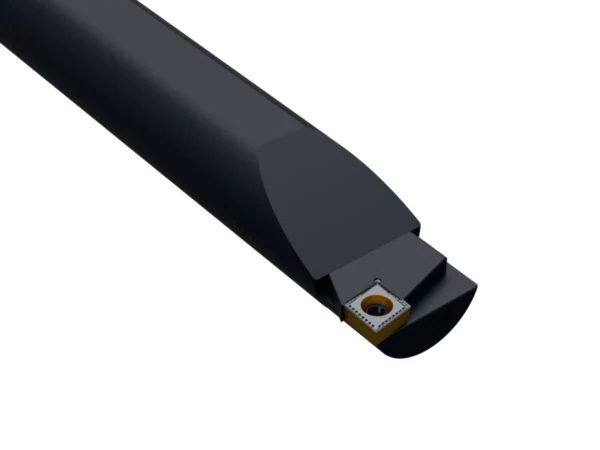
Steel or carbide boring bars, with internal coolant supply, for turning bores from small to large diameter.
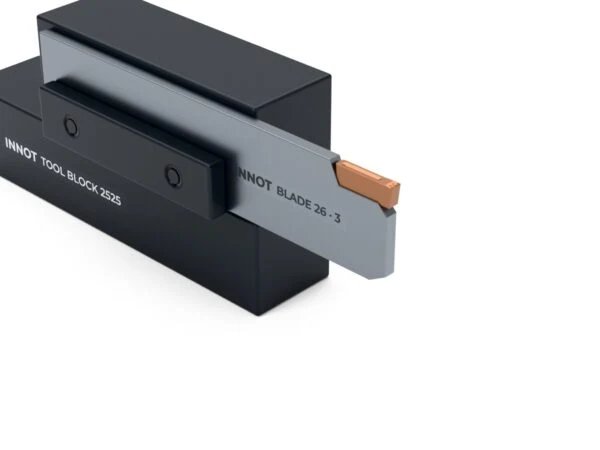
Blades and blocks for single- and double-ended inserts: bar parting, external grooving and side turning with the same blade.
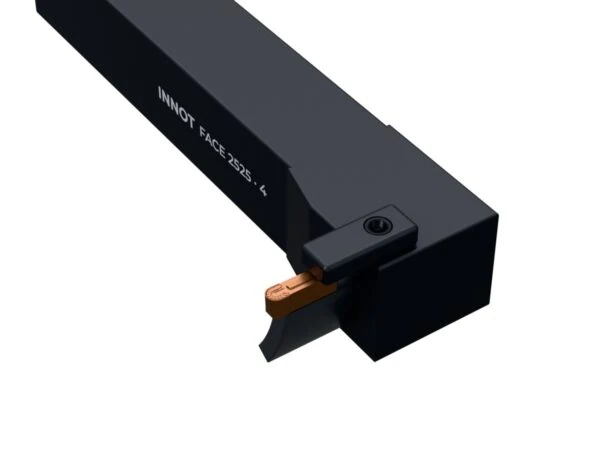
Curved toolholders for face grooving: the curvature follows the groove diameter to machine axially without rubbing.
Threading toolholders
Toolholders and boring bars for partial or full profile threading inserts: metric, pipe, UN and trapezoidal.
Face mills
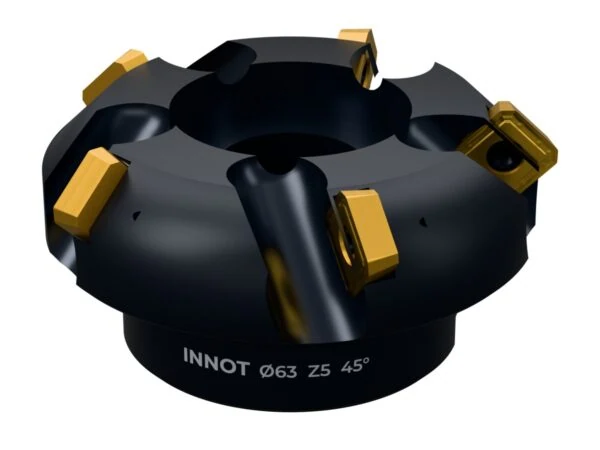
Indexable face mills, 45° or with double-sided inserts, for flat surfaces with high productivity and a good finish.
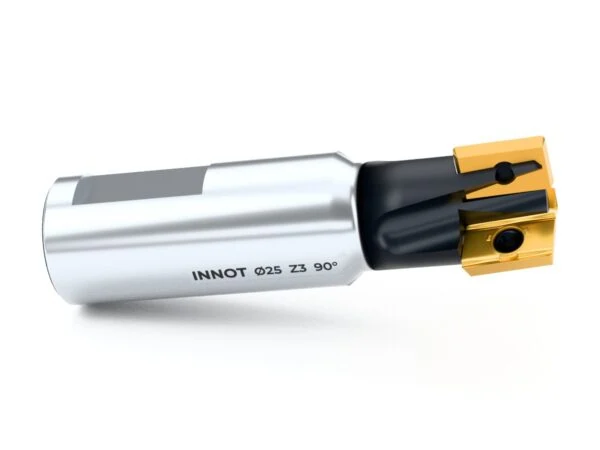
End mills and shell mills for 90° shoulders, slots and contouring, with positive or tangential inserts.
High-feed cutters
High-feed cutters: light cuts and very high feed per tooth to rough moulds and pockets in the shortest time.
Copy milling cutters
Copy milling cutters for round and ball nose inserts: 3D surfaces, moulds and complex profiles.
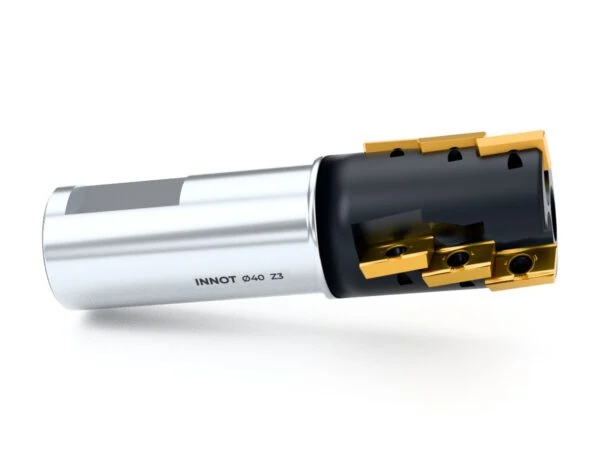
Helical cutters with several rows of inserts: a continuous flank for very deep shoulders and large chip volumes.
Chucks and adapters
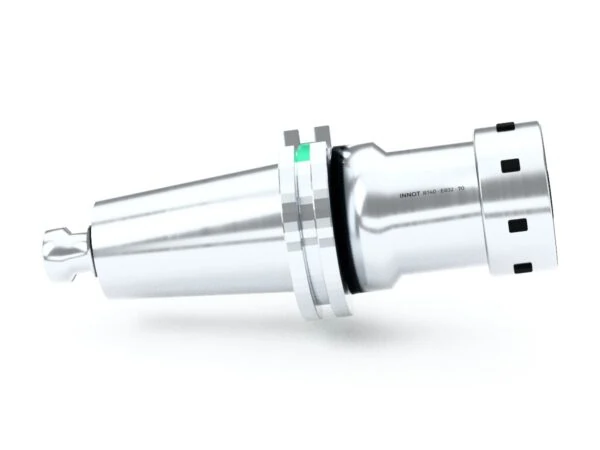
BT, HSK and DIN tapers with ER collets, shell mill holders and hydraulic or shrink-fit chucks to connect cutter and spindle.
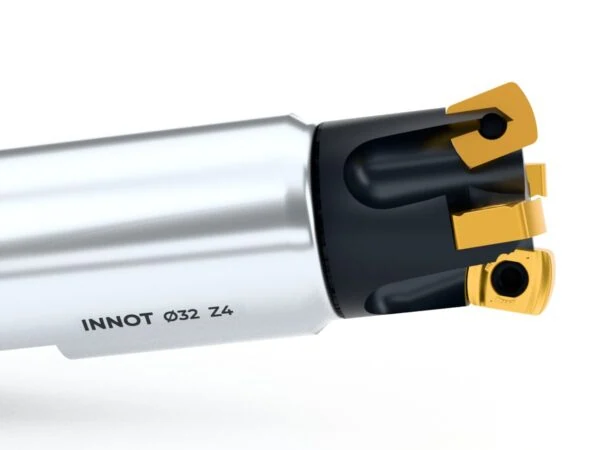
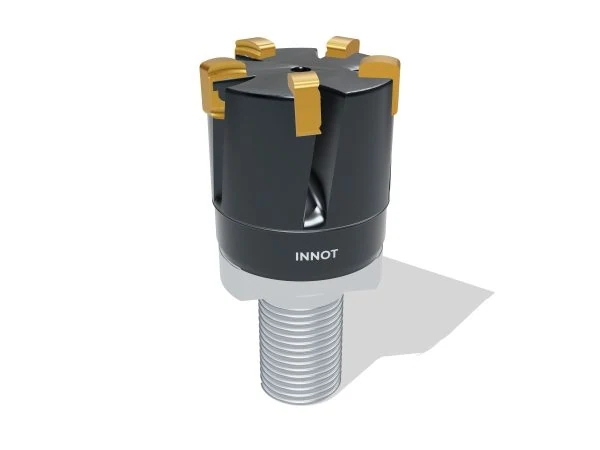
High-feed modular heads from Ø10 to Ø42 mm, 2 to 8 cutting edges, M6–M16 connection, for BLMP inserts.
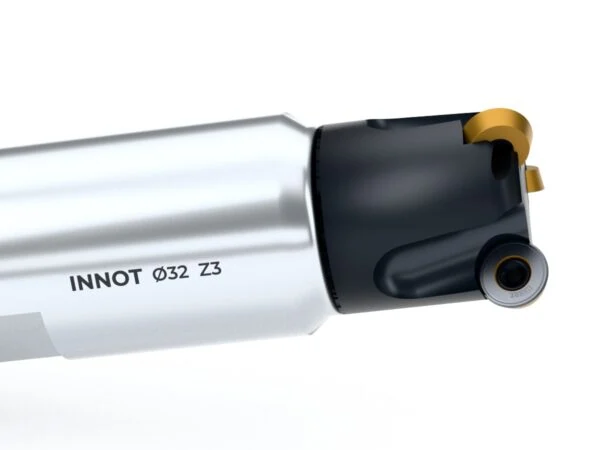
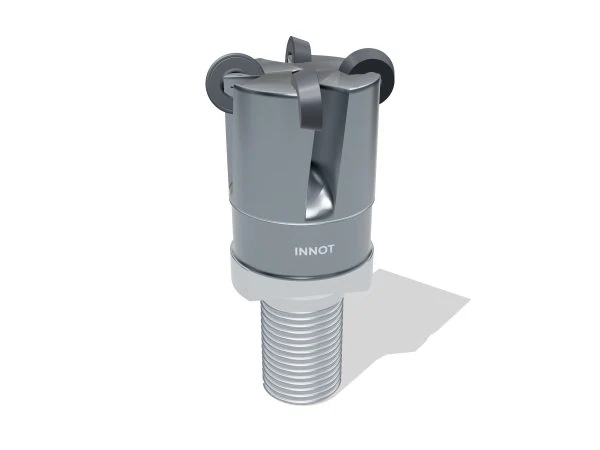
Copy milling modular heads from Ø10 to Ø42 mm, 2 to 5 cutting edges, M6–M16 connection, for RDHX round inserts.
Turning toolholders, indexable milling cutters and chucks
Here you will find the toolholders for INNOT inserts: 95° external turning holders, 93° profiling and 45° and 75° roughing holders, boring bars for internal turning, parting and grooving blades, face grooving holders and threading holders.
For milling there are face mills, 90° shoulder mills, high-feed, copy and helical cutters, BLMP and RDHX modular heads and chucks with BT, HSK and DIN tapers, ER collets, shell mill holders and hydraulic chucks.
How to choose the toolholder
The ISO code of the toolholder shows the insert clamping, the insert shape, the lead angle, the hand (right or left), the shank size and the cutting edge length. Tell us your machine and the insert you want to use and we will propose the right holder.
Categories
- Turning Inserts (121)
- Negative inserts (84)
- CNMG / CNMA - 80° rhombic (16)
- DNMG - 55° rhombic (13)
- SNMG - 90° square (15)
- TNMG - 60° triangular (14)
- VNMG - 35° rhombic (12)
- WNMG - 80° trigon (14)
- Positive inserts (23)
- CCMT - 80° rhombic (4)
- DCMT - 55° rhombic (4)
- SCMT - 90° square (2)
- TCMT - 60° triangular (4)
- VBMT / VCMT - 35° rhombic (7)
- RCMX - Round (2)
- Parting and grooving (7)
- Negative inserts (84)
- Milling Inserts (24)
- Face milling (8)
- 90° square shoulder (5)
- High feed (3)
- Copy milling and profiling (7)
- Helical cutters (1)
- Solid Carbide End Mills (14)
- Drills (9)
- Solid carbide drills (7)
- Indexable drills (2)
- Threading (19)
- Threading inserts (7)
- Taps (12)
- Through hole taps (5)
- Blind hole taps (5)
- Forming taps (1)
- Special and custom threads (2)
- Toolholders and Chucks (15)
Recently viewed
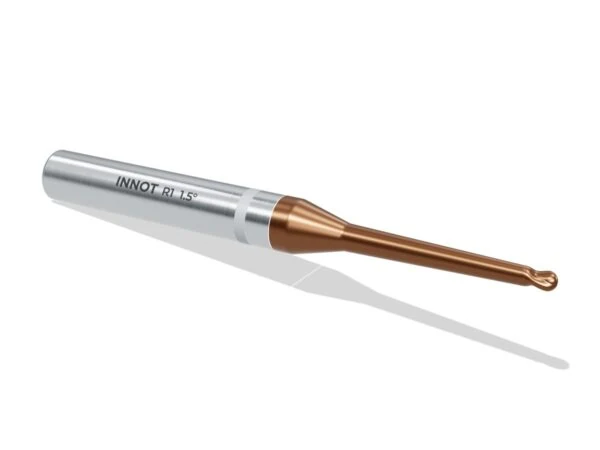
Ball nose end mill with reinforced tapered neck for copy milling and finishing of deep cavities with drafted walls: more rigidity, less vibration, up to 65 HRC.
Full-profile inserts for ISO 60° metric threads: crest and root formed by the insert, finished thread without deburring.
Toolholders for 93° profiling: the narrow tip of 55° and 35° inserts reaches grooves, fillets and undercut profiles.
40° right-hand spiral flute tap for blind holes in quenched and tempered and alloy steels: the chip flows back towards the shank. TiCN, 10 – 12° rake.
Torus end mill with reinforced tapered neck: the neck follows the draft angle of the walls, is more rigid and vibrates less in deep mould machining, up to 65 HRC.

Inserts and cutting tools for CNC machine shops. Dedicated grades for every ISO group, from steel to aluminium, from superalloys to hardened steels, with cutting data in every product sheet.
INNOT by Giammarco Turati
Via San Ponso, 57 – 10080 Pertusio (TO)
VAT No. IT13269100015
© 2026 INNOT by Giammarco Turati – VAT No. IT13269100015 – Pertusio (TO), Italy – Privacy Policy – Cookie Policy