
Turning Inserts
Positive inserts
Positive inserts with clearance angle: smooth cutting and reduced forces. Ideal for finishing, thin parts, boring and low-power lathes.
23inserts
Showing all 23 results
Sort:
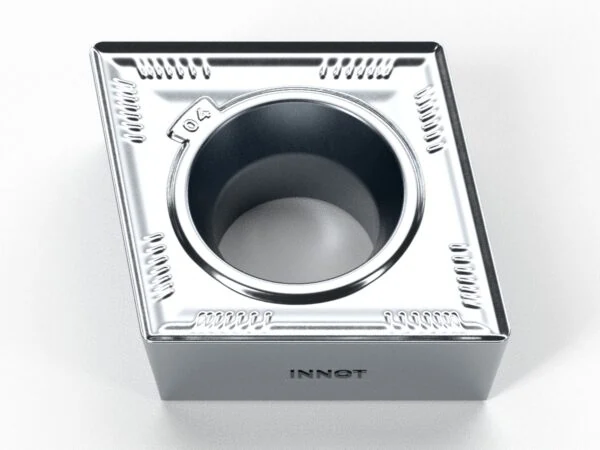
CCGT-AK
Available
NAluminiumFinishing
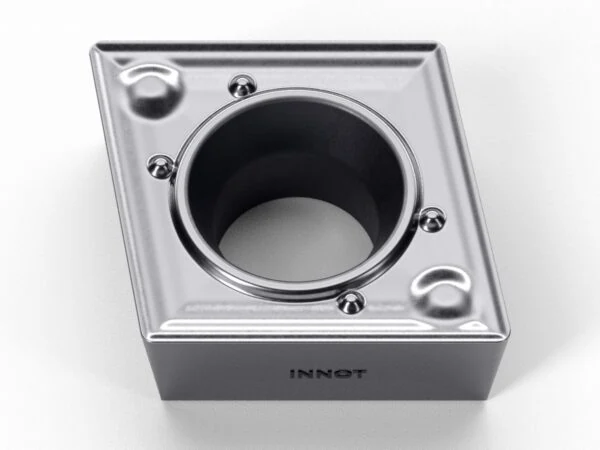
CCMT-HQ
Available
PSteelFinishing · Semi-finishing
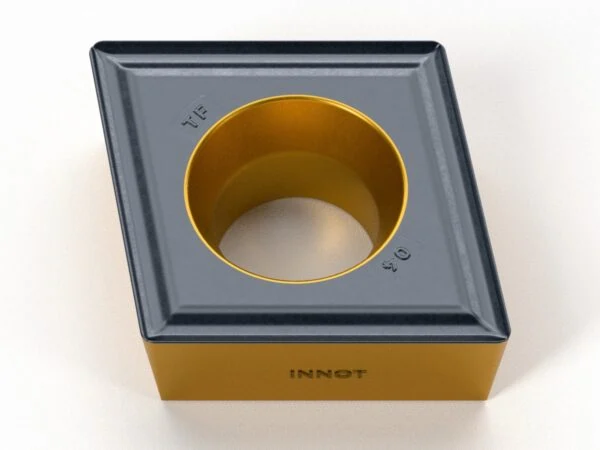
CCMT-TF
Available
PSteelMStainlessSSuperalloysFinishing
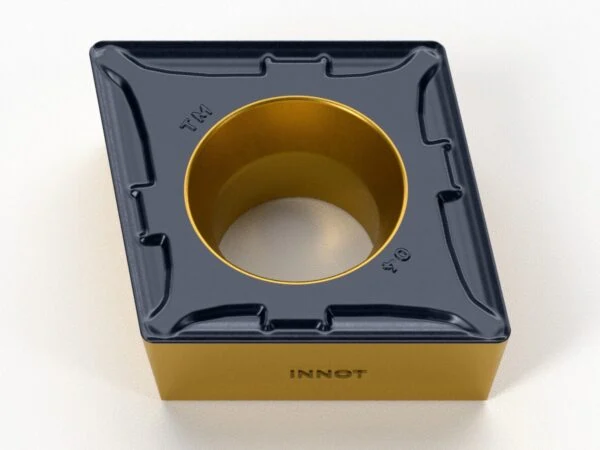
CCMT-TM
Available
PSteelMStainlessSemi-finishing
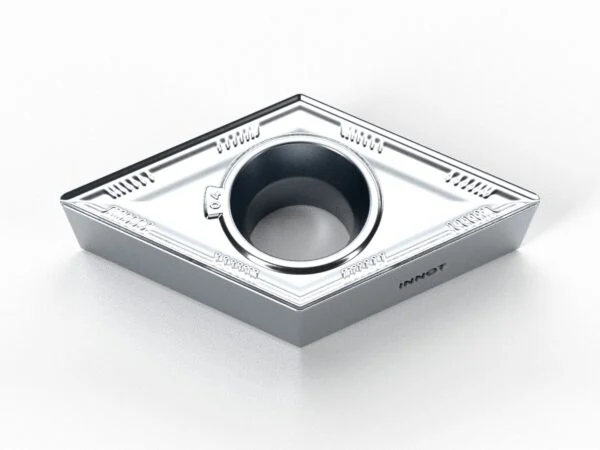
DCGT-AK
Available
NAluminiumFinishing
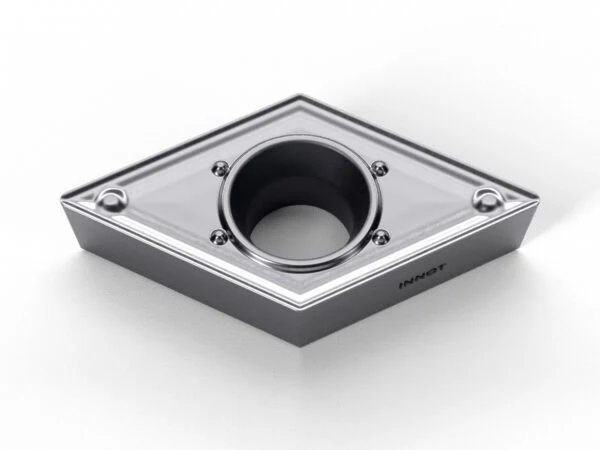
DCMT-HQ
Available
PSteelFinishing · Semi-finishing
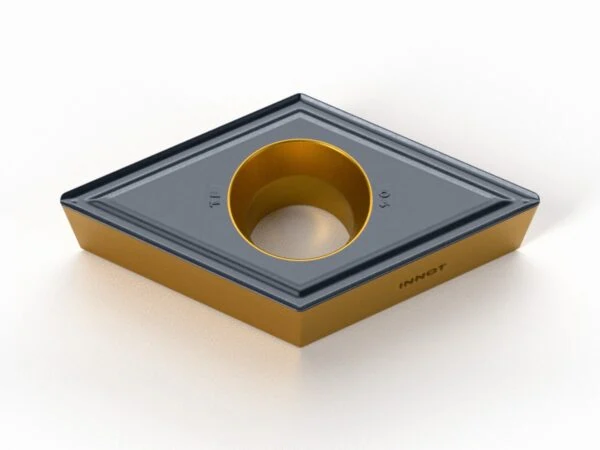
DCMT-TF
Available
PSteelMStainlessSSuperalloysFinishing
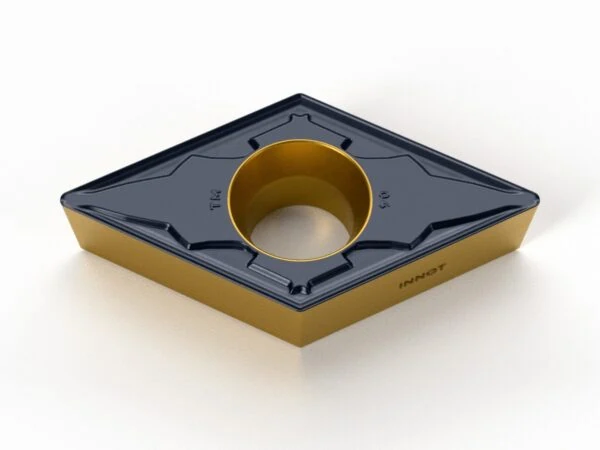
DCMT-TM
Available
PSteelMStainlessSemi-finishing
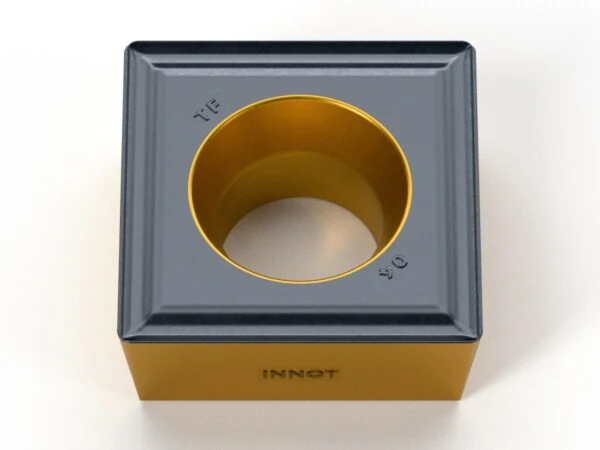
SCMT-TF
Available
PSteelMStainlessSSuperalloysFinishing
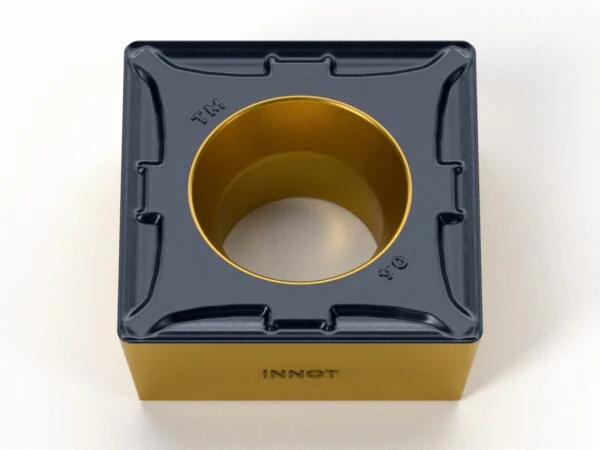
SCMT-TM
Available
PSteelMStainlessSemi-finishing
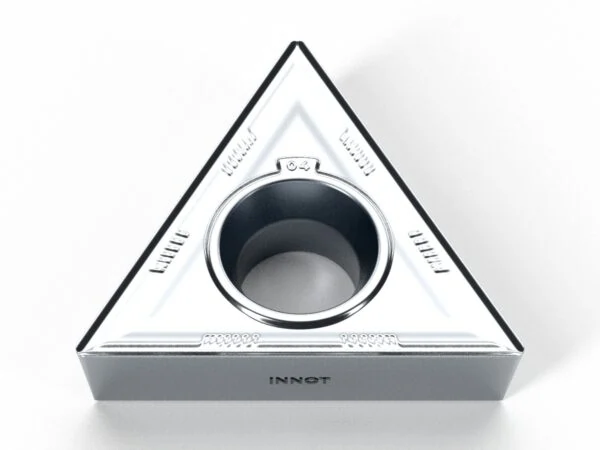
TCGT-AK
Available
NAluminiumFinishing
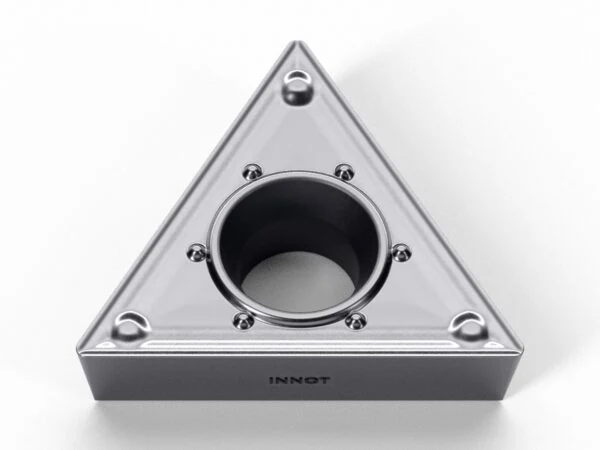
TCMT-HQ
Available
PSteelFinishing · Semi-finishing
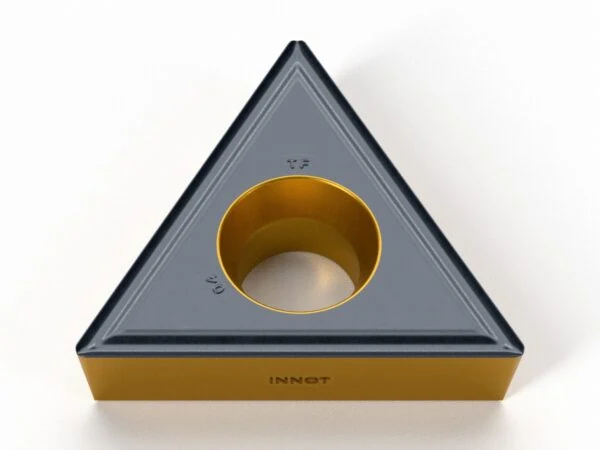
TCMT-TF
Available
PSteelMStainlessSSuperalloysFinishing
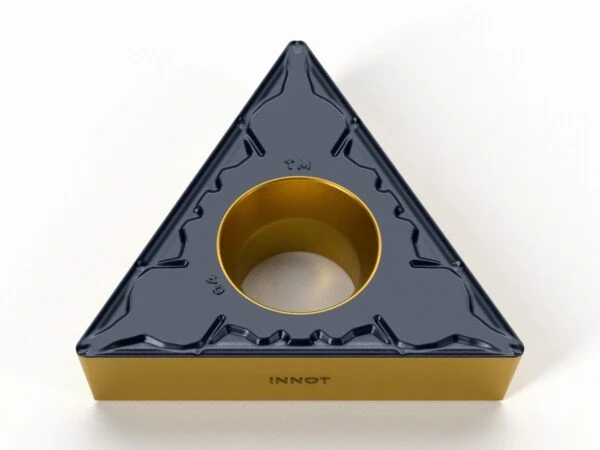
TCMT-TM
Available
PSteelMStainlessSemi-finishing
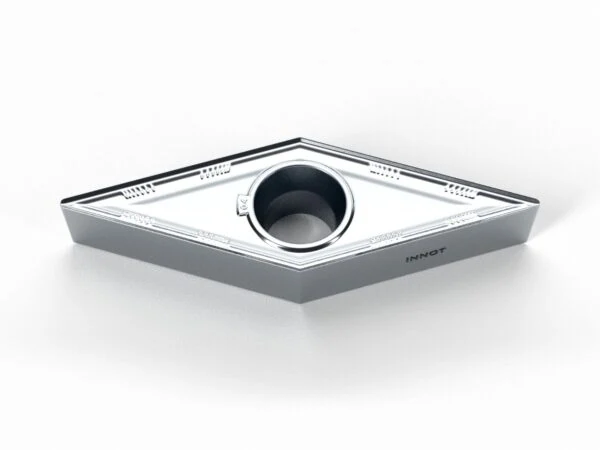
VBGT-AK
Available
NAluminiumFinishing
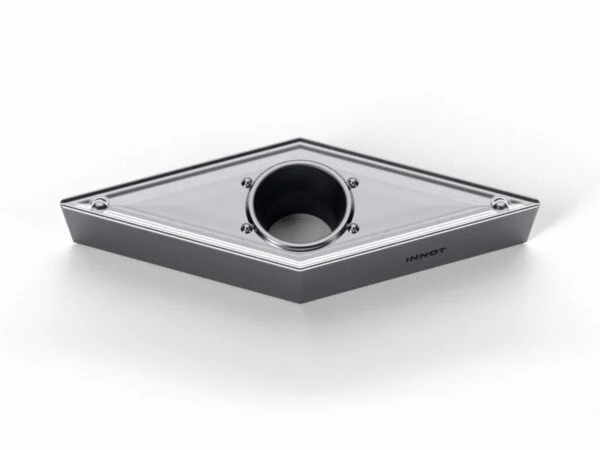
VBMT-HQ
Available
PSteelFinishing · Semi-finishing
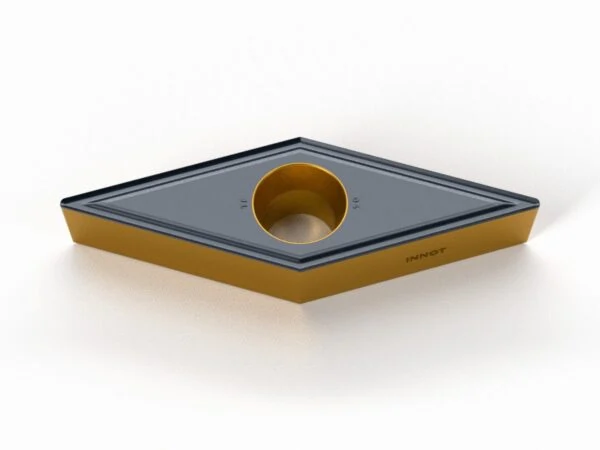
VBMT-TF
Available
PSteelMStainlessSSuperalloysFinishing
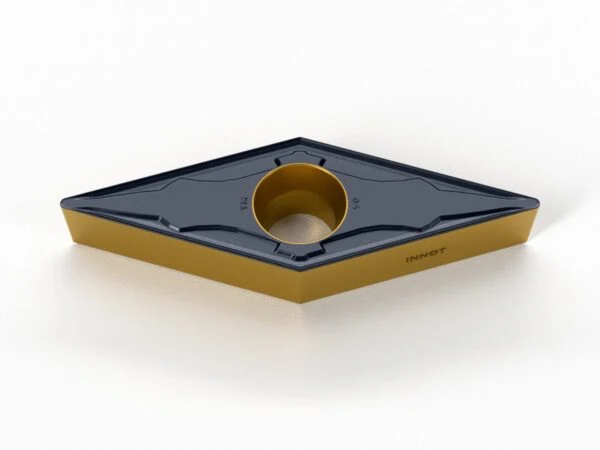
VBMT-TM
Available
PSteelMStainlessSemi-finishing
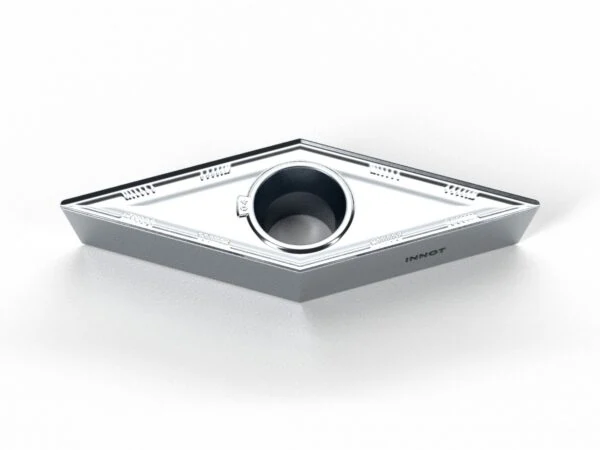
VCGT-AK
Available
NAluminiumFinishing
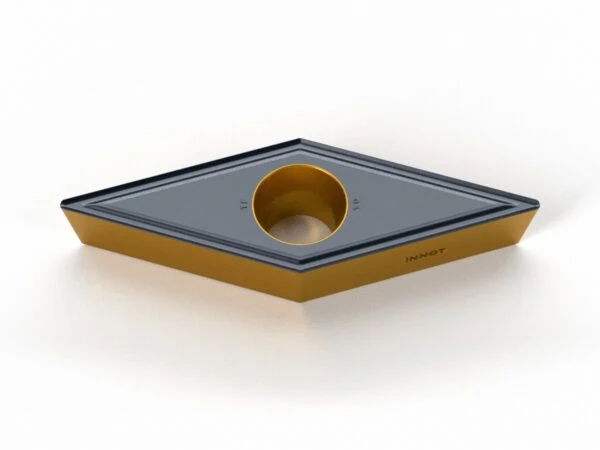
VCMT-TF
Available
PSteelMStainlessSSuperalloysFinishing
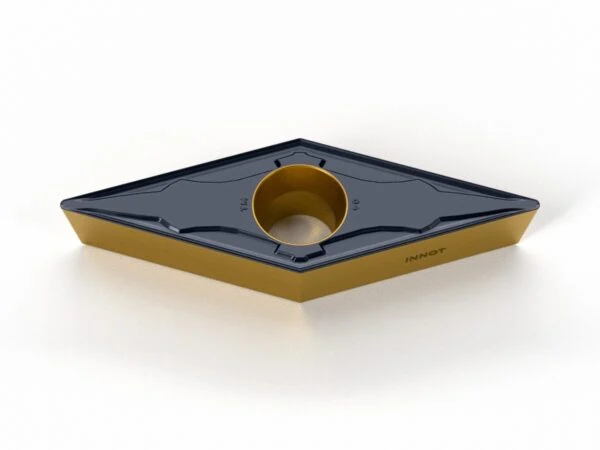
VCMT-TM
Available
PSteelMStainlessSemi-finishing
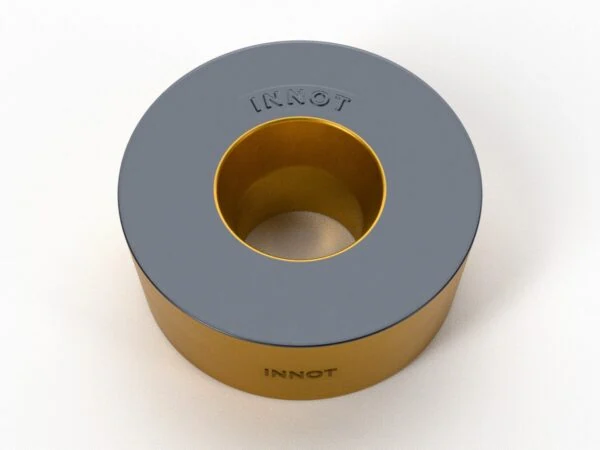
RCMX
Available
PSteelRoughing · Special
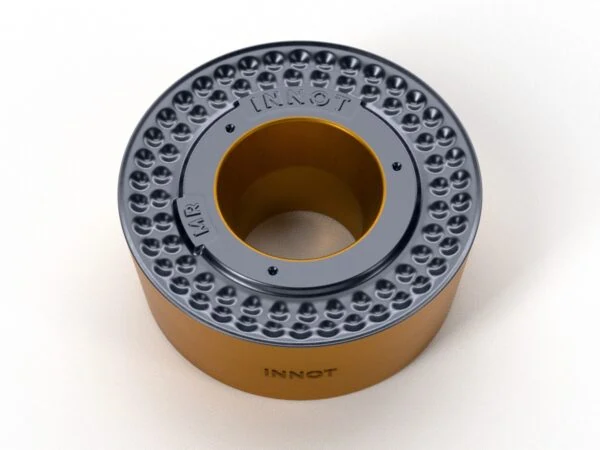
RCMX-MR
Available
PSteelRoughing · Special
INNOT guide
Positive turning inserts for finishing and small diameters
Positive inserts have a 7° (CCMT, DCMT, SCMT, TCMT, VCMT) or 5° (VBMT) clearance and a countersunk hole for the clamping screw. They cut with low forces: they are ideal for finishing, boring and internal turning, thin-walled parts and low-power lathes.
The ground versions CCGT, DCGT, TCGT, VBGT and VCGT have a sharp, polished edge for aluminium and non-ferrous alloys, while the cermet versions give an excellent finish on steels.
Choose the familyCCMT - 80° rhombicDCMT - 55° rhombicSCMT - 90° squareTCMT - 60° triangularVBMT / VCMT - 35° rhombicRCMX - Round
Can't find the size or do you use another brand's code?Send us the code or the drawing: we reply with a quote within 30 minutes.
Recently viewed
PSteel
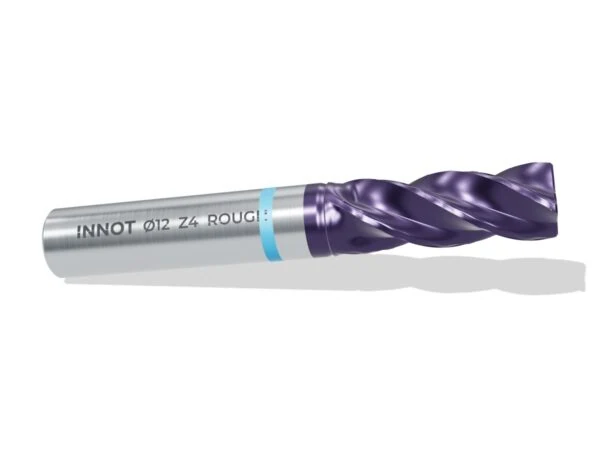
Roughing end mill with wavy cutting edge
Available
PSteelNAluminiumKCast ironRoughing
PSteel
PSteel
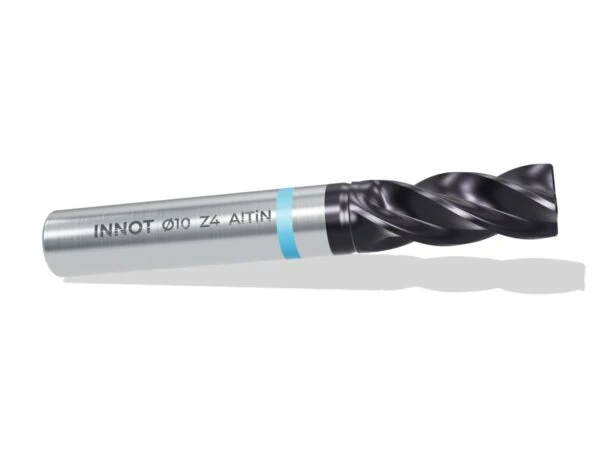
4-flute flat end mill – universal
Available
HHardenedPSteelKCast ironFinishing · Semi-finishing






