Need help? Call us: (+39) 3757861361 or info@innot-it.com
Milling Inserts
INNOT milling inserts: face milling, square shoulder, high feed, copy milling and helical cutters. CVD, PVD and cermet grades for steels, stainless steels, cast irons, superalloys and hardened steels.
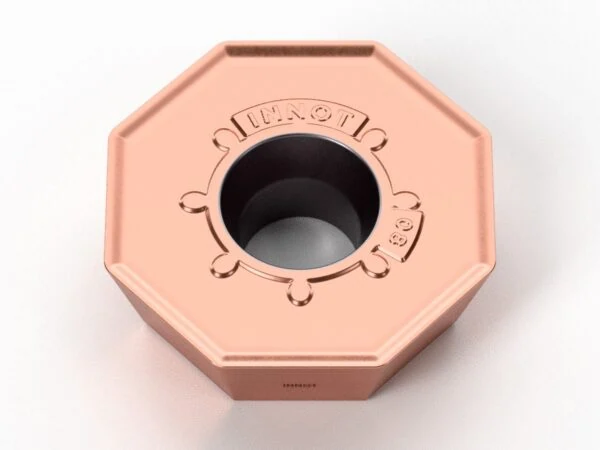
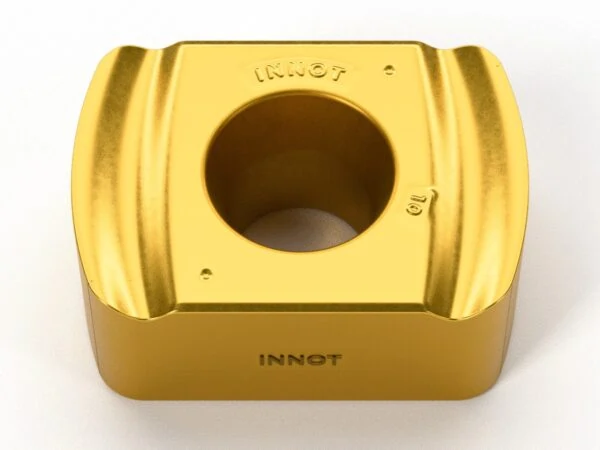
ODMT / ODKT
Octagonal face milling insert with 16 usable cutting edges (8 per side): very low cost per edge and great stability.
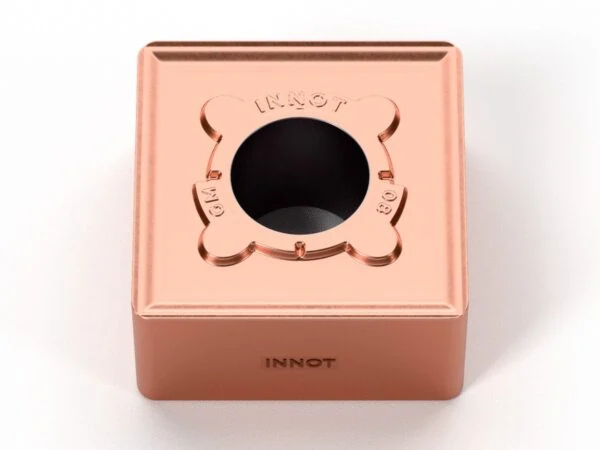
SNGX-GM / SNGX-GE
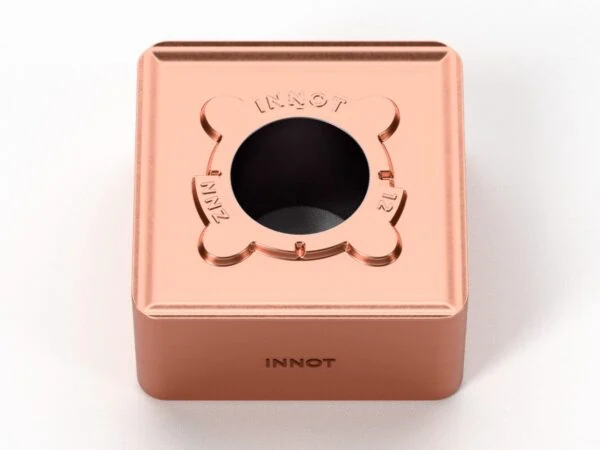
Double-sided square insert for face milling: 8 cutting edges per insert, universal GM geometry and GE for cast irons and interrupted cuts.
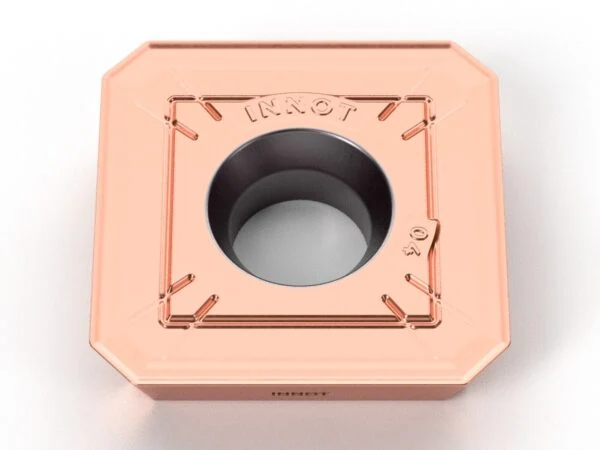
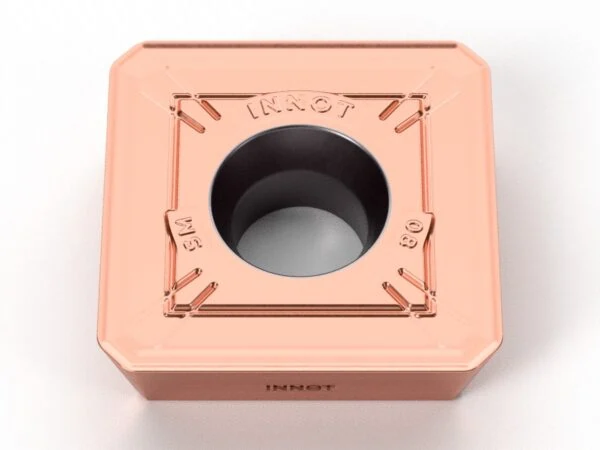
SEET / SEMT
Square insert for 45° face milling, with universal GM chipbreaker and FM for finishing.
SEKR / SEMR / SEEN
45° square insert for face milling: SEKR/SEMR in coated carbide, SEEN in cermet for finishing steels.
HNMX / HNGX
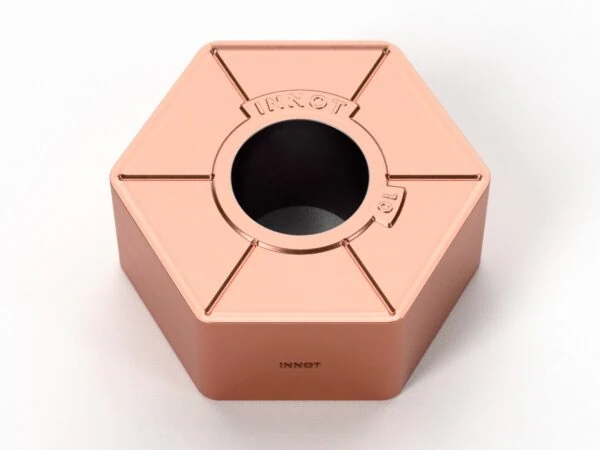
Double-sided hexagonal insert for face milling: 12 cutting edges, F (finishing), M (medium) and R (roughing) geometries.
XNMX / XNGX
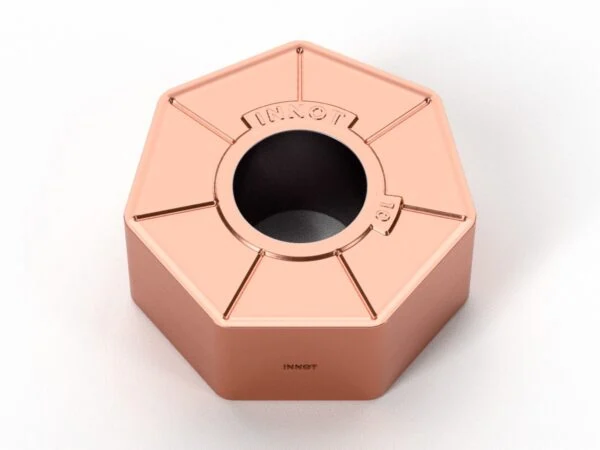
Double-sided heptagonal insert for face milling: 14 cutting edges, with dedicated W wipers for mirror finishing.
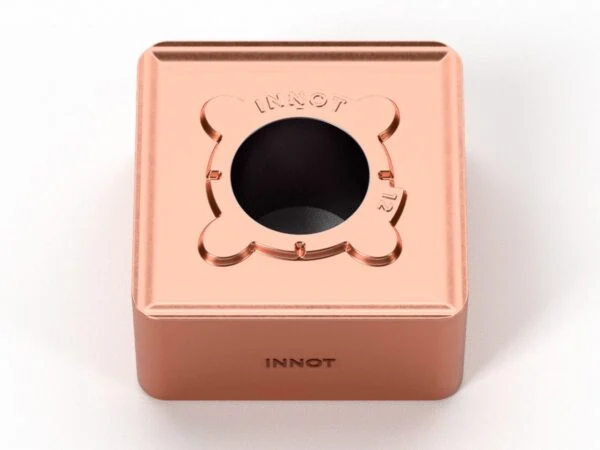
SNGX-ZNN / SNMX
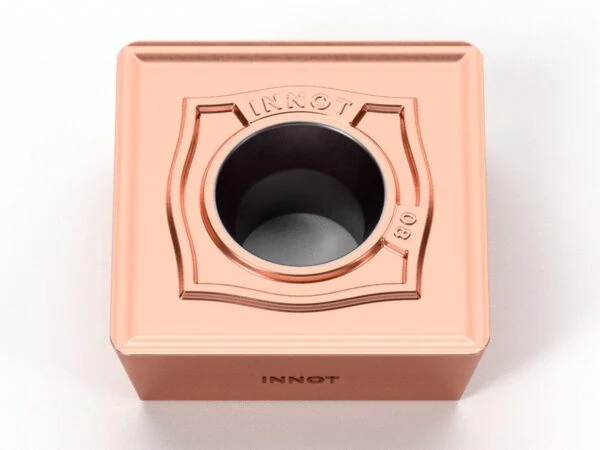
Double-sided square insert for face and shoulder milling with APMX up to 8 mm.
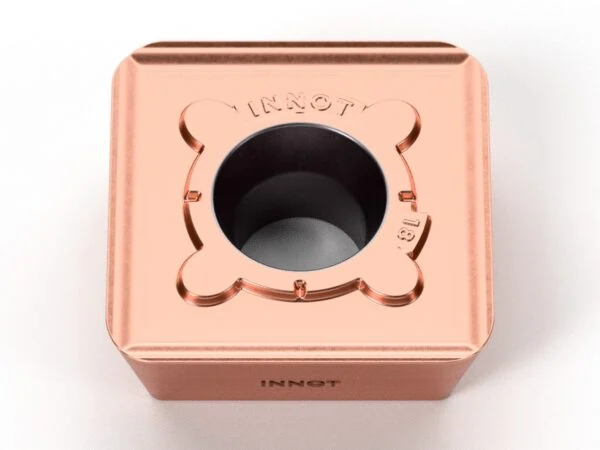
APMT-HM / APGT-AK
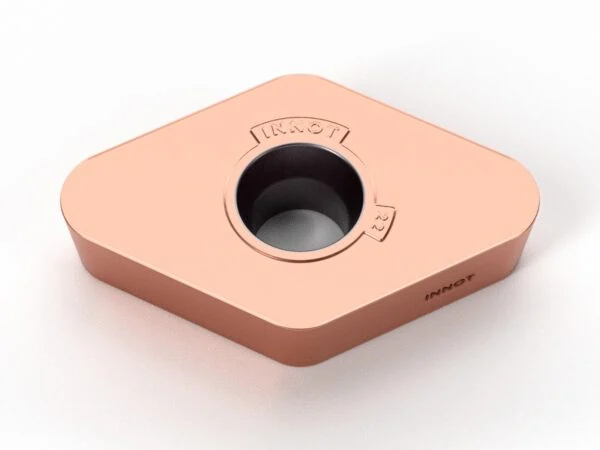
Insert for 90° square shoulder milling: APMT-HM in coated carbide, APGT-AK polished for aluminium.
BLMP (high feed)
Double-sided insert for high-feed cutters: from BLMP 04 to 13, up to 2 mm/tooth, for steels, stainless steels, superalloys and hardened steels up to 65 HRC.
SDMT / SDMW
Insert for high-feed cutters: light cuts (up to 2.9 mm) with feeds up to 1.5 mm/tooth.
RPMT-HM / RPMW
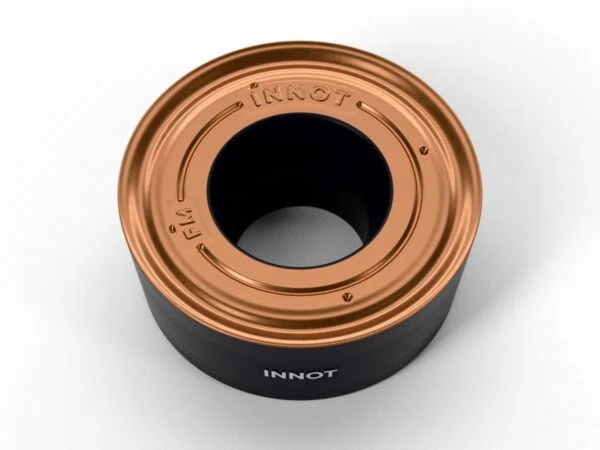
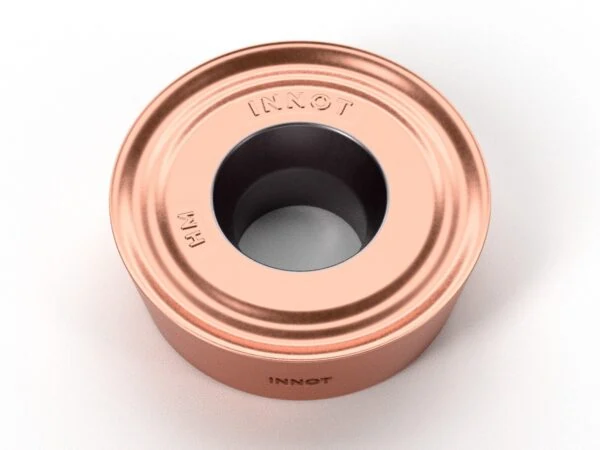
Round insert for copy milling of moulds and 3D surfaces, with 11° clearance angle.
RPKT / RPMT-SM
Round insert for stainless steels, titanium and superalloys: MS/SM chipbreaker and AlCrN PVD grades.
RDMW / RDKW
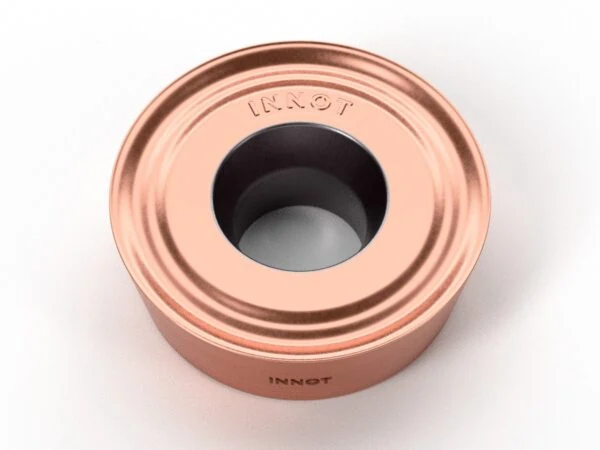
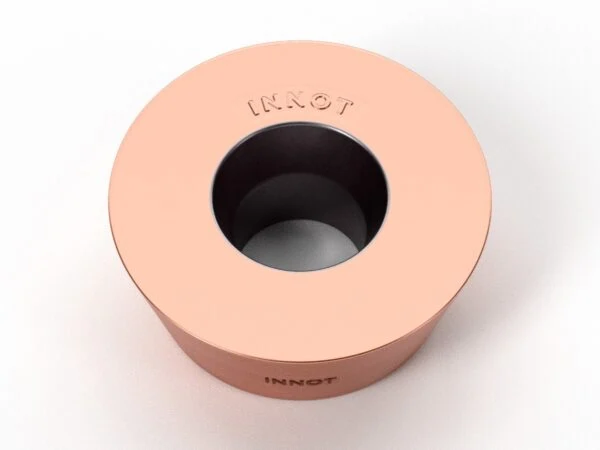
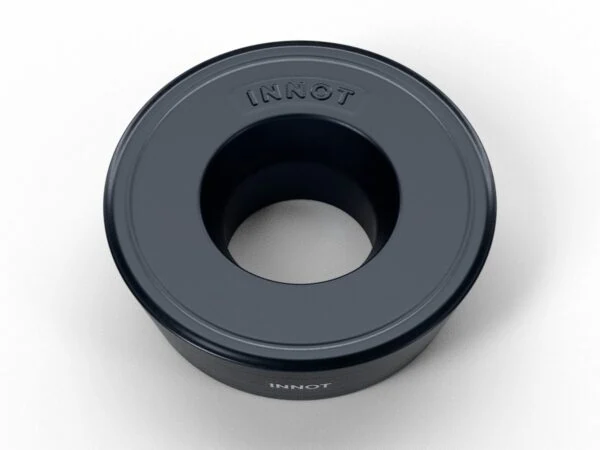
Round insert with 15° clearance for copy milling cutters, from Ø5 to Ø16 mm.
BNM (ball nose)
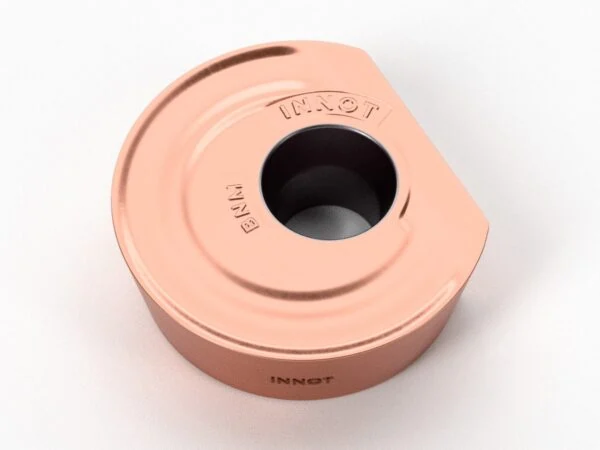
Ball nose insert for copy milling cutters, from Ø12 to Ø32 mm, for finishing moulds and 3D surfaces.
UNM-CE (copy milling)
Insert for large-radius copy milling cutters (RE up to 20 mm), for roughing and semi-finishing of moulds.
RDHX (15° round)
Ground round insert with 15° clearance for copy milling cutters, from Ø5 to Ø12 mm: moulds, 3D surfaces and hardened steels up to 65 HRC.
SPMT / APMT-MM
Inserts for 90° helical (long edge) cutters: deep shoulders and roughing of tall flanks.
Carbide milling inserts for every strategy
INNOT milling inserts cover face milling, 90° shoulder milling, high-feed milling, mould copy milling and helical cutters, in PVD and CVD coated grades for steel, stainless steel, cast iron, aluminium, superalloys and hardened steel.
Which insert for which operation
- Face milling: 45° inserts (SEET, SEMT, SEKR) and double-sided inserts with many edges (ODMT 16, XNMX 14, HNMX 12, SNGX 8) to cut the cost per edge.
- 90° shoulder milling: APMT and APKT, AOKT, the tangential LNHX and the double-sided triangular ZNMU for shoulders, slots and contouring.
- High-feed milling: SDMT and BLMP for roughing moulds and pockets with light depths of cut and very high feeds per tooth.
- Copy milling: round inserts RPMT, RDMW, RCKT, RDHX and BNM ball nose inserts for 3D surfaces.
For every insert you will find the matching indexable cutter in the toolholders and chucks section.
Frequently asked questions
Double-sided or positive inserts?
Double-sided inserts offer more edges and cost less per edge, but need stable and powerful machines. Positive inserts cut more lightly: they are ideal on small machines, less rigid setups and work-hardening materials such as stainless steel and superalloys.
What is the difference between PVD and CVD coatings?
CVD has a thicker layer and resists heat and wear better when milling steel and cast iron. PVD keeps the edge sharper and tougher: it is preferred for stainless steel, superalloys and interrupted cuts.

Categories
- Turning Inserts (121)
- Negative inserts (84)
- CNMG / CNMA - 80° rhombic (16)
- DNMG - 55° rhombic (13)
- SNMG - 90° square (15)
- TNMG - 60° triangular (14)
- VNMG - 35° rhombic (12)
- WNMG - 80° trigon (14)
- Positive inserts (23)
- CCMT - 80° rhombic (4)
- DCMT - 55° rhombic (4)
- SCMT - 90° square (2)
- TCMT - 60° triangular (4)
- VBMT / VCMT - 35° rhombic (7)
- RCMX - Round (2)
- Parting and grooving (7)
- Negative inserts (84)
- Milling Inserts (24)
- Face milling (8)
- 90° square shoulder (5)
- High feed (3)
- Copy milling and profiling (7)
- Helical cutters (1)
- Solid Carbide End Mills (14)
- Drills (9)
- Solid carbide drills (7)
- Indexable drills (2)
- Threading (19)
- Threading inserts (7)
- Taps (12)
- Through hole taps (5)
- Blind hole taps (5)
- Forming taps (1)
- Special and custom threads (2)
- Toolholders and Chucks (15)

Inserts and cutting tools for CNC machine shops. Dedicated grades for every ISO group, from steel to aluminium, from superalloys to hardened steels, with cutting data in every product sheet.
INNOT by Giammarco Turati
Via San Ponso, 57 – 10080 Pertusio (TO)
VAT No. IT13269100015
© 2026 INNOT by Giammarco Turati – VAT No. IT13269100015 – Pertusio (TO), Italy – Privacy Policy – Cookie Policy