Need help? Call us: (+39) 3757861361 or info@innot-it.com
Solid Carbide End Mills
Solid carbide end mills from Ø0.5 to Ø20 mm for steels, stainless steels, cast irons, aluminium, superalloys and hardened steels up to 65 HRC. Flat, torus, ball nose and long-neck mould end mills: choose the geometry or configure your custom end mill.
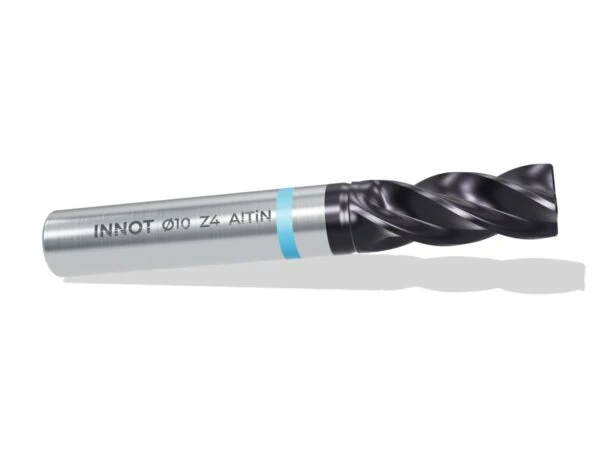
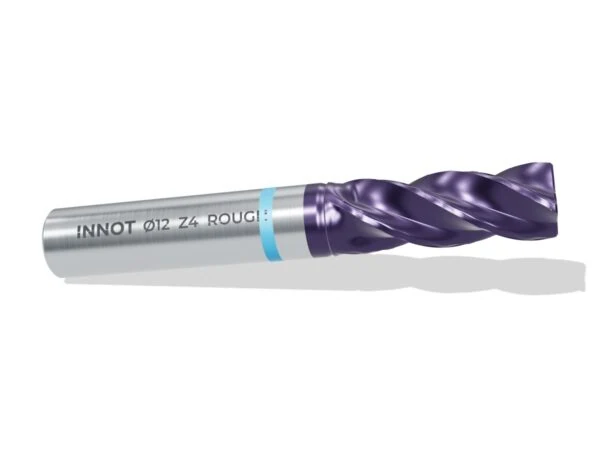
4-flute carbide end mill for steels, alloy steels and cast irons up to 54 HRC, and up to 65 HRC in the hardened-steel version. Available short or long, with or without reduced neck.
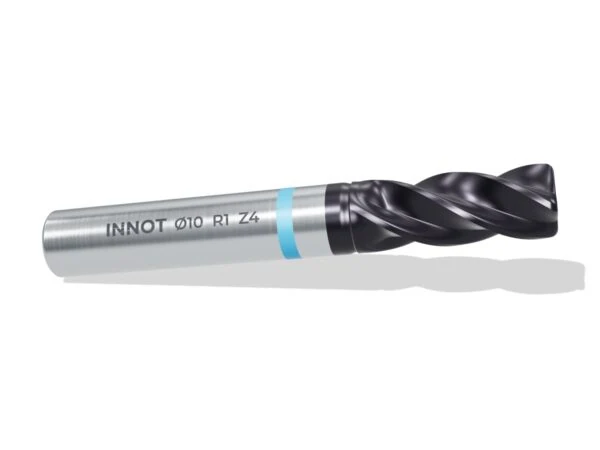
4-flute torus end mill
End mill with a corner radius: the radius protects the cutting edge and leaves a fillet on the part. For moulds, pockets and shoulders with radius.
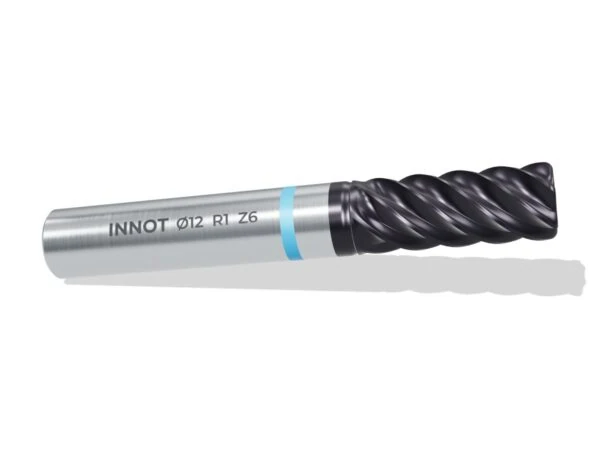
Solid carbide end mill with 6 flutes, square, torus or ball nose, for dynamic roughing and finishing: more flutes engaged for higher feed rates and better surfaces on steels, stainless steels, superalloys and hardened steels.
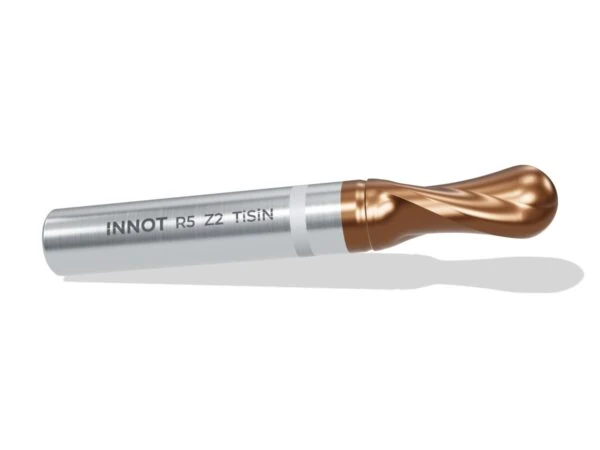
Full-radius end mill (R = D/2) for copy milling and finishing of moulds, free-form surfaces and 3D profiles.
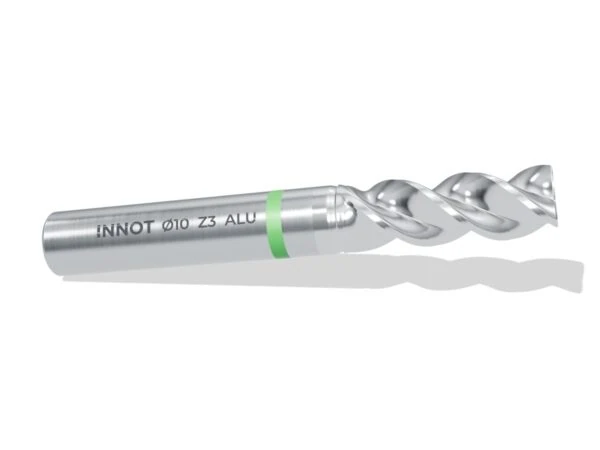
Polished end mill with wide flute for aluminium and light alloys: no built-up edge, excellent chip evacuation and a bright finish.
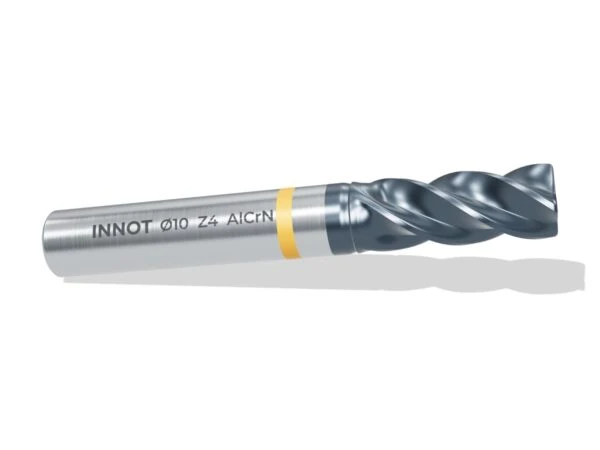
End mill with a highly heat-stable coating for heat-resistant superalloys and stainless steels. Flat or torus.
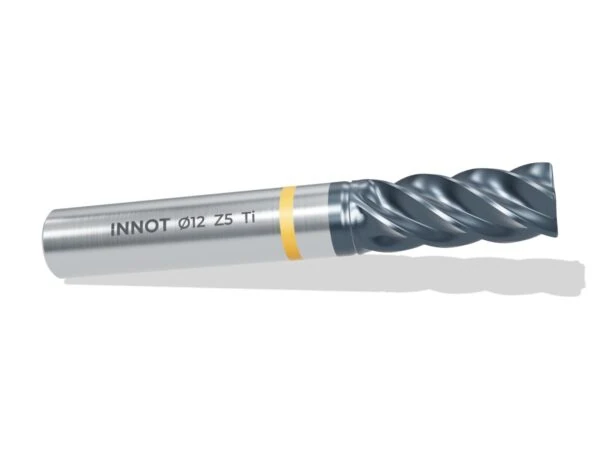
4- or 5-flute end mill with variable pitch for titanium alloys and stainless steels: no vibration and large chip volumes.
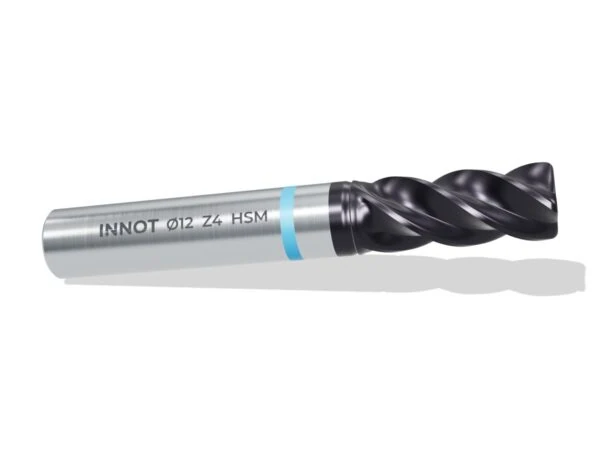
End mill for high-speed machining (HSM) strategies: light cuts and high feeds on steels, alloy steels and cast irons.
Wavy cutting edge that breaks the chip: lower cutting forces and vibration, very high removal rates in roughing.
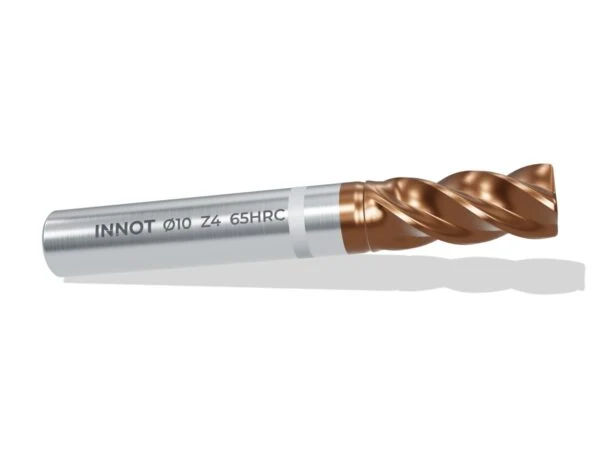
End mill for hardened and mould steels up to 65 HRC: ultra-fine grain carbide, high-silicon coating and reinforced cutting edges. Flat, torus or ball nose.
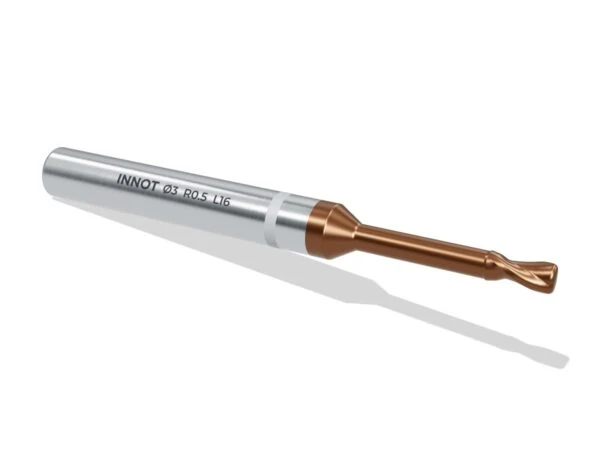
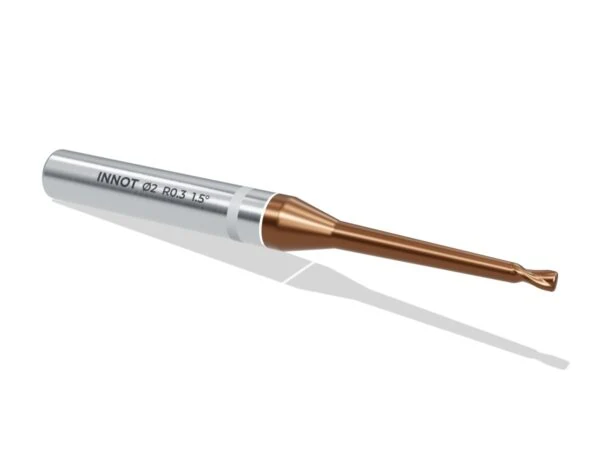
2-flute torus end mill with relieved cylindrical neck for ribs, deep pockets and mould details: it works where the shank cannot reach, up to 65 HRC.
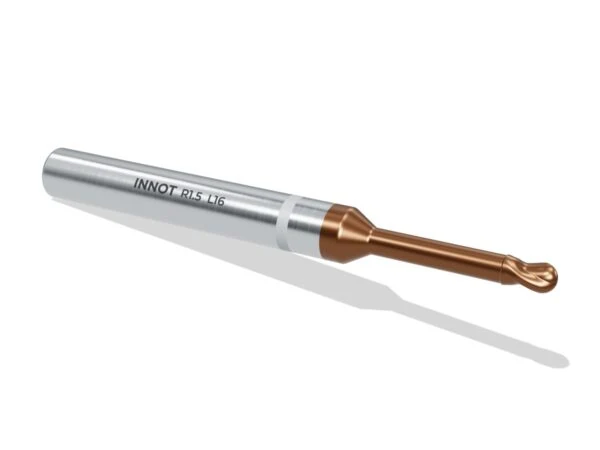
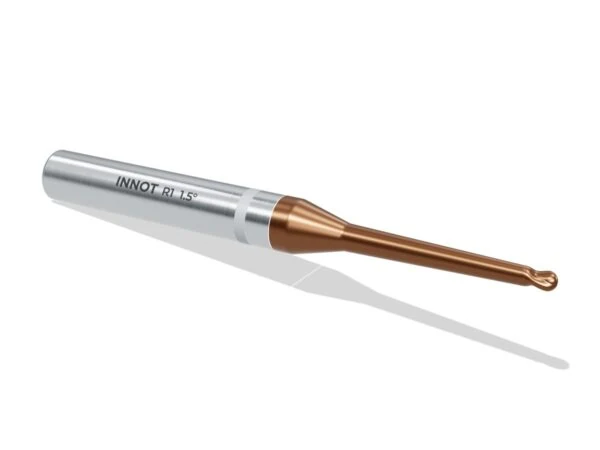
Ball nose end mill with relieved cylindrical neck for 3D finishing of ribs, fillets and deep mould cavities, up to 65 HRC.
Torus end mill with reinforced tapered neck: the neck follows the draft angle of the walls, is more rigid and vibrates less in deep mould machining, up to 65 HRC.
Ball nose end mill with reinforced tapered neck for copy milling and finishing of deep cavities with drafted walls: more rigidity, less vibration, up to 65 HRC.
Solid carbide end mills: square, torus and ball nose
INNOT solid end mills are made of carbide, with 2 to 6 flutes and geometries and coatings dedicated to each material: steel, stainless steel, cast iron, aluminium, titanium, superalloys and hardened steel up to 65 HRC.
How to choose the end mill
- Square end mill: shoulders, slots and contouring with a sharp corner.
- Torus end mill: the corner radius protects the edge and lasts longer in roughing and hard steels.
- Ball nose end mill: copy milling and finishing of moulds and 3D surfaces.
- Number of flutes: 2 or 3 for aluminium and full slots, 4 as the universal choice, 5 and 6 for finishing and dynamic roughing at high feeds.
For moulds there are end mills with a long cylindrical neck or a reinforced tapered neck, to machine deep without vibration. If you need a special size we build it to drawing: use the custom end mill configurator.
Frequently asked questions
Which coating does my end mill need?
AlTiN and TiSiN for steels, hardened steels and dry machining, AlCrN for stainless steel and superalloys, DLC or an uncoated polished end mill for aluminium and non-ferrous materials. The carbide and coatings guide explains the differences.
Do you make custom end mills?
Yes: diameter, lengths, radius, number of flutes, step and coating. Configure the end mill online and get a quote within 30 minutes.
Categories
- Turning Inserts (121)
- Negative inserts (84)
- CNMG / CNMA - 80° rhombic (16)
- DNMG - 55° rhombic (13)
- SNMG - 90° square (15)
- TNMG - 60° triangular (14)
- VNMG - 35° rhombic (12)
- WNMG - 80° trigon (14)
- Positive inserts (23)
- CCMT - 80° rhombic (4)
- DCMT - 55° rhombic (4)
- SCMT - 90° square (2)
- TCMT - 60° triangular (4)
- VBMT / VCMT - 35° rhombic (7)
- RCMX - Round (2)
- Parting and grooving (7)
- Negative inserts (84)
- Milling Inserts (24)
- Face milling (8)
- 90° square shoulder (5)
- High feed (3)
- Copy milling and profiling (7)
- Helical cutters (1)
- Solid Carbide End Mills (14)
- Drills (9)
- Solid carbide drills (7)
- Indexable drills (2)
- Threading (19)
- Threading inserts (7)
- Taps (12)
- Through hole taps (5)
- Blind hole taps (5)
- Forming taps (1)
- Special and custom threads (2)
- Toolholders and Chucks (15)
Recently viewed
Ball nose end mill with reinforced tapered neck for copy milling and finishing of deep cavities with drafted walls: more rigidity, less vibration, up to 65 HRC.
Toolholders for 93° profiling: the narrow tip of 55° and 35° inserts reaches grooves, fillets and undercut profiles.
Full-profile inserts for ISO 60° metric threads: crest and root formed by the insert, finished thread without deburring.
Torus end mill with reinforced tapered neck: the neck follows the draft angle of the walls, is more rigid and vibrates less in deep mould machining, up to 65 HRC.
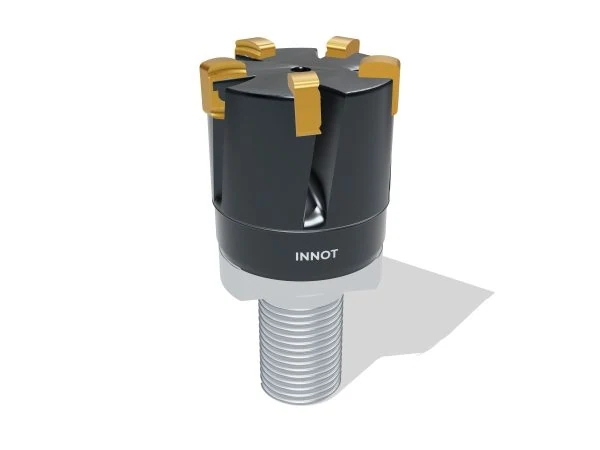
High-feed modular heads from Ø10 to Ø42 mm, 2 to 8 cutting edges, M6–M16 connection, for BLMP inserts.

Inserts and cutting tools for CNC machine shops. Dedicated grades for every ISO group, from steel to aluminium, from superalloys to hardened steels, with cutting data in every product sheet.
INNOT by Giammarco Turati
Via San Ponso, 57 – 10080 Pertusio (TO)
VAT No. IT13269100015
© 2026 INNOT by Giammarco Turati – VAT No. IT13269100015 – Pertusio (TO), Italy – Privacy Policy – Cookie Policy